- LAMMA Show 2026
- Sailun Group
- Maxam Tyre Europe
- Tom Pemberton Farm Life
- Tom Pemberton
- German Agricultural Society
- CASE IH
- New Holland
The Farmer Who Became A Brand: Inside Tom Pemberton’s Partnership With Maxam Tyres
- By Sharad Matade
- August 27, 2026
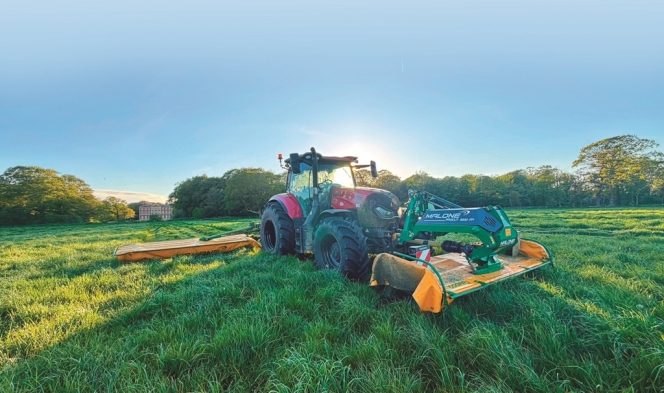
Tom Pemberton never set out to build an audience. He set out to document a Tuesday, filming the quiet, unglamorous reality of running a working farm in Lytham St Annes, Lancashire. Years later, that instinct has turned him into one of the most recognised faces in British agriculture, the man behind Tom Pemberton Farm Life.
At the LAMMA Show 2026, that instinct collided with a very different kind of machine: the global manufacturing engine of Maxam Tyre Europe, a division of the Sailun Group. The result is a new partnership under which Pemberton will fit MAXAM agricultural tyres to his own machinery and share, unfiltered, how they perform. Harry Wang, General Manager of Sailun Group Europe, points to Maxam’s credentials – testing by DLG, the German Agricultural Society, and its role as an original equipment partner to CASE IH and New Holland – as the backdrop to the deal. “Now is the time to further develop the brand and spread the word within the farming community. We feel privileged that Tom has agreed to work with the Maxam brand – and we really like his style and share the same passion for farming,” he says.
FROM A PHONE IN A FIELD TO A FOLLOWING
For farming influencer Tom Pemberton, known for his popular Tom Pemberton Farm Life digital channels, none of it was planned. “I never expected any of this when I first started putting videos online. At the beginning, it was literally just me filming bits of day-to-day farm life and showing the reality of it, the good days, the bad days and everything in between. I think people connected with that because it wasn’t polished or overthought, it was just real,” Pemberton says.
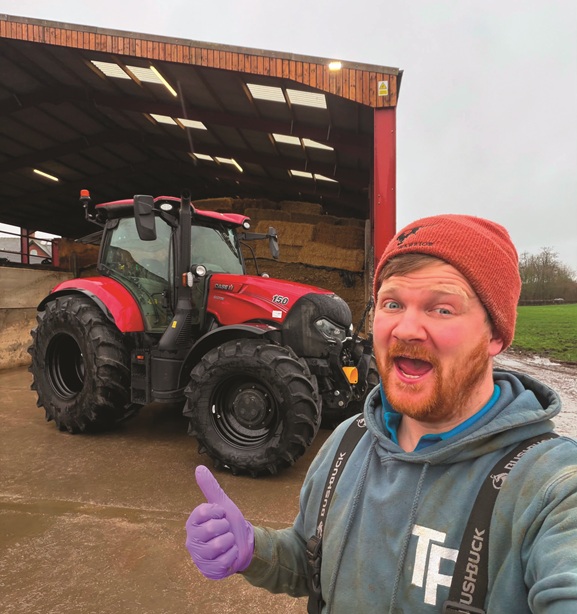 That word, real, threads through almost everything he says about his career. He never sat down with a grand plan for what the channel might become; it began with picking up a phone and filming the day’s work, whatever that happened to be. What changed everything, he believes, was honesty. “I’ve never tried to make farming look perfect because the reality is it isn’t. Some days are brilliant, and some days are stressful, exhausting and frustrating, but that’s real life in agriculture, and people appreciate honesty,” he says.
What has surprised him most is not the loyalty of the farming audience but the appetite from everyone else – a public curiosity about where food comes from that goes far beyond agricultural circles. Social media, he believes, has thrown open the doors of a world that used to keep largely to itself. “Farming used to be quite a closed world in many ways, but now people are sharing ideas, machinery, problems and experiences instantly. It’s opened the industry up massively and given people a real insight into modern farming,” Pemberton says.
That openness has reshaped his own life too. He still describes himself, first and foremost, as a farmer, but one who has found himself combining the daily rhythm of the farm with content and with brand partnerships he says he genuinely believes in. Pemberton adds. “I’m passionate about the industry, and if I can help showcase farming in a positive way whilst having a bit of fun along the way, then that’s a pretty good position to be in.”
WHY TYRES MATTER MORE THAN PEOPLE THINK
It is against that backdrop that tyres, of all things, enter the story. To an outsider, a tyre might seem like the least glamorous component on any piece of farm machinery. Pemberton sees it very differently.
“People sometimes underestimate just how important tyres are on a modern farm. They’re one of those things that can make a massive difference to productivity, efficiency and downtime, especially with the size and weight of modern machinery now,” he says.
Reliability, for him, is measured in hours lost during the exact weeks of the year when there are no hours to spare. “When you’re in the middle of summer harvesting, or trying to beat the weather, the last thing you need is machinery standing still because of tyre issues. Downtime costs money and also adds stress and pressure at the busiest times of the year,” Pemberton says.
Over time, the YouTuber has also come to appreciate the quieter ways tyres shape a farm’s performance and its footprint, from traction and fuel consumption through to the condition of the soil itself. “The right tyre setup can genuinely improve how a machine performs in the field and on the road,” Pemberton says, and it is precisely that intersection of performance and technology that drew him toward Maxam in the first place.
HOW THE MAXAM RELATIONSHIP BEGAN
His account of how the relationship began is notably unsentimental about brand marketing and notably specific about people. What attracted him first, Pemberton says, was attitude rather than advertising – a willingness on Maxam’s part to work directly with farmers and to actually listen to the people using the tyres, day in and day out.
“From the first conversations, it felt like they genuinely cared about performance and real-world applications rather than just selling a product,” Pemberton says. Since then, running the tyres has only reinforced that impression, with build quality, traction and comfort standing out under the kind of workload modern machinery now routinely demands. “Farming conditions are tough, and tyres have to cope with a huge mix of road work, heavy loads and field work, so reliability is a massive thing for me,” he says.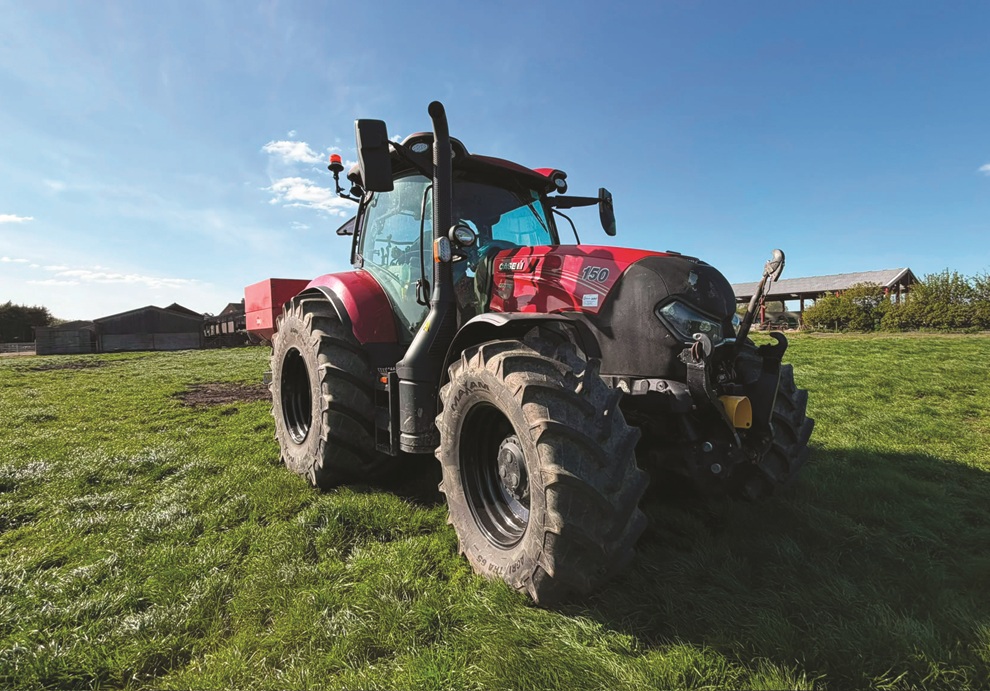 Above all, though, he returns to a single condition for any partnership: authenticity. “For me, it’s important that any partnership feels authentic and that I can honestly talk about the products I’m using on the farm, and that’s something that’s worked really well with Maxam. If I’m going to work with a brand and put my name to something, I want to properly understand the people behind it, the quality of the product and what goes into developing it,” Pemberton says.
He is candid about why that matters so much in farming specifically: farmers are practical people who can spot inauthenticity almost immediately, which means trust has to be earned through real experience rather than through marketing language.
THE FARM VISIT THAT SEALED IT
The turning point came when the Maxam team travelled to his farm in person, a moment Pemberton returns to with evident warmth.
“The real ice breaker for me was when the guys from Maxam came over to the farm to talk things through, see the place and meet me and my family. I genuinely felt like they would have happily gone straight to work on the farm that day. That made a real impression on me and showed they genuinely cared about the partnership,” Pemberton says. Learning more about the manufacturing and testing behind the tyres only deepened that confidence, revealing an engineering effort behind agricultural tyres he suspects most people never stop to consider.
Ask him about the specific technology that has impressed him most, and Pemberton points to a campaign Maxam has been running in UK under the banner ‘More Pull. Less Fuel’, which draws on the brand’s DLG test results. It is a bold promise, he acknowledges, tackling two problems that sit at the top of almost every farmer’s list simultaneously: productivity and fuel costs. “I was curious if they could really make that stretch of increasing productivity and saving fuel at the same time, a pain point for all farmers,” Pemberton says.
FIRST IMPRESSIONS FROM THE FIELD
As for how the tyres are performing on his own machinery, Pemberton is careful not to overstate an early verdict. “To be honest, we have just started, so it’s a bit early to give some in-depth analysis. But my gut feeling from the first weeks out on the fields is very good. No traction issues even in the muddy and ultra-wet areas,” Pemberton says, adding with the kind of dry humour familiar to anyone who follows his channel that the tyres look rather good on his Maxxum too.
SOIL, SUSTAINABILITY AND THE WEIGHT OF MODERN MACHINERY
Beneath the light-hearted asides sits a more serious concern that has come to define much of modern farming: what machinery does to the ground beneath it. Soil compaction and sustainability, Pemberton says, are now unavoidable topics in agriculture, and rightly so.
“The right tyres and pressures can make a huge difference when it comes to reducing compaction, improving flotation and protecting soil structure, especially with modern machinery becoming bigger and heavier every year. Healthy soil is everything in farming and once you damage it, it can take a long time to recover,” Pemberton says. It is a subject he has grown more attentive to over the years, one that now sits alongside traction and durability rather than behind them.
 None of this, in Pemberton’s mind, can be judged from a spec sheet. “You can read specs and brochures all day long, but until a product is out working in proper conditions, carrying weight, travelling on the road and dealing with different weather and soil types, you don’t really know how it’s going to perform,” he says.
Farmers, Pemberton adds, listen to other farmers above almost anyone else, which is exactly why he tries to share honest, unvarnished feedback rather than polished endorsement. For Pemberton personally, the metrics that matter most over time are simple: reliability, durability and consistent performance. “Farming is hard enough without equipment letting you down,” he says.
STAYING TRUSTWORTHY WHILE WORKING WITH BRANDS
It is this instinct for honesty that also explains how Pemberton has managed to work with commercial partners without losing the trust of an audience built on authenticity in the first place. The answer, he suggests, is refreshingly uncomplicated: only work with brands you actually believe in. “My audience would spot straight away if I was promoting something just for the sake of it, and that’s never been what my content is about,” Pemberton says. Whatever machinery or products appear on his channel are there because he is genuinely using them and genuinely curious about how they perform, a distinction that matters enormously to viewers who have followed his farm through years of unscripted reality.
That trust, he says, has been reinforced rather than tested by how closely Maxam and Sailun have worked with him. It began, again, with that farm visit, and it has continued since. “They really listen. Like I said earlier, they came out to the farm, spent time with me and the team here, and didn’t just leave after a quick look around. For me, that says a lot. I already feel like I know the people behind the brand personally rather than it feeling like just another partnership. That’s the true ‘in real life’ view that makes all the difference. You don’t always get that. That’s the sort of thing that builds trust and makes partnerships feel genuine rather than just business,” Pemberton explains.
WHAT SUCCESS LOOKS LIKE FROM HERE
So what does success look like from here, for a partnership that is only just getting started? Pemberton’s answer is less about targets and more about continuity – the relationship staying genuine and mutually beneficial as it grows, with him continuing to show his audience how the tyres perform in real working conditions and giving honest feedback drawn from daily farming life, because that, he believes, is what people relate to most. He also wants to keep expanding the content itself, offering his audience more behind-the-scenes insight into modern farming, machinery and the challenges the industry faces.
From the partnership’s side, he sees success in terms of relationships that deepen over time rather than a single campaign that fades. Farming, he points out, is changing constantly, and social media is only becoming a bigger part of how the industry communicates. There is one particular ambition on his list that captures the curiosity running through the whole partnership: a visit to see Maxam’s factories in person, to understand, as he puts it, how they do their magic.
It is a fitting note to end on. For Pemberton, this was never going to be a partnership built on a logo stitched onto a jacket or a scripted line delivered to camera. It is built on the same principle that built his channel in the first place: show the real thing, and let people decide for themselves. For a company the size of Sailun, betting its Maxam brand’s UK farming credibility on that principle is a considerable act of trust. For Pemberton, it is simply how he has always worked.
Hidden Cost In Tyre Plants: How The Rubber Moves
- By Gaurav Nandi
- October 14, 2026
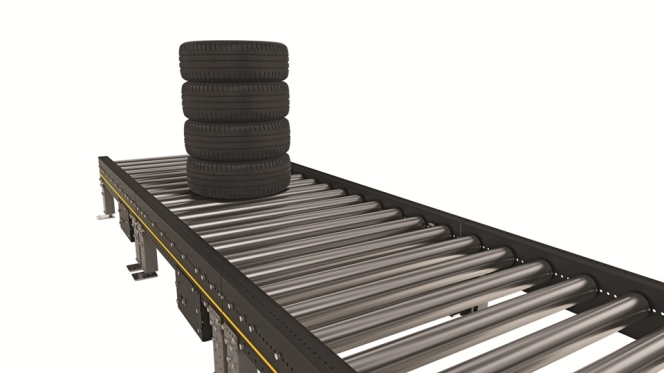
Interroll’s Gianmichele Piciocco argues that some of the largest efficiency gains in tyre manufacturing lie in the interfaces between machines, not only in the machines themselves.
Tyre manufacturers invest heavily in the best building machines and the fastest curing presses. The systems that connect them, however, are often specified late, inherited from earlier projects and seldom revisited, according to Gianmichele Piciocco, Global Strategic Business Development Manager at Interroll.
“Material flow is the backbone of the entire tyre industry,” Piciocco tells Tyre Trends. In his experience, engineers select and position process equipment first, and transport follows. The consequences emerge later, in energy consumption, maintenance stoppages and the cost of expansion. He argues that ‘we have always done it this way’ becomes a design constraint in its own right once technology, product mix, energy costs and safety expectations have changed. The examples that follow point to two closely connected areas: system optimisation during design and expansion, and lifecycle optimisation during operation.
THE LAYOUT TRAP
Piciocco says the pattern is consistent across the tyre manufacturers he advises. “In many cases, the layout initially proposed does not fully match what is ultimately implemented, often to contain the initial investment,” he says. Soon after start-up, plants may find that they need more buffer capacity, or that future expansion was not fully considered. With no floor space left, the remedy for material flow is often inclines, declines and additional levels, which can significantly increase costs.
 The alternative is far cheaper if raised early. “At the design stage, and with possible expansion in mind, it is worth asking whether small changes in machine positioning could support more effective and flexible material flow,” he says.
The issue is especially relevant in India, where sustained market growth does not always mean new greenfield plants. Expansion often happens inside operating sites, where new capacity must coexist with several generations of equipment from multiple vendors. Without a common architectural logic, each extension can add another component family, control standard and maintenance practice, increasing complexity and the potential for integration and compatibility problems.
REOPENING THE BELT QUESTION
Green-tyre transfer illustrates how convention hardens into constraint. Uncured rubber is soft and contamination-sensitive, and belt conveyors have long been the default because a continuous surface supports the tyre and certified belt materials address contamination. Piciocco does not dismiss that logic. He argues it should no longer be treated as absolute.
Left on widely spaced rollers, a green tyre can begin to deform during relatively short stops, and contact with the wrong material can degrade quality after curing. One approach being evaluated by Interroll combines closely spaced rollers, software that keeps them ‘skating’ when the line stops and transfer materials selected to meet contamination requirements. Where a roller solution suits the application, he says, component cost can be materially lower than a belt’s. Because a belt is a continuous element, maintenance work can also take longer and be more complex.
The larger benefit, he argues, is commonality. The same families of rollers, drives and transfer modules can serve both pre-cure and post-cure sections, reducing the spare parts a plant holds and the skills its teams must learn. “Who is interested in saving money in the life cycle of the plant? The user,” he says.
SAVING ENERGY BY DESIGN
Piciocco says moving from conventional 400-volt drive systems to zoned 24/48-volt roller conveyors can reduce energy use, with savings of up to 50 percent in some applications. The low-voltage architecture can also simplify installation and maintenance and reduce exposure to hazardous voltages at machine level, subject to applicable safety standards. The advantage, he stresses, comes chiefly from the on-demand, zoned operating principle, in which only the zones a product needs are active, rather than from voltage alone.
Another example concerns a leading tyre producer that wanted a more compact layout within an existing plant while retaining sufficient buffer capacity and scope for future expansion. The initial conveyor concept required several accumulation loops, curves, inclines and declines, making both engineering and installation relatively complex.
“Working together, we proposed a solution comprising a motorised ascending spiral, an overhead bridge and a gravity spiral for the descent,” Piciocco says. “Each spiral has a footprint of roughly three metres in diameter. At a height of about 7.5 metres, the motorised spiral can provide buffer capacity for approximately 25 to 40 tyres, depending on their dimensions.”
The configuration provided the required buffer in a very compact footprint, with fewer powered components and a cleaner, more modular installation. Its cost was in line with, or slightly above, the conventional solution. Piciocco says the question he put to the customer’s technology director was simple: “Are you thinking about today, or the next 10 years?”
GROWING WITHOUT REBUILDING
A brownfield expansion is not simply a matter of adding more metres of conveyor. New sections must fit existing space, controls and maintenance organisation while the plant keeps running.
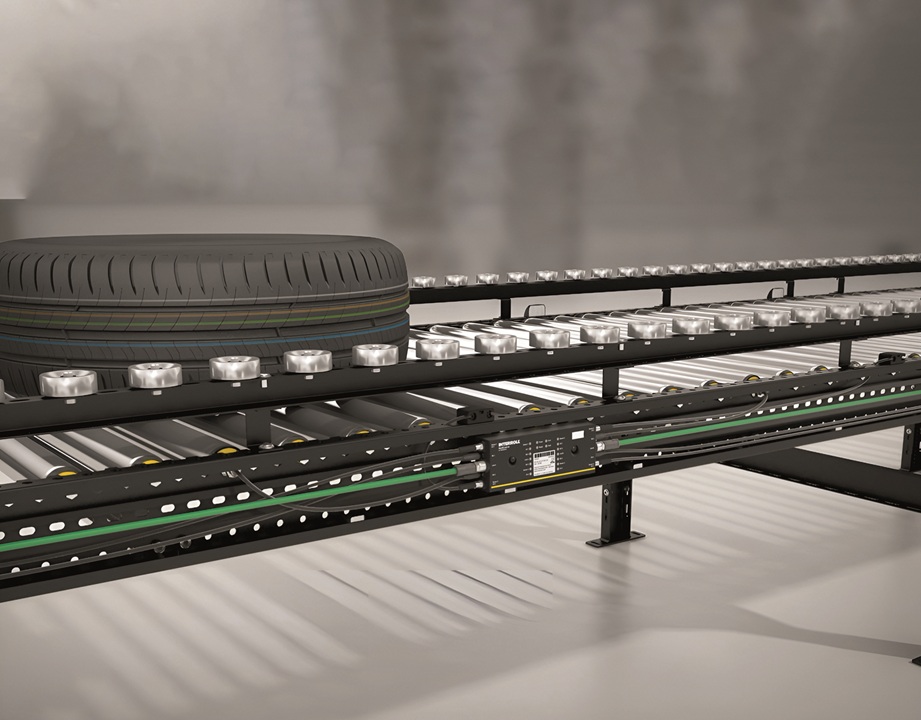
Interroll’s modular platforms, including the MCP range, are built from standard modules. RollerDrive EC5000 units, managed by MultiControl electronics, form a highly scalable and energy-efficient material handling system.
In a conventional centralised architecture, adding zones can require additional I/O, cabling and software changes. In a decentralised system, expansion means adding a module and an Ethernet connection. Independently controlled zones can also absorb small cycle-time differences and micro-stoppages without passing every interruption down the line. Upgrades follow the same logic. The 24-volt EC5000 versions rated at 20 and 35 watts with Analogue Interface (AI) can be used as replacements for the earlier EC310, supporting a more straightforward maintenance approach and the extension of existing installations.
ROUTING WITHOUT OVER-ENGINEERING
Not every route variation calls for a sorter. When tyres must be directed to testing, quality inspection, rework or the next process, Interroll’s position is that a modular conveyor backbone with targeted transfers and diverters often gives a better balance of performance, footprint and cost than a sorter built for distribution logistics. Further downstream, particularly after warehousing, higher volumes and more destinations can justify a dedicated sorter such as the company’s MC-S range.
Piciocco’s warehouse example shows the risk of getting this wrong. A large operator that stacks and stores tyres with considerable automation then needs a separate, costly sorting system to retrieve and route them. In this part of the process, he says, a solution such as Interroll’s MC-S can provide the required throughput with a more efficient layout and a significantly smaller footprint.
CONTINUITY INTO DOWNSTREAM HANDLING
Where load and duty allow, the same architecture can extend past the individual tyre. A 24/48-volt modular pallet conveyor, the MPP platform, can handle a load of up to 500 kilogrammes per metre while retaining decentralised control and zero-pressure accumulation. Rollers of 60 millimetres in diameter allow a closer pitch and more support points, which, after application validation, can reduce vertical undulation when handling tyre stacks.
Piciocco is careful not to make continuity a dogma. Above the platform’s operating envelope, robust 400-volt heavy-duty conveyors remain the correct choice.
FROM REACTION TO PLANNING
Maintenance is where Piciocco sees the most overlooked cost. When total cost of ownership and plant availability are considered, he says, maintenance and stoppage-related costs can account for around 10 to 15 percent of the overall cost associated with material flow in some applications, including labour, spare-parts inventory and lost production during downtime. “Maintenance is often treated as something that simply happens. It should not be. Much of it can be avoided,” he says.
Connected drives, such as the RollerDrive EC5000 BI with MultiControl, make more than 100 parameters available, including operating hours, cycle counts, temperature, system status and error type. If the torque required by a motor rises progressively, the system can flag an abnormal trend before it develops into a stoppage and give the maintenance team a stronger basis for planning an inspection.
Without that information, a failed motor can cause a prolonged stoppage while crews identify the source and check whether the spare part is available. With an early warning, maintenance can schedule the intervention; for an accessible RollerDrive with the spare available, replacement can take less than an hour. Piciocco calls this preventive rather than predictive maintenance. The data does not replace maintenance expertise, but it gives teams a stronger factual basis for decisions, and standard components make diagnostics and training common across the plant.
GLOBAL STANDARDS, LOCAL EXECUTION
A shared catalogue alone does not make a standard, Piciocco says. It also needs consistent selection criteria, spare-parts strategies and support after start-up. Interroll has production, engineering and service capabilities across the world’s main industrial regions, allowing global standards to be supported by local execution. Its life-cycle offering includes structured maintenance programmes, dedicated stock of critical components, periodic audits and staff training, scaled to how critical the application is.
He applies the same logic across markets. Using a smartphone as an analogy, Piciocco says the same platform can be used in a basic configuration or with more advanced functionality, depending on a plant’s needs and technological maturity. A manufacturer can therefore retain common components, diagnostics and training across sites while adapting the level of automation to local conditions.
That flexibility extends to how far automation should go. Speaking for himself, not Interroll, Piciocco says not every producer needs a dark factory. The appropriate level of automation depends on volumes, product mix, process maturity and available skills. “If people do not understand how the technology works, you can have the best technology in the world, but it will not be used properly and may even become a limitation,” he says.
REAL ISSUE
Asked what single mindset shift the industry needs, Piciocco did not hesitate. “Interface,” he says. “The machines are already quite optimised. The problem is how we serve the machine.” As individual machines become increasingly optimised, the interfaces between them play a growing role in improving productivity, simplifying maintenance, reducing energy consumption and enabling future expansion.
“Material flow should not be the last part of the engineering process,” he adds. “If it is considered earlier, we can contribute to a solution that supports optimisation of the entire plant.”
ATIRE Appoints Thierry Miche As Director Of Oem And Product
- By TT News
- October 13, 2026
ATIRE, a leading Sri Lankan Solid tyre maker, has appointed Thierry Miche as director of OEM and product, effective September 2026, bringing more than 25 years of experience in the global tyre and mobility industry to the role.
At ATIRE, Miche will lead the company's OEM and product activities, focusing on portfolio development, OEM relationships and expansion into new technical and commercial markets globally.
Miche joins from Michelin, where he spent 26 years in senior product and operational leadership positions, including roles at Solideal and Camso before their integration into the French group.
His most recent position was product Management Director for Beyond Road, with global strategic and operational responsibility for the product portfolio. He led teams across Belgium, Canada, France and the US, working with research and development, industrialisation, original equipment manufacturer (OEM) and aftermarket sales, and supply chain functions.
Previously, Miche was Product Line Executive Director For material handling, overseeing the global product platform and holding full profit and loss responsibility for three manufacturing sites in Belgium, Germany and the US. He also led global research and development teams in Belgium and Sri Lanka.
His career has spanned product management and engineering, technical support, warranty management, quality assurance and systems. The experience covers the development and delivery of products across engineering, industrialisation, validation, sales and supply chain operations.
The Tyre Giant That Doesn’t Want A Dark Factory
- By Sharad Matade
- October 13, 2026
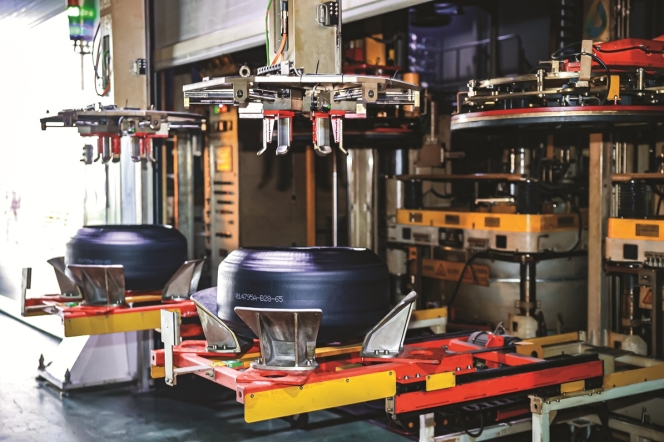
ZC Rubber, China’s largest tyre maker, is running 18 AI agents across its Hangzhou 5G plant. It insists the goal is smarter manufacturing, not emptier factory floors.
Walk into the industrial conversation about automation these days and ‘lights-out’ production tends to come up within minutes: factories with no people, no lighting and machines working in the dark. However, ZC Rubber, the Hangzhou-based group that ranks among the world’s top nine tyre companies, would like to correct that impression before it takes hold.
“We see this as a 5G Smart Factory, or Future Factory V2.0, rather than a ‘dark factory’. The goal is intelligent manufacturing, not simply removing people from the production process,” the company said in an interview.
That is a notable position from a company that has just put 18 AI agents to work across its production chain and reports defect rates well under half those of its earlier operations. It is also a considered one, and the details explain a good deal about how the world’s largest tyre market is approaching the factory of the future.
PEOPLE AT THE EXCEPTIONS
ZC Rubber’s division of labour is simple. Automation, AI and real-time data are steadily taking over what the company calls ‘repetitive and highly standardised operations.’ Its people are being moved towards engineering, process management, quality assurance and the handling of exceptions, meaning the unusual problems that no model has seen before.
“We will continue to increase automation, but fully unmanned production is not the goal,” ZC Rubber said. “It is about combining intelligent systems with human expertise.”
The same logic applies to the future. Asked whether lights-out production is on the roadmap, ZC Rubber was clear. “We do not see fully lights-out production as a goal in itself. Technology will be introduced where it brings clear improvements in quality, efficiency, safety and sustainability,” it said.
EIGHTEEN AGENTS, ONE PRODUCTION CHAIN
The scale of the AI deployment is considerable. Since June 2025, ZC Rubber has introduced 18 AI agents across the full production chain. Their use ranges from AI-assisted formulation and virtual simulation to equipment maintenance, production scheduling and quality control. According to the company, they have helped shorten tyre development cycles by 50 percent and lifted production efficiency by 50 percent.
Where does the value come from? Not from any single stage, the company suggests. “The biggest value comes from using AI to analyse production data, optimise process parameters and support faster decision-making across the manufacturing process,” it said. ZC Rubber does not currently publish a stage-by-stage breakdown of the gains.
INSPECTION AND THE DEFECT RATE
Quality control is where the company’s numbers are most striking. Its latest AI-based visual inspection systems, it says, can achieve a defect detection rate of close to 100 percent, improving both the speed and the consistency of inspection. That matters most in high-volume passenger car radial (PCR) output, where human inspectors face the twin problems of fatigue and sheer throughput.
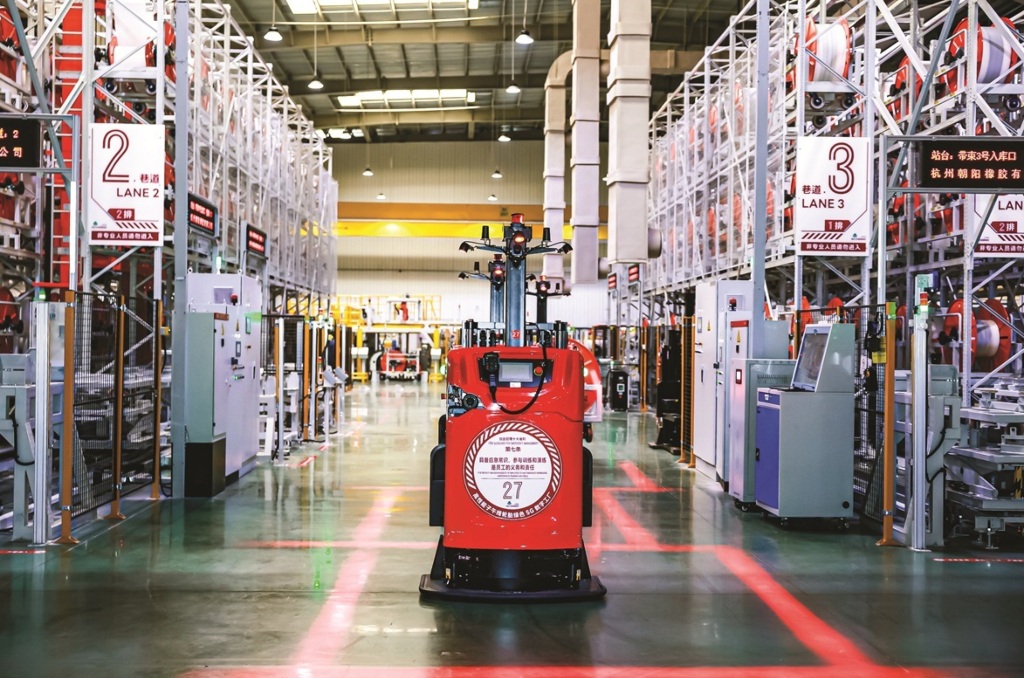 Zooming out, the company says AI and digital quality control across its smart manufacturing system have cut its product defect rate from 1.2 percent to 0.5 percent.
HOW THE SYSTEMS TALK TO EACH OTHER
“Thousands of sensors collect production data in real time, while 5G connects equipment, quality inspection and logistics systems,” the company said. The APS+MES system pulls production, quality and logistics information into one place ‘so operations can be monitored and adjusted quickly’. AI and big data analytics then help staff spot problems and make faster production decisions.
AN EARLIER SET OF NUMBERS, UPDATED
ZC Rubber’s earlier claims of a 15 percent efficiency gain, up to 40 percent lower defect rates and a 5 percent cut in energy use make one notice that the latest figures are considerably better. The company is candid about why. “Those figures reflect an earlier stage of our smart factory development,” it said.
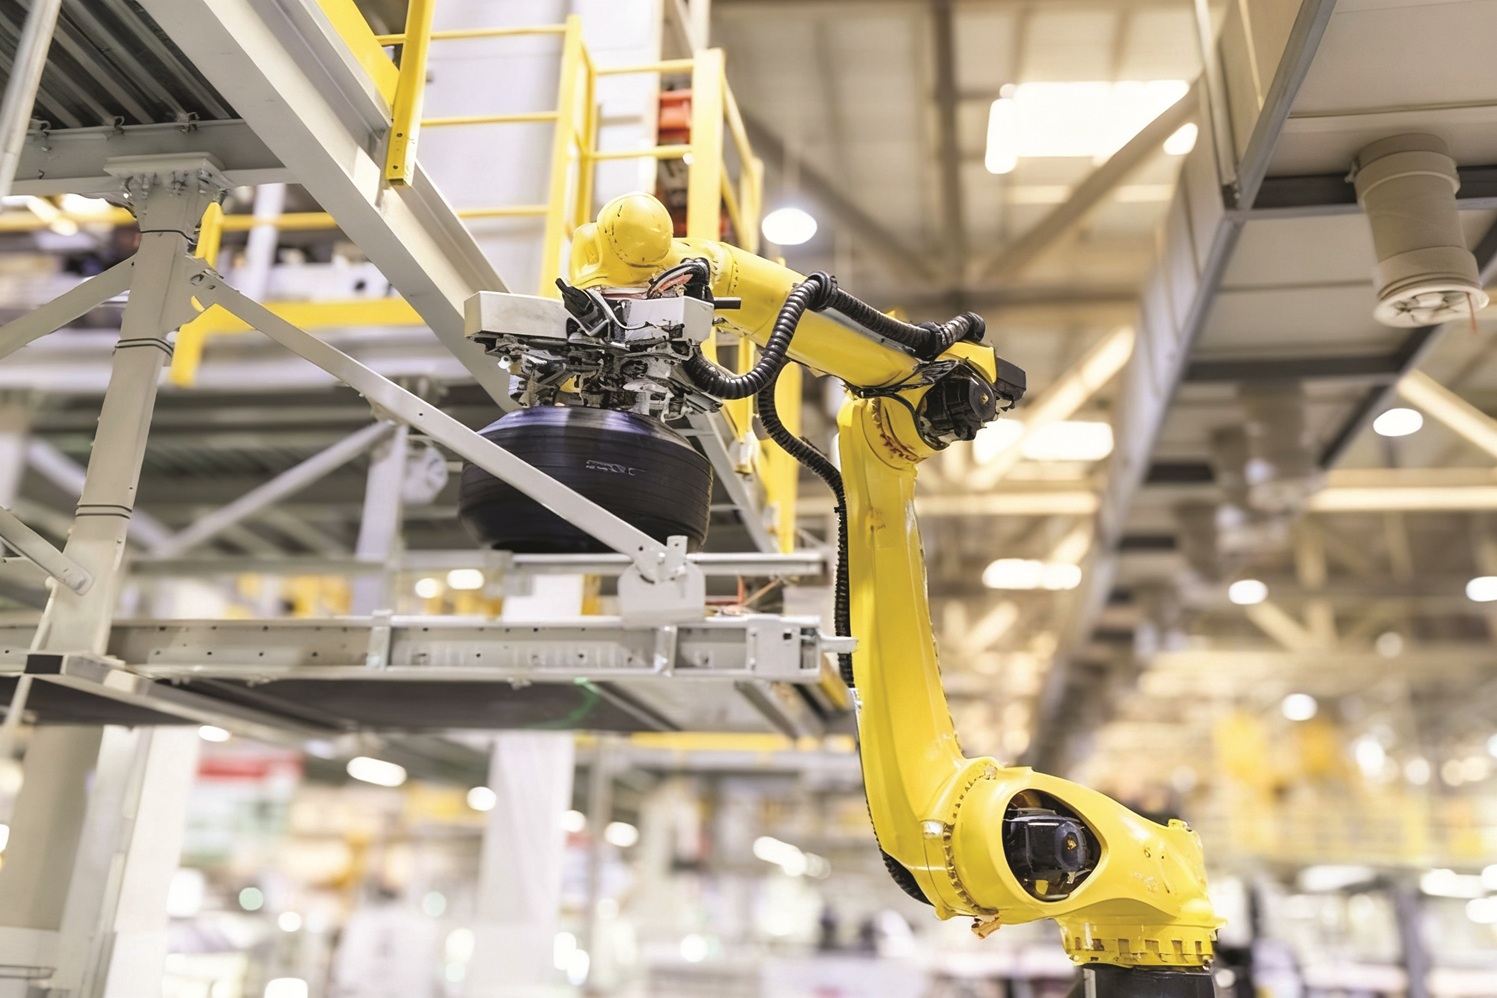
The current numbers, for the 5G Smart Factory, are a 50 percent improvement in production efficiency, defect rates down from 1.2 percent to 0.5 percent and a 10 percent reduction in overall energy consumption.
As for which technology deserves the credit, ZC Rubber declines to rank them. “We do not break down the improvement by individual technology,” it said, naming instead the key components: AI-based process control, automated inspection, intelligent logistics, APS+MES production management and data-driven quality control.
ENERGY, MEASURED VALVE BY VALVE
The energy figure is worth a closer look, because it comes from a fairly granular system. ZC Rubber’s energy management combines 5G, IoT, big data, AI and digital-twin technologies. Smart sensors, smart meters and smart valves feed real-time data into a central energy platform, while AI supports analysis and operational optimisation.
The division of labour among the technologies is neat. “5G provides the connectivity, while AI, big data and digital twins help turn the data into better energy-management decisions,” the company said.
TWO PLATFORMS AND A DIFFERENT STARTING POINT
The manufacturing story is inseparable from the development story. ZC Rubber runs two proprietary technology platforms: the X-Tech System, primarily for truck and bus radial (TBR) tyres, and the Phecda Tech System, primarily for PCR tyres. Each integrates compound formulation, tyre structure, process engineering, simulation, testing and intelligent manufacturing within a single development framework.
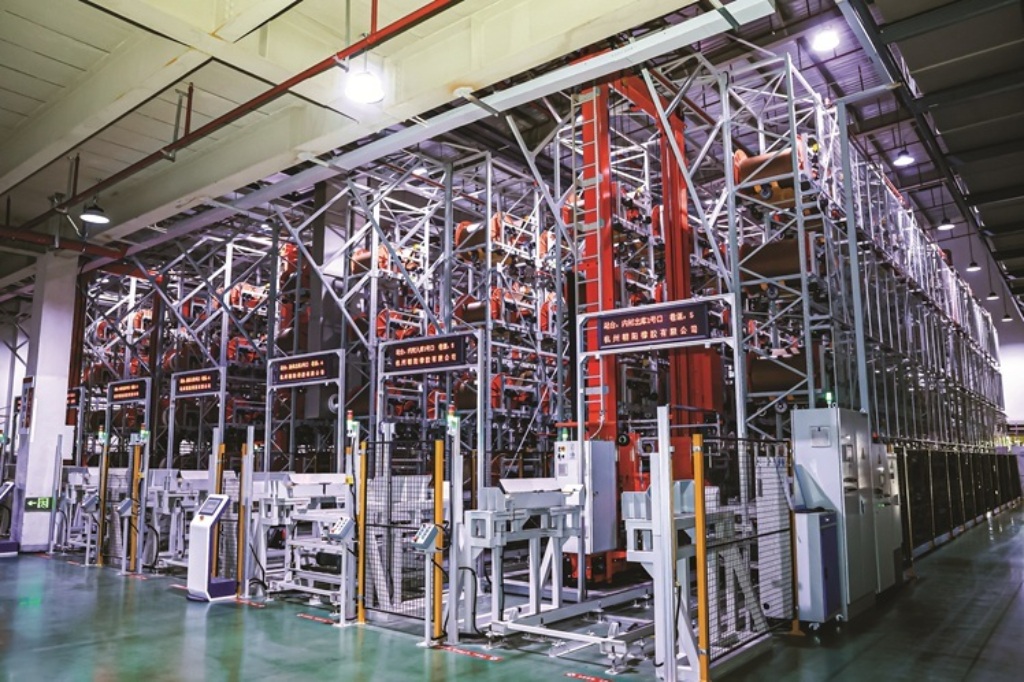
Their defining feature is what the company calls the Forward-development Approach. Traditional development, it explains, “often starts from an existing product and improves it through repeated design and testing cycles”. ZC Rubber starts elsewhere: with the target performance, whether that is vehicle characteristics, duty cycle, climate, road conditions or customer requirements. The compound, tyre structure and manufacturing process are then built around those targets. “This shifts the workflow from repeated iteration to a more integrated, target-driven development process,” the company said.
That, it argues, is where the halving of development time comes from. The 50 percent reduction reflects ‘a more integrated digital development process’, combining engineering expertise with simulation, AI-assisted tools and closer links between R&D, testing and manufacturing. AI lets engineers evaluate more design options against defined performance targets, and virtual simulation cuts out unnecessary physical iterations.
How tightly these platforms are wired into live production data has not been shared publicly. X-Tech and Phecda, the company said, connect R&D, manufacturing and validation within an integrated development process, but the detailed real-time data architecture behind them ‘is not something we currently disclose publicly’.
Henry Shen, ZC Rubber’s Senior Vice President, has made the wider point in the context of the group’s recent State recognition. “Our objective is not simply to develop an individual material, tread pattern or manufacturing process,” he said. “X-Tech and Phecda are complete development systems that connect user requirements with simulation, materials, tyre engineering, manufacturing and validation.”
THE STATE PRIZE
That recognition is significant. ZC Rubber, together with Harbin Institute of Technology, has been awarded the Second Prize of China’s State Science and Technology Progress Award for a project titled ‘Key Technologies and Green Intelligent Manufacturing of High-Performance Tires’. It is one of the country’s highest state-level honours for scientific and technological innovation, and ZC Rubber says it is the only Chinese tyre manufacturer in the past decade to win it at the Second Prize level or above.
The company backs the claim with spending. In 2025, it invested around RMB 1.54 billion (approximately USD 226 million in R&D, equal to 3.43 percent of annual revenue, according to its annual report. The award, it says, recognises technologies that have ‘progressed beyond laboratory research into industrial application’.
GLOBAL FOOTPRINT
ZC Rubber has built a truly global footprint, combining a strong manufacturing base in China with an expanding network of operations across Europe, the Americas, Southeast Asia and beyond. In China, the company operates through multiple sites, including its headquartered in Hangzhou and facilities in Tianjin, Chaoyang, Jiande, Qingquan, Yonggu, Anji and Jintan, supported by dedicated units for recycling technology and automotive aftermarket services in Hangzhou.
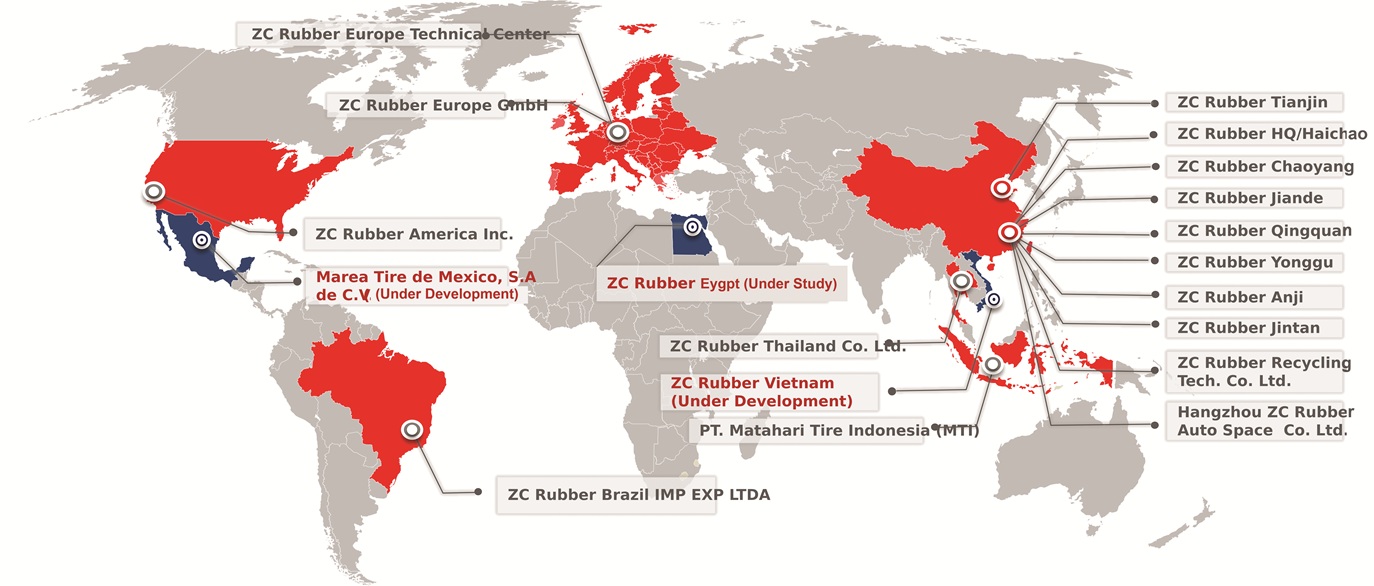
Beyond China, ZC Rubber has established a European presence through ZC Rubber Europe GmbH and its Europe Technical Center, alongside ZC Rubber America Inc. in the United States, ZC Rubber Brazil IMP EXP LTDA in South America and ZC Rubber Thailand Co. Ltd. and PT. Matahari Tire Indonesia (MTI) in Southeast Asia.
The company is also preparing for further expansion, with new projects under development in Vietnam and Mexico (Marea Tire de Mexico, S.A. de C.V.) and a feasibility study underway in Egypt. Together, these locations allow ZC Rubber to serve customers closer to their markets, strengthen supply chain resilience and combine local insight with global technical expertise.
CUSTOMISATION WITHOUT THE PENALTY
The forward-development model has a commercial payoff: tyres tailored to where and how they will be used. Asked whether the platforms allow genuine mass customisation, including regional climates and EV-specific requirements, ZC Rubber answered ‘to a significant degree’.
“X-Tech and Phecda allow us to develop tyres around specific climates, road conditions, vehicle applications and performance targets, including EV-specific requirements,” it said. On the factory floor, flexible production lines adjust output as product mix and orders change. The company does not disclose a separate efficiency figure for customised production, though ‘the goal is clear: to increase product flexibility while keeping production efficient’.
The regional examples are concrete. In Asia, X-Tech underpins the X-Elite Truck Tyre Series. In Europe, it is applied to the WESTLAKE Gen II commercial lineup, with a focus on fleet efficiency, performance and regulatory requirements. Phecda sits behind the WESTLAKE ZuperAce Z-007 and GOODRIDE Solmax 1 passenger tyres, and technologies from both platforms have been applied across ARISUN’s full TBR and PCR ranges for the Americas.
“International markets do not have identical requirements,” Shen said. “A tyre developed for European highway fleets, Southeast Asian transport operations or passenger vehicles in the Americas must respond to different vehicles, roads, climates and customer priorities.”
WHAT COMES NEXT
Much of the technology commonly billed as next-generation is already in service at ZC Rubber. Automated logistics, AI-based visual inspection, process optimisation, digital simulation and virtual testing are all in use. Digital twins are applied in areas such as energy management, and a broader digital-twin virtual factory is part of the next-stage plan.
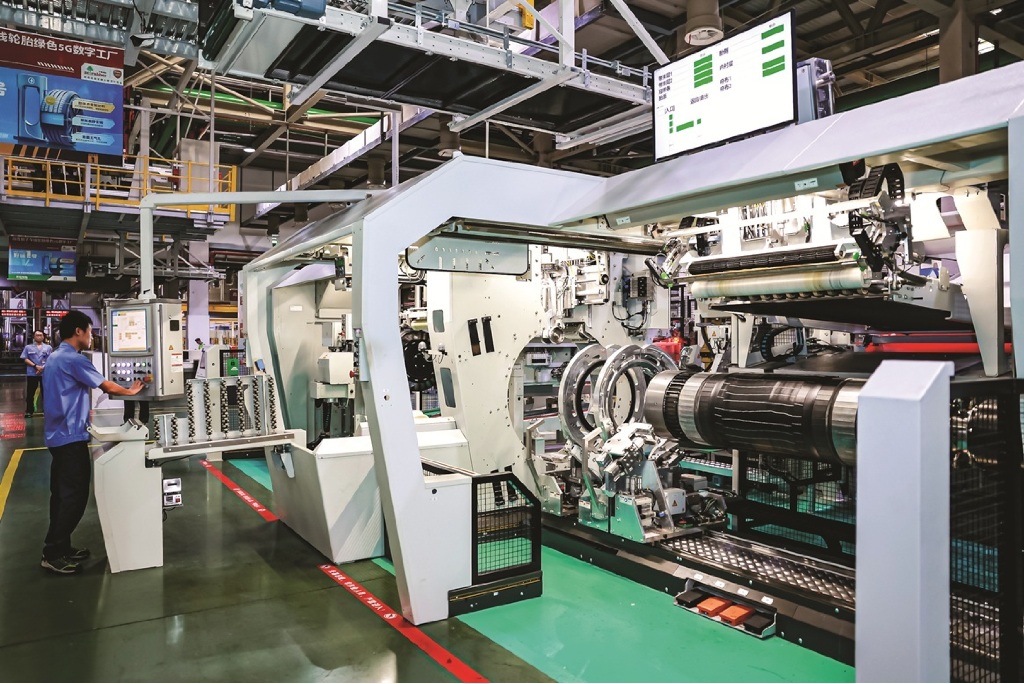 The company frames the coming three years as a period of deepening rather than reinvention: more smart-factory applications, more AI and industry-specific models and close attention to emerging technologies such as humanoid robotics ‘as they mature’.
That phrasing may be the most revealing thing about ZC Rubber’s approach. It is chasing results rather than headlines. As the company itself puts it, the launch of the Hangzhou plant marks ‘a new opportunity and starting point’, and its stated ambition is to become a world-leading tyre company with higher standards. Whether the lights stay on, it seems, is the least of its concerns.
AMETEK Completes USD 5bn Acquisition Of Indicor Instrumentation Businesses
- By TT Bureau
- October 12, 2026
AMETEK recently completed its USD 5- billion all-cash acquisition of a portfolio of instrumentation businesses from Indicor.
The businesses, collectively known as Indicor Instrumentation, make equipment for industrial and scientific applications. Their products serve markets that overlap with AMETEK’s existing operations and generate recurring revenue from consumables, services and aftermarket support.
David A Zapico, AMETEK’s Chairman and Chief Executive, said: “We are excited to complete this highly strategic acquisition and to welcome the Indicor Instrumentation team to AMETEK. With its mission-critical solutions, deep technical expertise, and strong positions in attractive end markets, Indicor Instrumentation is an excellent fit with AMETEK. We also see meaningful opportunities to create value through integration into our proven operating model.”
Indicor Instrumentation is expected to contribute about USD 350 million to AMETEK’s sales in 2026 and to be modestly accretive to adjusted earnings for the year.
The acquired businesses will join AMETEK’s Electronic Instruments Group and Electromechanical Group, according to their products and market focus.
Comments (0)
ADD COMMENT