Reducing Ash Content In rCB
- By Gaurav Nandi
- December 18, 2025
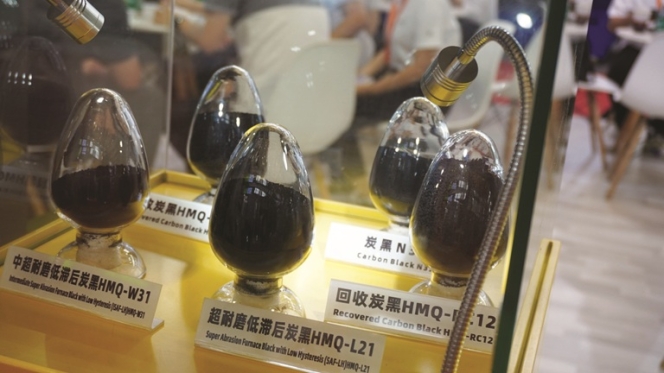
Recovered carbon black is edging closer to mainstream adoption as ASTM International committee D36 on Recovered Carbon Black develops a new ash content standard, D8621. The test promises to slash analysis times from 18 hours to just a few, a change that could reshape productivity and quality control for tyre makers and rCB producers. Yet the push for faster monitoring also exposes a bigger challenge, as standardisation alone will not guarantee industry-wide adoption. With high capital investment, scaling hurdles and safety considerations, the new method sits at the intersection of technical progress, economic pressure and the tyre industry’s sustainability ambitions.
The ASTM International’s recovered carbon black (rCB) D36 committee developed and published a new standard called D8621, which will improve productivity of tyre makers and also enhance production process monitoring abilities.
Speaking exclusively to Tyre Trends, ASTM D36 Chair and Director of rCB at Circtec, Pieter Ter Haar, said, “The D1506 method was developed for regular carbon black, which typically has an ash content of <1 percent. rCB typically has an ash content between 15 and 30 percent.”
The new standard promises to cut testing times from 18 hours to just a few. Commenting on this, he said, “This rCB-specific test method requires less material, and by operating the furnace at a higher temperature, the rate-of-reaction is optimised for rCB, resulting in the significant reduction in time. Since ash content is one of the important product specifications, reducing the time to obtain results is of great help in quality control of the production process of rCB.”
“The main benefit is the significant reduced time required to obtain ash content information of the rCB sample from a tailor-made test method. The future bias and precision study will have to show if the method also has an improved standard deviation,” he added.
CONSENSUS BUILDING
The method’s creation reflects the convergence of some of the industry’s biggest players. “This standard was created by the globally leading rCB, carbon black and tyre manufacturers who come together in the committee. We will actively try to promote the use of this method going forward both for producers and users,” said Ter Haar.
He argued that the proposed standard could reshape the economics of rCB production, particularly in terms of reducing waste or lowering costs as more process control will typically result in less waste and a quicker ability to adjust feedstock ratio’s when changes need to be made.
“This new method will also help tyre manufacturers analyse rCB faster and this will, however, not likely play a role in competitiveness compared to virgin carbon black,” he stated.
According to Ter Haar, the temperature of the muffle furnace has increased from 550 degrees Celsius to 700 degrees Celsius, which is an important consideration for the manufacturer using this method when it comes to safe execution of this method. Besides, he wasn’t aware of any other potential risks or limitations that need to be considered.
Alluding to how critical is standardisation in gaining wider adoption of rCB within tyre production supply chains from Circtec’s perspective, Ter Haar explained, “Standardisation will not be the silver bullet for better understanding of rCB or overcoming the initial adoption phase of rCB in rubber compounds. However, when it comes to consistent supply of rCB, relevant rCB-specific specifications are crucial.”
SUSTAINABILITY PUSH
ASTM Standard D8621 fits neatly into the tyre industry’s strategic pivot towards greener materials. According to Ter Haar, the new standard is part of the wider industry development of the rCB producers and adaptation to the needs and requirements of the tyre industry for adoption of new raw materials for the construction of tyres.
He pointed to high levels of capital deployment, the emergence of reputable producers across global regions and platforms like ASTM as proof that rCB is on track to become a cornerstone of tyre sustainability.
“There are very few sustainable raw material options available for the tyre industry that seem to be developing into mature industries,” the spokesperson noted, stressing that rCB is now positioned as a key strategic material for fulfilling long-term sustainability and circularity objectives.
Circtec itself is pushing hard to lead the charge. Later this year, the company will open its third European factory in the Netherlands. The facility, built to a scale comparable with regular carbon black plants, is expected to convert around six percent of all waste tyres in Europe into sustainable products once it reaches full capacity.
“We will continue to focus on the global expansion of Circtec and the development of the sector when it comes to regulatory compliance, technical knowledge and producing high-quality rCB at large industrial scale,” he said.
INDUSTRY RECEPTION
The new standard has already won the backing of the tyre industry. “The tyre industry was an active participant in the development and approval process of this new standard,” Ter Haar emphasised.
The benefit is straightforward, which is more precise quality control. “Any time one of the raw material suppliers can improve their quality control, this is welcomed. The main objective of any new standard is that the test method is technically relevant and improves the ability to test rCB’s characteristics that actually correlate to in-rubber performance,” he explained.
For producers, the efficiency gains are significant. At Circtec’s Netherlands plant, for instance, output is expected to reach 10 tonnes of rCB per hour. At these production rates, quick quality control test methods are crucial.
While faster process monitoring will primarily benefit producers with scaled up production capacity, Ter Haar noted that the standard is not necessarily designed to spark innovation in rCB applications beyond tyres such as plastics or coatings.
Crucially, adopting the new standard won’t require expensive technical upgrades. “The benefit of this method and aim during the development is that for most producers or end-users, there would not be a need for any new investments in equipment. This method is based on the use of an affordable ashing muffle furnace with the ability to heat to 700 degrees Celsius,” he said.
ADOPTION DYNAMICS
ASTM standards remain voluntary, but Ter Haar expects uptake to be swift given the operational advantages. “This new standard is a tool to improve the speed of quality control. It is up to the individual parties to adopt this or any other ASTM method. Due to the clear advantages of this method, I would expect both producers and users to welcome using this test method moving forward,” Ter Haar said.
The development also represents a milestone in a broader strategic roadmap. The ASTM committee D36 on Recovered Carbon Black, formed eight years ago, initially issued guidance on which carbon black test methods could or should not be used.
“At the moment, most of the key product performance characteristics of rCB can be determined,” he observed, suggesting that D8621 could be a stepping stone towards a broader suite of rCB-specific standards on par with virgin carbon black testing.
As rCB moves into the mainstream, the combination of industrial-scale production, regulatory support and technical validation is setting the stage for what could become one of the tyre industry’s most significant sustainability transformations in decades.
Kumho Petrochemical Group Shifts Focus To R&D and Speciality Materials
- By TT News
- September 25, 2026
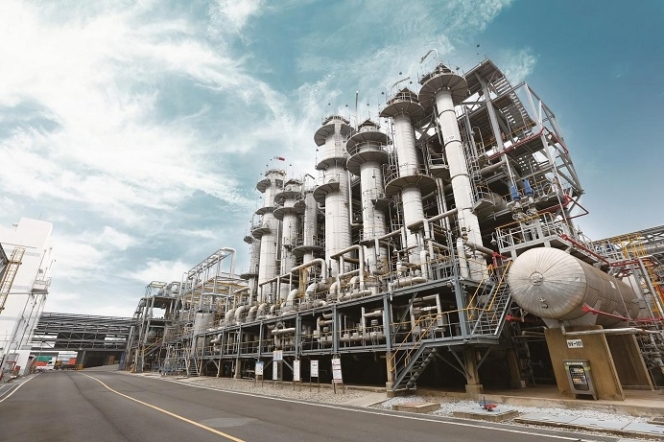
Kumho Petrochemical Group is steering its business towards research-driven, higher-value outputs as oversupply and soft demand continue to weigh on the worldwide petrochemical sector. The Seoul-based group outlined plans to boost spending on speciality chemicals, sustainable materials and novel production methods, a push intended to lift profits while building a foundation for future expansion.
Underlying the move is a deliberate evolution in the group's identity, from a bulk materials vendor to a provider of technology-backed solutions that address shifting customer requirements and stricter environmental rules. A central element of that effort involves widening the speciality lineup, exemplified by added capacity for solution styrene butadiene rubber, a synthetic rubber that enhances durability, rolling resistance and tread wear in high-performance electric vehicle tyres.
Environmental initiatives form another pillar. Facilities built by the company can trap approximately 76,000 metric tonnes of carbon dioxide each year, while separately developed technology turns recycled acrylonitrile butadiene styrene sourced from scrapped household appliances into automotive-grade interior components that satisfy performance standards and generate fewer emissions than conventional methods. The group has also joined forces with POSCO Future M and BEI on anode-free lithium-metal battery development.
Parallel technology-focused programmes are underway at affiliated units. Kumho P&B Chemicals is formulating water-based epoxy resins that curb volatile organic compound releases while incorporating more bio-based inputs to reduce carbon intensity. Kumho Mitsui Chemicals is advancing bio-based polyurethane systems and electric vehicle materials, alongside debottlenecking work to add 100,000 tonnes of annual methylene diphenyl diisocyanate capacity. Kumho Polychem, meanwhile, is targeting ethylene propylene diene monomer through low-temperature polymerisation paired with energy-efficiency improvements.
Birla Carbon Announces Asia-Wide Speciality Materials Price Hike Of Up To 15%
- By TT News
- September 22, 2026
Birla Carbon has confirmed a price increase of up to 15 percent for its Speciality Materials products across Asia, scheduled to take effect on 1 October 2026. The company pointed to significant and sustained rises in feedstock costs, driven partly by ongoing geopolitical instability and disruptions in global feedstock markets, as the reason behind the adjustment.
Although Birla Carbon pursued operational efficiencies, supply chain optimisation and disciplined cost management to soften the impact, the scale and persistence of the cost escalation left a price adjustment unavoidable. The company's sales teams will engage customers directly to explain the details and help them navigate the transition.
ACE Laboratories, Abdallah Consulting Launch VericarbSM To Standardise Recovered Carbon Black
- By TT News
- September 20, 2026
ACE Laboratories, an independent ISO/IEC 17025-accredited polymer testing laboratory, has partnered with Abdallah Consulting, LLC, a prominent tyre pyrolysis advisory firm, to introduce VericarbSM. This independent certification programme verifies that materials marketed as recovered carbon black (rCB) meet established criteria for rCB.
Recovered carbon black, derived from end-of-life tyres via pyrolysis, serves as a sustainable substitute for virgin carbon black in rubber and polymer applications. However, the emerging market has lacked the standardisation and independent verification that established supply chains provide. VericarbSM addresses this gap through independent material characterisation and rubber performance data, offering stakeholders a consistent basis for evaluating rCB products.
For producers, certification accelerates market entry and improves buyer approval rates. Consumers gain more capable suppliers and reduced evaluation time, while investors benefit from clearer volume sizing and fewer costly test failures. The programme is jointly administered by both organisations.
Erick Sharp, CEO, ACE Laboratories, said, “The rCB market has enormous potential, but growth has been held back by uncertainty about material quality and consistency. VericarbSM gives producers a way to prove their product and gives buyers the independent data they need to say yes.”
Dave Abdallah, Founder, Abdallah Consulting, said, “One key reason for the delayed growth of recovered carbon black is lack of product performance information in the customer’s language. ASTM standards are critical; in fact, most testing done in the process follows ASTM methods. But customers relate to a product better when its performance is shown in applications relevant to them. VericarbSM solves the language issue by showing verified rCB in terms of rubber performance while simultaneously adding credibility via third-party analysis and reporting.”
Zeon Establishes Kurashiki Subsidiary To Absorb Tohpe's Acrylic Rubber Business
- By TT News
- September 18, 2026
Zeon Corporation established Zeon Chemicals Kurashiki Co., Ltd. on 23 July 2026 to take over the acrylic rubber operations of fellow group firm Tohpe Corporation. The new entity, headquartered in Kurashiki City, Okayama Prefecture, is wholly owned by Zeon with paid-in capital of JPY 10 million and is led by representative Koji Minami.
On 21 August, Tohpe and the new subsidiary signed an absorption-type company split agreement, prompting Zeon to begin the procedures required under the Companies Act. Operations at the new company, focused on manufacturing and selling acrylic rubber and related activities, are scheduled to commence on 30 October 2026.
Acrylic rubber, known for its heat resistance, is used in automotive components including oil seals and hoses. The Zeon Group already maintains four production sites across Japan, United States and Thailand, forming a global supply network for the material.
The restructuring follows Zeon’s 11 May 2026 announcement that it would transfer Tohpe shares to NATOCO Co., Ltd. of Miyoshi City, Aichi Prefecture, as part of Tohpe’s paints business divestiture. Tohpe’s acrylic rubber operations, which complement Zeon’s Elastomers Business, will now be positioned as a key specialty rubber manufacturing site, with closer operational coordination intended to strengthen Group competitiveness and corporate value.
Comments (0)
ADD COMMENT