- Dr Gerard Nijman
- American Chemical Society
- Fernley H. Banbury Award
- Vredestein
- Prof Ingen Housz
- Albert Dijks
- Michelin
- Green Tyre
The Rubber Whisperer
- By Sharad Matade
- April 06, 2026
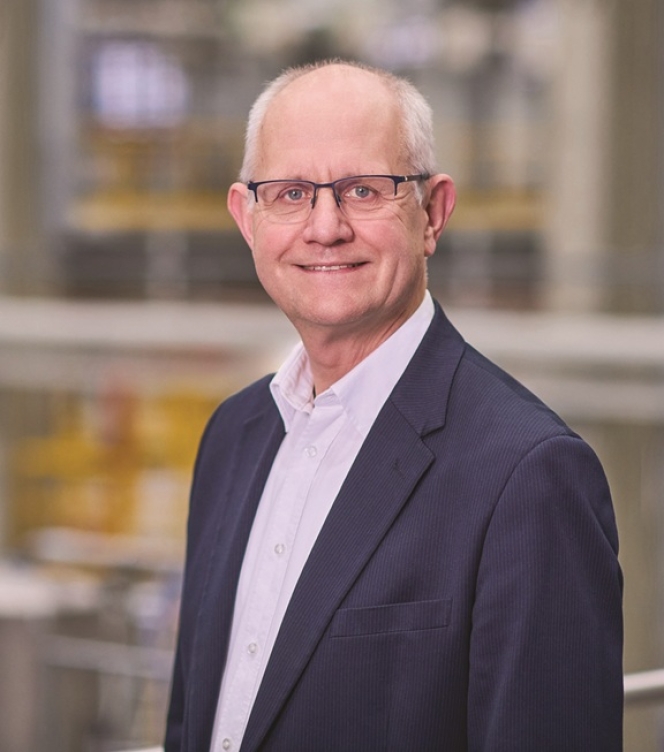
Dr Gerard Nijman
How Dr Gerard Nijman de-mystified the ‘black magic’ of tyre engineering.
In the high-stakes, multi-billion-dollar world of automotive engineering, where the screeching captures the headlines, Dr Gerard Nijman focuses on the quiet, molecular drama happening just inches from the asphalt. To the uninitiated, a tyre is a simple black circle of rubber. To Nijman, it is a visco-elastic masterpiece, a complex soup of polymers, fillers and oils that behaves according to laws of physics that many in the industry once dismissed as ‘black magic’.
Recently, the Rubber Division of the American Chemical Society announced Dr Nijman as the recipient of the Fernley H. Banbury Award. It is one of the highest honours in the field, a recognition of a lifetime spent bridging the gap between the ‘black magic’ of the factory floor and the cold precision of laboratory rheology.
Now, two months after it was announced, I feel proud of being awarded and it is an acknowledgement of my contributions to rubber processing,” Dr Nijman says, reflecting on a career that has spanned nearly four decades. “However, if I consider the enormous lineup of previous winners, I still cannot realise that I am a part of it... I am probably still too humble to really enjoy it.”
THE FRIDAY EVENING CALL THAT CHANGED EVERYTHING
Dr Nijman’s journey into the world of elastomers didn’t begin with a lifelong passion for tyres, but rather with a fortuitous interruption. In 1987, he was deep into a PhD project focusing on molecular orientation in injection-moulded products. His trajectory seemed set for a traditional academic or specialised research path until a Friday evening phone call changed his life.
The caller was the P&O Manager of Vredestein, the Dutch tyre manufacturer. He was looking for a process engineer, specifically someone who understood the complexities of extrusion. For Dr Nijman, it was an opportunity to apply his theoretical knowledge to a massive industrial scale without abandoning his roots.
“For this position, I did not really have to leave my comfort zone, so I decided to join Vredestein on a 50 percent basis while I completed my PhD project,” Dr Nijman recalls. At the time, the industry’s understanding of material flow was rudimentary. The ‘gold standard’ was the Mooney viscosity test – a simple measurement that Nijman knew was insufficient for the high-speed, high-heat world of modern manufacturing.
“I was fascinated by rheology and especially how the material morphology was related to the processing behaviour. At Vredestein, the common understanding of Rheology was ‘Mooney viscosity’, but somehow, I could make them clear that understanding processing means that one must understand the (thermo-)rheological behaviour and morphological characteristics of rubber compound in much more detail,” he says.
 SEEING THROUGH ‘SCIENTIFIC GLASSES’
Dr Nijman attributes much of his success to a trio of mentors who helped him synthesise his disparate skills. His PhD supervisor, Prof Ingen Housz, taught him the fundamental skill of ‘looking at industrial processes through scientific glasses’. It was this ability to analyse a complex, messy industrial problem until the root cause was exposed that set Dr Nijman apart.
At Vredestein, his first boss, Albert Dijks, built his confidence by handing him immense responsibility early on. Meanwhile, Kees Hettema taught him the art of the deal – how to negotiate with customers – and Matthias Sieverding of KraussMaffei Berstorff eventually gave him the reins to lead an entire business unit.
“What I learned from all of them is that, while believing in what you are doing, you should not be afraid of answering difficult questions from your stakeholders,” Dr Nijman notes. This philosophy allowed him to navigate the friction that often exists when a scientist tries to tell a factory veteran that their decades-old ‘gut feeling’ might be wrong.
BREAKING THE SPELL OF ‘BLACK MAGIC’
In the 1980s and 90s, rubber manufacturing was often viewed as more art than science. When a production line ran into trouble, solutions were often found through trial and error. “Suddenly, problems were solved without really knowing why,” Dr Nijman explains. “It was commonly called ‘black magic’.”
Dr Nijman became one of the first engineers to replace that magic with math. He realised that the complex technological hurdles of the industry – irregular shrinkage, surface defects and inconsistent quality – could be solved through a rigorous rheological approach.
His most transformative moment came during the ‘Green Tyre’ revolution of the early 90s. Michelin had just introduced silica-based compounds, which offered lower rolling resistance and better wet grip. While industry giants like Goodyear were still scrambling to adapt, the smaller Vredestein successfully implemented the technology.
The secret weapon was Nijman’s understanding of the microstructure. He recognised that silica compounds were a different beast entirely from the traditional carbon black mixtures. “We looked at the compounds’ processing behaviour by looking to the degree of freedom of the rubber molecules moving around in their microstructure,” he says.
By understanding how silica hindered or helped the ‘relaxation’ of rubber molecules after extrusion, Dr Nijman was able to control ‘extrudate swell’ – the tendency of rubber to expand like a sponge after being squeezed through a die. Without this scientific insight, manufacturers faced uncontrolled shrinkage, leading to tyres that simply didn’t fit the rim.
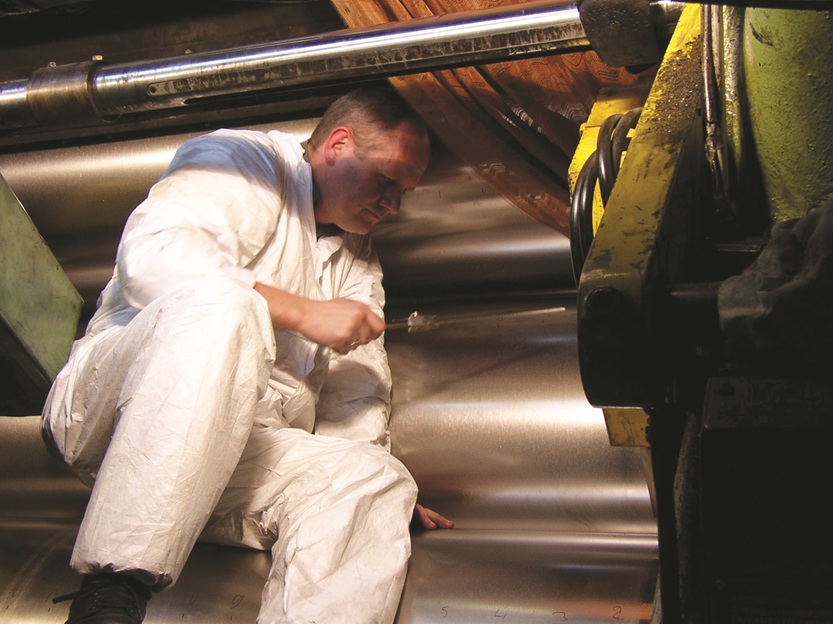 THE PORSCHE 911 CHALLENGE: WHEN THEORY MEETS THE ROAD
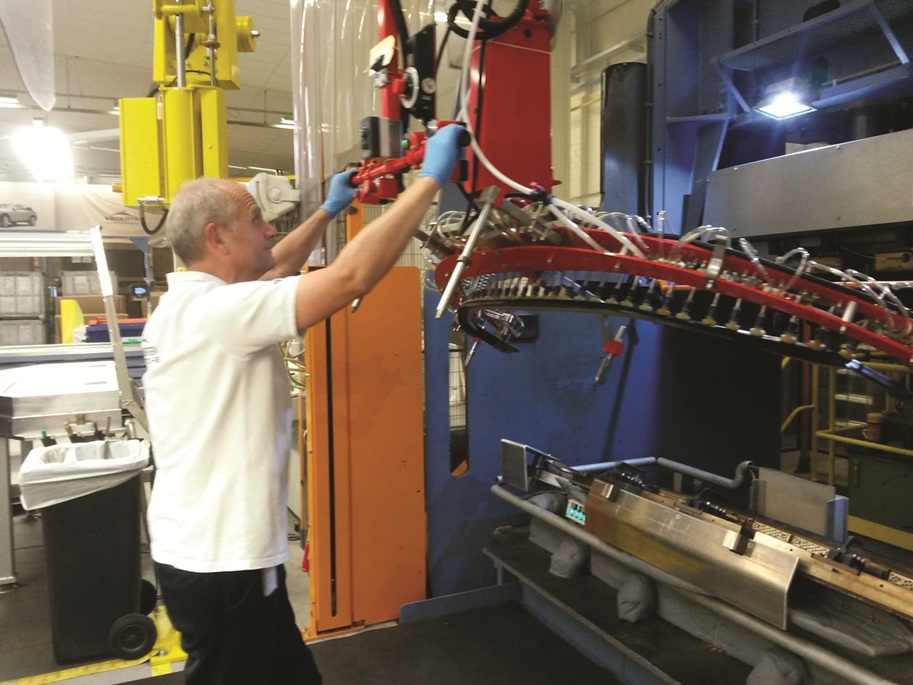
Perhaps the most gruelling test of Dr Nijman’s career wasn’t a tyre at all, but a piece of high-performance aerodynamics: the active front spoiler for the Porsche 911 Turbo. This rubber lip had to deploy at high speeds via air bellows and retract perfectly through its own elasticity once the car slowed down.
The stakes were astronomical. Porsche demanded ‘A1 surface quality’ – meaning the rubber had to be absolutely flawless, with zero visual defects and uncompromised functionality, all while meeting the strict Start of Production (SOP) deadlines of one of the world’s most iconic cars.
“Naming it a challenge was an understatement,” Dr Nijman admits. The project required a total immersion in the material’s behaviour. Dr Nijman describes his method as almost meditative: “I try to be part of the microstructure of the rubber compound on its way from rubber slab to the shape in which it is conveyed. Then I am able to ‘observe’ my surrounding and to ‘see’ what happens with the rubber molecules in their world of fillers, process oils and chemicals.”
THE DIGITAL TRAP: A WARNING TO THE NEXT GENERATION
As Dr Nijman prepares to retire at the end of this year, he looks at the current state of engineering with a mix of admiration and concern. Today’s engineers have access to powerful simulations and AI that Dr Nijman could only dream of in 1987. However, he warns that these tools can be a double-edged sword.
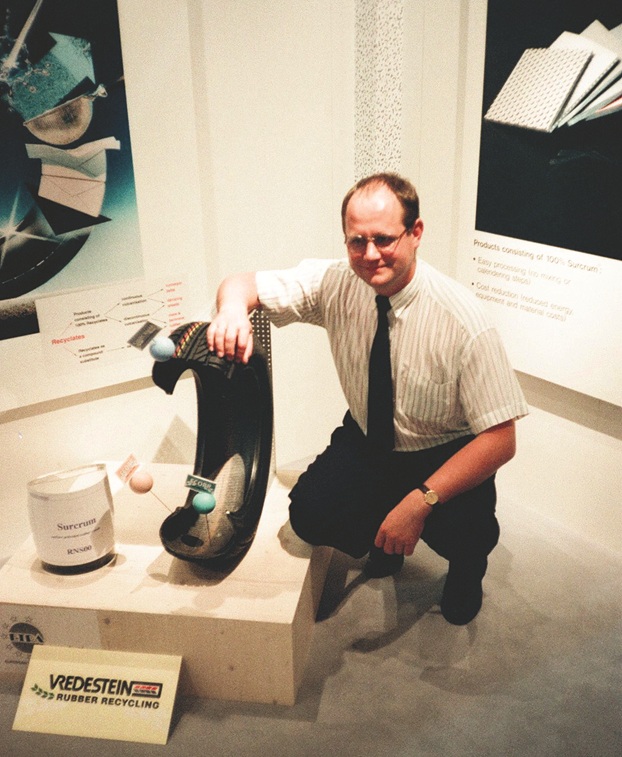 “Engineers tend to believe the results of such simulations are true without critical interpretation,” he says. “In the world of rubber, where chemistry and physics are constantly shifting during the heat of production, a computer model can only go so far. A rubber compound behaves truly visco-elastic. This is not something you can ignore.”
He has observed a shift where younger engineers prefer to solve problems via the Human-Machine Interface (HMI) rather than walking the shop floor. To Dr Nijman, the smell of the rubber and the heat of the extruder are essential data points that a laptop cannot capture. “Both must be done to successfully solve the production problem.”
A SUSTAINABLE FUTURE: THE FINAL FRONTIER
Dr Nijman isn’t using his retirement to slow down; instead, he’s refocusing on the industry’s biggest challenge: sustainability. He believes the next decade of tyre technology won’t just be about grip or speed, but about energy.
“Both tyre manufacturers and extrusion line suppliers should focus more on how to save energy and how to recover heat,” he asserts. He points out a glaring blind spot in current research: while everyone wants ‘sustainable’ compounds, few are looking at reducing the viscosity of the rubber itself – the single biggest factor in how much energy a factory consumes to shape a product.
Reducing scrap and optimising heat recovery, he argues, will require a deeper cooperation between research institutes and manufacturers. “There is still a lot more to be explored scientifically,” he says.
THE LEGACY OF A ‘HUMBLE’ EXPERT
For those entering the field today, Dr Nijman’s advice is simple: love the work, or leave it. But if you stay, never stop asking ‘why’.
“Pursue to deeply understand the problem before you start solving it,” he counsels. “Rubber processing and tyre manufacturing is very exciting... especially if you love being on the shop floor and, at the same time, if you are able to continuously interpret your observations.”
As he prepares to accept the Banbury Award, Dr Nijman remains the same engineer who once spent his Friday nights thinking about molecular orientation. He has spent his career making the complex simple – so simple, in fact, that he measures his success by a unique metric.
“It helped me a lot to realise to explain very complex situations in a way that my mother-in-law would understand,” he says. “That is how I could realise breakthroughs.”
The ‘black magic’ of rubber is gone, replaced by the lifelong work of a man who decided to step out of his comfort zone and look at the world through scientific glasses. Dr Gerard Nijman didn’t just engineer tyres; he engineered a more precise, sustainable and understood future for the entire industry
Azur’s Blueprint For A Circular Tyre Industry
- By Gaurav Nandi
- September 11, 2026

Europe’s tyre industry stands at a crossroads as mounting regulatory pressure, resource constraints and circular economy targets reshape the end-of-life tyre landscape. Despite Germany achieving one of the world’s highest recycling rates, an estimated 100,000 tonnes of used tyres continue to leave the country annually, undermining domestic recovery efforts. In conversation with Tyre Trends, AZuR Network Coordinator Anna-Maria Guth outlines the policy reforms, recycling technologies, retreading opportunities and cross-border collaboration needed to keep valuable raw materials in circulation and build a fully circular European tyre ecosystem.
What gaps in the traditional tyre value chain led to the establishment of the AZuR network?
In Germany, we have a very high recycling rate for end-of-life tyres. However, following a merger of certified tyre disposal companies that collect and sort tyres, it became clear that we needed to bring all stakeholders together to really make progress. The excellent response to the AZuR network shows that this is the right approach.
The European tyre industry is under increasing pressure regarding emissions, waste management and the circular economy. What policy measures are still needed to accelerate the widespread adoption of tyre recycling?
Couple of policy implementations must be achieved in order to reach this goal. The first is a strict ban on the export of ELTs and rigorous enforcement of this regulation. Secondly, clear, predictable and statutory regulations regarding the use of ELT granulate. Lastly, consistent implementation of circular economy strategies.
 What role can recovered carbon black (rCB) play in reducing Europe’s dependence on primary fossil raw materials?
The pyrolysis companies in the AZuR network are making great strides in improving the quality of rCB. We are optimistic that in the foreseeable future, we will be able to produce a grade that allows the material to be incorporated into new tyres in larger quantities. That would be a major breakthrough and would create real added value as it would keep the raw materials within the circular economy.
How does AZuR distinguish between mechanical recycling, devulcanisation and pyrolysis in terms of sustainability and scalability?
Within the network, we adhere to the European waste hierarchy viz-a-viz prevention, reuse, recycle including mechanical and chemical and, finally, thermal recycling.
We are open to all technologies when it comes to processes. However, it is clear that in the interests of the circular economy, we want to minimise thermal recovery. And this also applies to pyrolysis oil provided it is not used for the production of new products but as a secondary fuel.
How close is the tyre industry to establishing tyres made with recycled materials without compromising on performance?
Some manufacturers are already field-testing tyres containing over 70 percent recycled and bio-based raw materials. The industry is very active in this area. However, we would like to see a more nuanced approach to recycled materials and bio-based materials.
Bio-based materials cannot be the solution in the medium term and the EUDR is already restricting the use of bio-based materials in Europe. Our focus must be more on recycled materials and their qualities so that raw materials can be kept in the cycle.
More than 500,000 tonnes of end-of-life tyres are generated in Germany every year. What are currently the biggest bottlenecks in the infrastructure for collection, sorting and processing?
At present, the SME sector in Germany is structured in such a way that all tyres generated can be collected, sorted and processed. Our biggest challenge is that the material is currently being exported rather than ending up with responsible companies in the circular economy. We estimate that around 100,000 tonnes are exported annually without proper regulation.
How will the network influence future EU regulations on the circular economy?
We are delighted to be engaging in growing dialogue with EU bodies, which enables us to raise the profile of the circular economy, which is dominated by small and medium-sized enterprises. Our aim is to set the right course at European level as quickly as possible so that companies can work successfully with the materials and keep as many raw materials as possible in the cycle.
Which groundbreaking technologies or business models are currently attracting the most attention?
There are quite a few, and to name just a few, we have companies in the network working on AI-driven solutions for tyre sorting as well as start-ups producing devulcanised materials for the new tyre industry or AI-assisted machines for the professional regrooving of truck tyres.
How important is cross-border cooperation in establishing a sustainable circular economy for tyres across Europe, rather than in isolated national markets?
AZuR started as a German network, but we can now safely say that we have become a European network. We have partners from Italy, the Netherlands, Austria, Ukraine, Estonia and Poland. All these countries face similar challenges as the relevant legislation is often decided at European level and we can achieve very little at national level. We can only take the big steps together in Europe.
How difficult is it to reconcile economic interests within such a diverse ecosystem?
All AZuR partners are united by a shared vision of 100 percent recycling of end-of-life tyres generated in Europe. We know that this is economically viable. However, we also know that we can only tackle the hurdles that are currently preventing us from reaching our goal by working together.
Our target of 100 percent recycling of end-of-life tyres is very realistic and, in our view, can be achieved in the short term with the right measures.
How do you respond to the market’s ongoing concerns regarding the safety, quality and performance of retreaded tyres?
The retreaders currently operating in Germany are industrial retreaders whose quality standards are in no way inferior to those of new tyre manufacturers. Real-world use shows that there are no quality limitations with retreaded tyres. When retreaded, the casings from premium manufacturers offer a quality comparable to that of the original new tyre.
Incidentally, the safety of the technology is demonstrated by retreaders of aircraft tyres as such tyres are retreaded 12 to 14 times and are highly relevant to safety. And retreading is the ideal solution for recycling as it allows the tyre to be used a second and third time as a tyre.
Why has retreading uptake in the passenger car sector remained relatively limited compared to that in the commercial vehicle sector?
One of the major challenges facing retreading in the passenger car sector is the vast variety of sizes, which makes retreading economically unviable. We are constantly seeking dialogue with vehicle manufacturers on this issue.
Furthermore, passenger car tyres are often in use for longer because they are driven less frequently, meaning fewer casings are available for retreading. However, we believe in passenger car tyre retreading, particularly given the growing share of electric vehicles, and are delighted that a retreader in Germany will be relaunching operations in this segment this year.
How important will AI, predictive analytics and sensor-based tyre management become over the next decade?
Smart tyre management is both an economic factor for haulage companies and an environmental one. We know that how a tyre is used has a significant impact on its service life. And at the top of the waste hierarchy is waste prevention. Here, both the new tyre industry and users are called upon to make optimal use of tyres so that they can remain in service for as long as possible.
What would success look like for AZuR in the next five years?
We would have reason to celebrate if we were to achieve the following key objectives in the coming years. The objectives include 40 percent market share for retreaded lorry tyres in Europe, 10 percent market share for retreaded passenger car tyres in Europe, 100 percent recycling of end-of-life tyres in Europe and clear legal regulations governing the use of recycled ELTs.
Epsilon Carbon Doubles Speciality Carbon Capacity To 600,000 TPA With New Karnataka Plant
- By TT News
- September 10, 2026
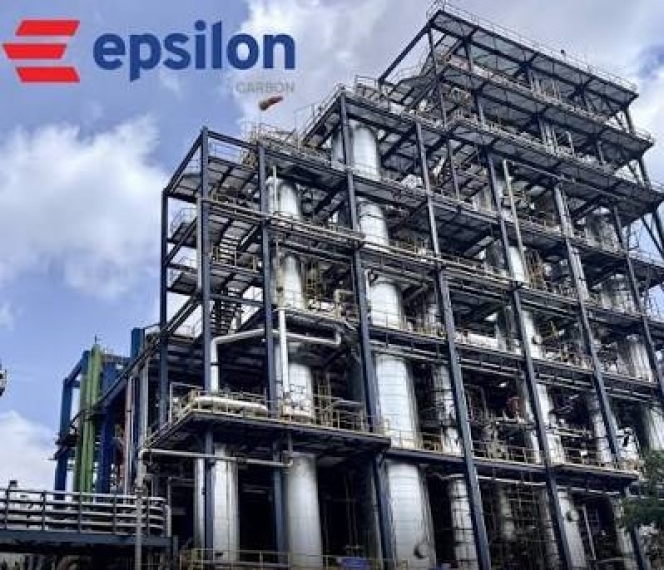
Epsilon Carbon has significantly expanded its manufacturing footprint with the formal activation of a new 300,000-tonne-per-annum speciality carbon plant in Vijayanagar, Karnataka. This latest addition brings the company’s aggregate production capacity in this segment to 600,000 tonnes annually, a development that elevates the firm to a leading position among domestic producers and reinforces India’s broader influence in the international speciality carbon market.
The new installation operates on a fully digitised manufacturing architecture, incorporating real-time process monitoring, automated quality controls and interconnected production systems. Such technological integration is intended to minimise operational variability, maximise throughput and provide overseas buyers with a stable and predictable supply base across multiple product categories.
Output from the Vijayanagar complex will encompass a wide array of coal-tar derivatives, including binder and impregnated pitches, refined naphthalene, anthracene and creosote oils and wash oil. These intermediates find application across a spectrum of heavy and light industries, ranging from primary aluminium and graphite electrode production to tyre compounding, pigment formulation, pharmaceutical synthesis and speciality construction materials.
Looking ahead, the company has outlined a trajectory towards further capacity enhancement, with a proposed integrated facility in Jharsuguda, Odisha, expected to push total speciality carbon output to one million tonnes per annum by the end of the decade. Meanwhile, the Karnataka plant has been configured with closed-loop water management, recycling all treated effluent internally, and derives its entire power requirement from a 17‑megawatt captive unit running on recycled process off-gases. Certifications such as Responsible Care, EcoVadis Silver and SA8000 attest to the company’s adherence to stringent safety, environmental and labour standards.
Gaurav Mathur, Chief Executive Officer, Epsilon Carbon, said, "This expansion reflects India's growing capability to become a global supplier of speciality carbon materials. With 600,000 TPA of Speciality Carbon capacity, we are strengthening supply chain resilience for both domestic industries and international customers, particularly the global aluminium sector. As the world looks to diversify supply chains, Epsilon Carbon is proud to contribute to India's emergence as a reliable, sustainable and globally competitive manufacturing hub."
HS HYOSUNG ADVANCED MATERIALS Showcases Carbon Fibre Innovations At CCE 2026
- By TT News
- September 09, 2026
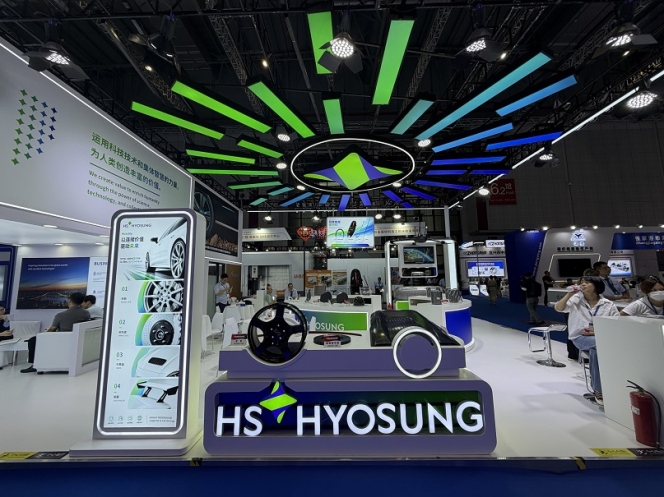
HS HYOSUNG ADVANCED MATERIALS participated in the China Composite Expo 2026 (CCE 2026), held at the National Exhibition and Convention Center in Shanghai from 1 to 3 September. This annual event stands as Asia’s largest specialised exhibition for composite materials, drawing a significant global audience.
The company has been a consistent participant in CCE since 2013, leveraging the expo to progressively reinforce its foothold in the Asian market. At this year’s showcase, the strategic focus was on its portfolio of high-performance carbon fibre products, which are increasingly recognised as essential materials for advanced sectors including energy, mobility and aerospace due to their superior tensile strength and modulus.
Central to the presentation were actual samples of TANSOME, the company’s proprietary carbon fibre brand developed through in-house technologies. The exhibit featured a diverse range of applications, from mobility components like automotive wheels, hoods and brake discs to sporting goods such as hockey sticks and pickleball rackets, as well as high-pressure vessels for hydrogen and oxygen, drones and wire cores.
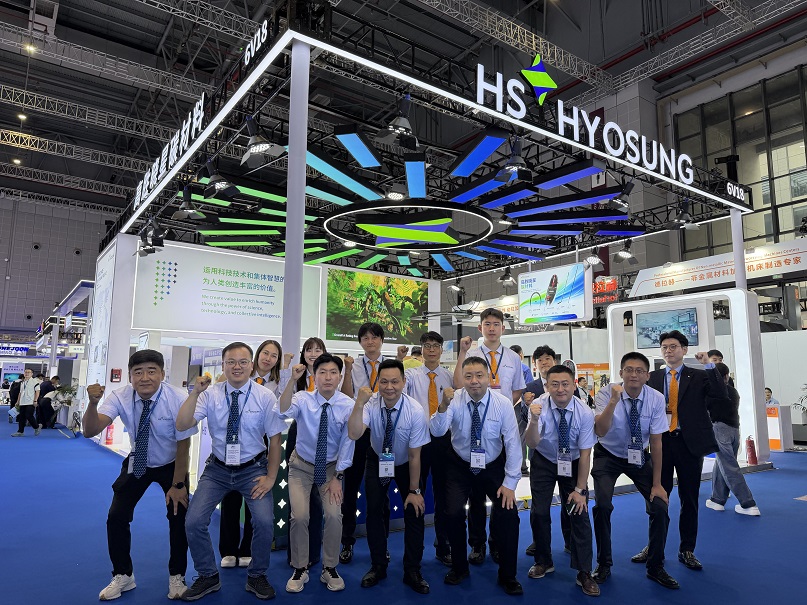
In parallel, HS HYOSUNG ADVANCED MATERIALS emphasised its robust manufacturing capabilities and stable supply chain, supported by production bases in Korea, China and Vietnam. This strategy reinforces its standing as a leading global carbon fibre manufacturer. Notably, the company achieved a milestone in 2011 as the first in Korea to independently develop TANSOME, a material 4 times lighter and 10 times stronger than steel. This was followed by the 2022 launch of H3065, a T-1000-grade fibre with strength exceeding steel by over 14 times, designed for demanding aerospace applications.
Jin Dal Lim, CEO, HS HYOSUNG ADVANCED MATERIALS, said, “This exhibition is an important opportunity to further strengthen strategic partnerships with global customers and demonstrate the outstanding technological capabilities of HS HYOSUNG’s carbon fibre. We will continue to build deeper trust in the global market based on world-class product quality and stable supply capabilities.”
Bekaert Secures Future Of Sardinian Facility Through Nuova Icom Partnership
- By TT News
- September 08, 2026
Bekaert has taken a decisive step towards reshaping its operational footprint in Sardinia by securing a preliminary deal with Nuova Icom, a local engineering entity. The arrangement paves the way for the handover of the Macchiareddu premises and guarantees job continuity for the existing staff stationed there, subject to the final stipulations of the contract.
The decision stems from long-term turbulence in the tyre sector, which has steadily undermined the commercial viability of the plant's primary output. With tyre cord manufacturing struggling to remain profitable amidst evolving industry dynamics, the company concluded that a fundamental operational shift was unavoidable.
This initiative follows an extensive search for sustainable alternatives, emphasising regional employment preservation. Bekaert remains attuned to the social ramifications of the transition and pledges to engage transparently with all affected parties. The prospective ownership change is scheduled for completion by October 2026, pending regulatory clearances and the finalisation of employee consultations.
Comments (0)
ADD COMMENT