Understanding The Customer Psyche, Maintaining personal touch
- By PP Parera
- April 19, 2022

Innovation, similar to communication, which I touched on in the previous issue of Tyre Trends, is a somewhat elusive subject as far as modern organisations are concerned. My intention here is not to delve into the subject’s intricacies but to share my experiences and views with the readers.
I do not know if I am the best person to touch on customer psyche from a marketing perspective. However, on thinking widely and looking at the big picture, I feel I am not very far from the truth that we are all engaged in putting our ideas across and understanding, or very often misunderstanding, relationships and dependencies throughout our lives, be it in family or social and business circles. In other words, we are marketers in the sense that we seek agreement to our views and expect a positive response from those with whom we associate. The Buddha, in one of his discourses, has indicated that the world depends 100 percent on relationships. This is equally applicable to all phenomena in nature, including human relationships. The quality of the relationships is the key determinant of the success or failure of the quality of any human activity. On thinking broadly, quality is a rather evasive term with a wide variety of interpretations, reminding us of the proverbial ‘seven blind men and the elephant’.
My experience with the ISO certifications naturally prompts me to seek information from the ISO standards. A widely accepted and general definition of quality is the level to which requirements are fulfilled. According to the ISO 9001:2015 QMS, the customer requirements are broadly categorised as: (a) stated requirements, (b) implied requirements and (c) compliance obligations dealing with statutory and regulatory, and other legal requirements. Requirements stated by the customers are apparently straightforward but may need careful evaluation, while the implied requirements need to be invariably derived using the available information and the experience of the supplier or the manufacturer.
At the very beginning, the ISO 9001:2015 standard gives top priority to understanding the context of the organisation, which takes in to account the external and internal issues as well as the expectations of the external and internal interested parties while assessing the business risks and opportunities associated with the same. It is rather discouraging to note that many companies do not pay the due attention to Clause 4.0 in their quality management systems.
The concept of ‘internal customer’ is another important area that is apparently taken for granted in many companies despite the complex dependency and the independency between the processes and the process owners. The several ‘meetings’ that the managers are frequently engaged in – to the level of becoming a malady – could be the outcome of not paying attention to the ‘internal customer’. Habits 4, 5 and 6 of Stephen Covey’s ‘The 7 Habits of Highly Effective People’, namely Think Win/Win; Seek First to Understand, Then to Be Understood and Synergize, can be of valuable guidance in interpersonal relationships. Not understanding the requirements of the ’internal customer’ or the next in line in the value adding process has created closed domains and ivory towers within organisations.
As I have mentioned in one of my previous articles, ‘social distancing’ cannot be considered as post-Covid addition to our vocabulary. Its origins can be traced back to the post industrial revolution, when the traditional craftsmanship and cottage industries gave way for mass production system, which simultaneously resulted in mass de-personalisation. Individual craftsmanship was the norm in my native village in Sri Lanka (then Ceylon) in the fifties. I presume that some of the surviving ‘baby boomers’ can recollect similar experiences in their own countries. Pride of ownership and personal reputation were considered in high esteem – sometimes even at the expense of a little extra profit..
Notwithstanding the tremendous benefits accrued by way of increasing the agility and responsiveness with tools and conveniences of modern communications in the modern organisations, the distancing of relationships has introduced new problems. The importance given to the ‘personal touch’ appears to be the hallmark of an extinct species.
On the same lines, I remember an episode from my days in Nairobi, Kenya in the early nineties, how the owner of a well-known chain of hotels got his Harvard MBA son to work in a hotel kitchen as his first job and set a practical example of humanely understanding the customer psyche. Similarly, when I joined the Bata Shoe Company in 1969 as a management trainee, the first training we were given was to work in the retail shops for one week, irrespective of whether we are going to end up in marketing, purchasing, finance, technical or quality control. I still possess the leaflet we were given on the first day we joined the company, the contents of which goes as follows:
WHO IS A CUSTOMER
• A customer is the most important person ever in our business…in person or by mail.
• Customers are not an interruption to our work…they are the purpose of it.
• We are not doing them a favour by serving them…they are doing us a favour by giving us an opportunity to serve them.
• Customers are not dependent on us…we are dependent on them.
• A customer is not an outsider to our business…but a part of it.
• Customers are not cold statistics…they are flesh and blood human beings with feelings and emotions like our own, and with biases and prejudices.
• A customer is not someone to argue…and match wits with. Nobody ever won an argument with a customer.
• Customers are people who bring us their wants. It is our job to handle them profitably, to them and to ourselves.
Honestly, I should say that as a freshly joined management trainee in 1969, it took me many years to realise the implications of these time-honoured pearls of wisdom about interpersonal relationships. With the proliferation of online sales and e-marketing, the customer has become an obscure or virtual figure or a non-entity. Going to the bank and exchanging greetings with the counter clerk or having a friendly chat with the vegetable or fruit vendor down the street is a thing of the past and a luxury which only a few retired persons like me can afford to enjoy.
Voluminous studies and research have been done in the past from the time the human relations approach to management which started about 100 years ago. It is still an area that the modern day management thinkers, CEOs and specialists of the many disciplines related to human behaviour are grappling with. New theories and hypotheses are continually emerging. The modern managers are very often overwhelmed by the challenge of discerning the trees from the forest, and I am aware about two companies in my own country that were duped by ‘marketing experts’ – to spend millions on magnanimous customer relations programmes which proved to be failures.
Customer satisfaction is a requirement of performance evaluation under Clause 9.0 of ISO 9001:2015. Some companies have developed rather intricate quantitative methods to evaluate customer satisfaction. Poor response rates are a common trend unless the products or the services are of a high level of importance and the consequences of failures are catastrophic. The cost of not fully comprehending what the customers want can be high and the consequences can sometimes be disastrous.
The behaviour and body language – the genuine vs the artificial smile – can be easily spotted. It could be the glittering front office of a large multinational company or an airline check-in counter or the flight cabin itself. Or it may be a small kiosk or a boutique in a remote village. The underlying principles are the same. The courteous, patient and the enduring etiquette of the saree vendors in many parts of India and the remarkable business success of some minor communities in Sri Lanka provide good examples of staying close to the customers.
Customer satisfaction is the extent to which we strive to meet the needs of the customers. However, the way the modern market promotion and advertising is continuously striving to create new needs and wants with only the financial bottom-line as the supreme priority makes me wonder if we have a ‘hen and the egg’ situation in modern business. It was Mahatma Gandhi who once said, “The world has enough for everyone's need, but not enough for everyone's greed.”
According to a recent market study, some common pitfalls of poor customer experience are enumerated as:
a) Rushing it
b) Losing focus
c) Assuming satisfaction, loyalty, advocacy is the same
d) Letting the stakeholders to influence the customers
e) Making rash decisions
f) Comparing apples to oranges
g) Keeping it as a secret
h) Ignoring the data
i) Thinking short term
j) Standing still
Some important aspects to be considered in understanding the customer behaviour have been identified as follows:
• Marketing positioning and distribution
• Personal factors such as age, gender, education and upbringing
• Psychological factors such as buying motives, perceptions and attitudes
• Situational factors such as physical surroundings, social surroundings and time factor
• Social factors such as social status, reference groups, social media and family
• Cultural factors such as religion and ethnicity
• Lifestyle factors such as status, income and identity
• Geographical factors such as the country, religion, urban or rural
With all due respect to the modern approaches to understanding the customers, I find it opportune to cite a far-reaching teaching from the Buddhist doctrine which has deeper management implications on interpersonal relationships. Once the Buddha noticed a young person called Sigala, from an affluent Brahmin family, worshiping reverently at different directions after having his ritualistic bath at the Ganges. It was found that he was following the death wish of his late father. The Buddha explained to him the real significance of the six directions of worship, which is a lesson for the modern managers on harmonious interpersonal relationships. The discourse covers in great detail the duties and responsibilities of the different stakeholders of the social fabric, namely:
• Parents-children
• Students-teachers
• Husband-wife
• Friends and associates
• Employer-employee
• Individual-religious fraternity
It can be seen how these interactive factors cover every aspect of our lives on a life course approach, irrespective of geographical, national, social and religious boundaries, in a world made complicated by our own ambitions and actions.
- wellness
- efficiency
- National Productivity Secretariat of Sri Lanka
- Malcolm Baldrige National Quality Award
- USA
Efficiency And Effectiveness: Looking Beyond Productivity
- By P P Perera
- November 09, 2026
On the first of September this year, I completed 58 years of my career in the rubber industry, after starting as a trainee in a medium-scale footwear company in Sri Lanka. Now, at the ripe age of 80 and coming from the ‘Baby Boomers’ generation (1945–1964), I feel it would be worthwhile for the managers of the current generation, some of whom are in Gen Z (1997–2012), with the majority being Millennials or Generation Y (1987–1996), to gain some insights into the changing perspectives of productivity through the generations. On a more personal and sentimental note, I feel that this would be an attempt to compile reflective thoughts from my career in the manufacturing industry.
My first encounters with productivity can be traced back to my early childhood and rural upbringing, where the thoughtful use and conservation of materials, mainly food and clothing, as well as reuse and recycling, were practiced long before the concepts of the circular economy and green productivity became widely emphasised in modern times. The simplicity of lifestyles and households, along with the cleanliness and housekeeping practices seen at our ancestral homes and the village temple, are reflections that come to my mind. Although I did not have any idea about productivity as it is labelled today, I now realise that it was ingrained in our culture, and we in our part of the world are used to reinventing the wheel, perhaps as a remnant of colonialism. Notwithstanding this, it is always acknowledged that we must move with the times instead of resting on our laurels.
My first industry encounter with productivity was around 1970, when we were introduced to the inputs and outputs involved in using traditional resources: men, materials, machinery and money, and the mathematical ratio of achieving more with less. The specific concepts of resource utilisation, namely efficiency and effectiveness, were introduced and popularised as a contrasting pair in modern management by Peter Drucker in the mid-20th century, most notably in his book, The Practice of Management, in 1954. He formally crystallised the distinction that managers use today, with the famous definition:
Efficiency: ‘Doing things right’, maximising outputs while minimising resources consumed and waste.
Effectiveness: ‘Doing the right things’, pursuing the correct goals and achieving the intended results.
In conventional practice, productivity ratios, cost reductions, process optimisation, lean manufacturing and waste elimination are the traditional measures of productivity.
On the other hand, effectiveness measures the extent to which intended objectives are achieved. An organisation can be highly efficient but ineffective if it performs the wrong activities exceptionally well. Conversely, it may achieve its objectives effectively while using resources inefficiently. Together, efficiency and effectiveness have formed the cornerstone of modern management thinking and have served as the primary yardsticks for measuring success, organisational performance and the achievement of rewards.
These definitions have withstood the challenges of time for more than five decades. In my own experience, efficiency has more technical and operational utility and plays a major role in directing our activities through the first two or three decades of our careers, while effectiveness has a more subjective aspect, which often poses challenging dilemmas for the corporate and managerial sectors.
Despite their universal use, an important question remains: Do the conventional interpretations depict the complete picture, or are they merely helping us examine the individual trees while missing the forest? In an era where organisations navigate increasingly complex economic, technological, social and environmental challenges, it is timely to reconsider whether the traditional definitions of efficiency and effectiveness, which we have been accustomed to throughout our careers, are sufficient to define genuine success.
The traditional interpretation mainly concentrates on measurable outputs, such as production volumes, profits, market share, return on investment and operational excellence. While there is no doubt that these indicators are important, they primarily represent the economic dimension of organisational success. Based on what I have witnessed in the few organisations I have visited over the past few years, managers are overly occupied with productivity metrics or KPIs, resulting in a KPI subculture, where they think, talk, walk, eat and sometimes even sleep with KPIs.
Over the past three months, I had the opportunity to participate in field visits to assess applicants for the National Productivity Awards 2025/26, which was organised by the National Productivity Secretariat of Sri Lanka, a government-based institution. Although this has been a well-regarded biennial national event, its frequency was disrupted due to the outbreak of Covid-19 and the politico-economic disturbances in the ensuing years. Hence, a rejuvenated interest and enthusiasm were demonstrated by most of the applicant organisations, numbering about 2,000 and covering the state sector, education, healthcare and private organisations. The evaluation criteria, which were based on the Malcolm Baldrige National Quality Award, USA, in 1987, covered seven core areas:
- Leadership
- Strategic planning
- Customer and market focus
- Measurement, analysis and knowledge management
- Human resource focus
- Process management
- Business results.
I am currently conducting field assessments of companies aspiring to win the National Cleaner Production Awards, where the key evaluation criteria are resource efficiency, waste reduction, responsible sourcing, green productivity, GHG emissions, eco-labelling and life-cycle implementation.
I consider engaging in such assessments at government administrative institutions, service and utility providers such as water and electricity providers, schools, manufacturing organisations and tea plantations, to name a few, to be a challenging and mentally satisfying endeavour because it gives me the opportunity to reflectively examine activities using the knowledge, experience and insights assimilated during my working life of 58 years. In some instances, I was highly impressed by the dynamism and enthusiasm demonstrated by the young managers of certain organisations. On the other hand, I am saddened to see that while most of them, ranging in age from their late twenties to early forties, were competent in their disciplines and fields of specialisation, their grasp of the total picture leaves much to be desired. Looking back, I recollect how I also went through a similar stage in my working life. The remarkable contrast is that the pace of change in every conceivable sphere is astonishingly fast in the current era.
The familiar expression ‘not seeing the forest for the trees’ aptly describes this situation.
Efficiency and effectiveness are instruments for achieving desired outcomes. They are not ends in themselves. When organisations become excessively preoccupied with productivity metrics, they risk overlooking the broader purpose of their existence. If these are only intermediate measures, what should be regarded as the ultimate measure of success? A more overarching answer lies in human well-being. To what extent do economic growth, technological advancement and organisational profitability add value and contribute to improving the quality of human life?
We cannot simply interpret well-being as the absence of illness or as employee happiness in the modern-day context. It is a multi-dimensional concept encompassing the physical, mental, social and spiritual dimensions of human life. These are closely interconnected. Any weakness in one can eventually influence the others and finally affect both individual and organisational performance.
At this juncture, it would be interesting to note how the Buddha had identified 2,500 years ago the four dimensions of human well-being as physical, mental, social and spiritual. It sometimes makes us wonder whether we are trying to re-invent the wheel.
a) Physical well-being (The foundation)
Healthy employees possess the energy and vitality necessary for sustained performance. Safe workplaces, ergonomic design, balanced workloads, healthy lifestyles and occupational health programmes contribute directly to long-term organisational success.
b) Mental well-being (Quality of the mind)
Rapid technological change, constant connectivity, information overload, unrealistic targets and job insecurity have significantly increased stress and burnout. Mental resilience, psychological safety, opportunities for learning and meaningful work have become essential components of organisational effectiveness.
c) Social well-being ( The power of relationships)
Human beings are inherently social. Trust, teamwork, fairness, inclusion, compassion, respect and a sense of belonging strengthen organisations far more than competitive individualism. Healthy interpersonal relationships create resilient organisations capable of adapting to change.
d) Spiritual well-being (Meaning, values and purpose)
Spiritual well-being does not necessarily imply religious belief. Rather, it reflects purpose, integrity, ethical conduct, inner peace, compassion and alignment between personal values and organisational values. Individuals who find meaning in their work often demonstrate higher commitment, creativity and resilience.
In the context of traditional management, productivity is primarily viewed as the relationship between inputs and outputs. However, people are not simply another input. While machines can be replaced, processes can be redesigned and technology can be updated, human beings bring experience, judgement, relationships, creativity, intuition and values. These qualities cannot be meaningfully captured through conventional productivity metrics. This, however, does not mean that efficiency and effectiveness are no longer important. The fact is that they are necessary but not sufficient conditions for sustainable growth. They are just means to an end. An organisation can probably achieve impressive short term results by continuously striving to increase targets, reduce costs and demanding more from its people. This apparent productivity gain can eventually become a liability if this approach leads to exhaustion, disengagement, declining morale, conflict and loss of experienced people. Sustainable productivity must therefore consider both organisational performance and human sustainability.
During past few years, management thought has seen a proliferation of new terminology such as sustainability, sustainable development goals (SDGs), RSG, social responsibility, corporate citizenship, green productivity and inclusive growth. Each of these concepts points to a genuine attempt to expand and broaden the traditional term of organisational success.
Yet the uncomfortable question is whether we have fundamentally changed the purpose of business or have we ingeniously developed new and more sophisticated terminology to describe the same age-old economic objectives. The social bottom line should not be another column in the annual sustainability report.
The paradigm shift should ideally be from ‘Profit with Purpose’ to ‘Purpose with Profit’. This, however, is a speculative question to ponder, much like the famous line ‘to be or not to be’ from William Shakespeare’s tragic play Hamlet.
The author is a Management Counsellor from Sri Lanka.
Tyre Making: Engineering’s Last Black Art
- By Adam Gosling
- November 03, 2026
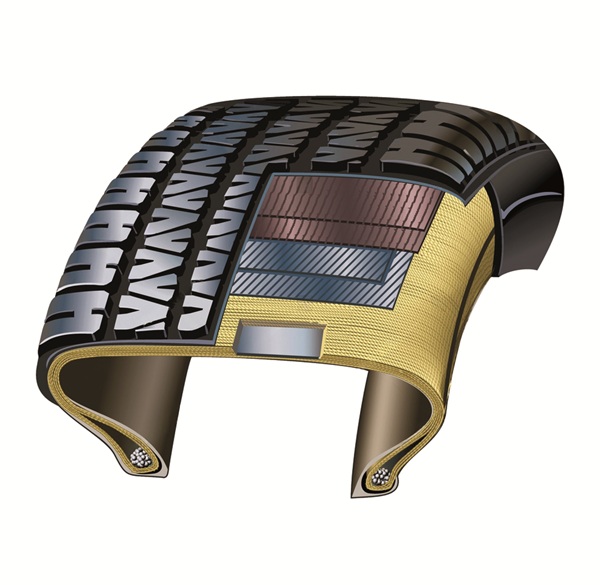
Tyre manufacturing, the black art of bringing seemingly incompatible materials together into a flexible pressure container matrix that will stand being driven over rough surfaces at high speed. Tyres have the reputation of being the most complex single item on a modern motor vehicle. F1 cars are not limited by their engines or aerodynamics; the tyres are the limiting factor. How many people getting into their car or onto a bus for their daily commute even consider what is supporting the machine they are riding in … in my honest opinion <1 percent.
The art (and I say this quite deliberately) of getting rubber to adhere to a steel cable is very deep (and some say troublesome) level, or some may say science, but I prefer to think black magic. Even the layup design of the cables of the high-quality steel filaments that are wound together to form the essential strength of the radial tyre is absolutely critical. Rubber must adhere to the steel at a rate of 100 percent. Having witnessed corrosion progressing along individual wound cables, I can attest to the fact that if there is a gap in the structure, it will be filled eventually; nature abhors a vacuum.
The metals used to promote the adherence of the rubber are special; you can’t go to the metal shop and buy them off the shelf. In the recycling industry, tyre steel is always a highly sought after product as the quality and properties of the steel make it high value. This steel accounts for some 15–20 percent of the tyre’s mass.
There are three distinctly different profiles of steel in a modern steel radial tyre. The body cords are laid up into cables, whereas the steel belts as we know them are a different design with individual filaments formed into a steel mesh. Again, this steel has to be treated or coated so as to engage the rubber of the belt and tread package to adhere and meld into a single unit during curing. Then there are the bead bundles, worthy of another discussion but subject to the same requirements of steel to rubber adhesion.
Like a lot of manufacturing these days, robots are continuing to overtake humans as the preferred method of building. The reasons are the same as every other industry – machines don’t need meal or toilet breaks, aren’t given annual holidays or public holidays, but most importantly, the machines are extremely accurate in performing their duties.
Having inspected numerous tyres over my career, I have observed on enough occasions the internal elements are not as per the design. Whilst the green (uncured) tyre can be laid up as per design, when the green tyre is placed into the mould for curing, any control is lost. The design of the mould becomes another highly critical factor. The mould has to be closed without disturbing the design requirements. Under pressure, the rubber has to flow into the tread design evenly and without flow laminations, the belt packages must adhere to the body cords and everything must stay in alignment, which is a huge ask. Like baking a loaf of bread or a cake, when it goes into the oven, the final product must align with the design.
With the computing power behind AI, such designs can be simulated or trialled in coding rather than producing a steel mould only to find it doesn’t work as expected. In the early days of giant OTR bias tyre manufacturing, I included strips of white rubber onto the green tyre before it was placed into the mould. These strips showed just how much the rubber moves during the expansion of the green tyre into the mould cavities. This was a time consuming and expensive exercise as the tyre was
not saleable; it was a trial tyre only. These development costs all flow into the retail costs; volumes of scale are evident in tyre manufacturing.
With the performance of the modern motor vehicle, we ask and expect so much more of our tyres; they have to be quiet and smooth, grip the pavement in all circumstances, and did I forget, they must last the life of the vehicle as people don’t wish to replace their tyres as often as they should. Then, above all, the tyres have to be low cost; I don’t say cheap as quality is often the first victim of a cheap manufacturing exercise.
As we’ve observed, large-scale manufacturing can and does affect the end result. One only has to consider the rise of EVs to understand just how change in magnitudes can happen when technology takes over. Some may say for the good, while others the polar opposite.
Think about ADAS (auto driver assistance systems); some say useful, others say it’s just a pain. What would happen if this same technology was applied to a tyre? The driver wants to go one way, the car the other; now we think the tyre is trying to do something otherwise, technology tying itself in knots.
I believe we are about to see the same large magnitude changes coming to tyres where information from the tyre is fed into the ECU on the vehicle to determine how much power or braking is applied, what steering angle can be deployed considering the traction available; this is all driving towards autonomously controlled vehicles. Think about this level of change for a minute. Just this weekend, we’ve seen robots break Usain Bolt’s 100 metre running record. Some looked like a tyre gator after they’d finished, but nevertheless, it demonstrates how has fast technology is changing. I’m not sure that I can fully understand let alone digest this progress. No need to call me a dinosaur, I already wear that label.
With the combination of AI and robotics, manufacturing is entering a new age where quantum steps will be made. How do we as humans deal with this?
Do we continue to drive our cars manually or hand over some or all control to machines?
I for one will continue driving my vehicles manually for the most; sure I use cruise control, but having the vehicle steer for me, no thanks. Just as in aviation the pilot earns their money when the stuff is dripping from the fan, when things don’t go right, humans can still engage in extraction from the hazardous situation, most times. If we haven’t programmed a machine to deal with the circumstances it encounters, how is it going to deal with ‘it’? Human decision making is still (at this point in time) required. What happens when human decision is no longer required?
Take care. Look after your tyres frequently or at least regularly.
Why The Future Of Manufacturing Needs An India–Latin America–China Dialogue
The future of manufacturing is no longer being shaped by technology alone.
Artificial intelligence, automation and advanced materials will certainly transform factories. But geopolitics, trade tensions, access to raw materials and supply-chain security are increasingly determining where companies produce, where they invest and how industrial capacity is distributed around the world.
For the tyre industry, this shift is already visible. Manufacturers are reconsidering their global footprints. Production is moving closer to strategic markets, supply chains are being diversified and companies are balancing efficiency against the risks of excessive dependence on individual countries, suppliers or transport routes.
Manufacturing capacity is once again becoming strategic capacity. And that should lead us to reconsider not only how industrial value is created, but what happens to that value once a product leaves the factory.
THE VALUE ALREADY MANUFACTURED
Can a tyre be considered truly sustainable if it is manufactured efficiently but cannot remain in use?
At first sight, this may appear to be a question about retreading, but it is a question about manufacturing.
When a commercial tyre leaves a factory, it contains much more than rubber and steel. It embodies raw materials, energy, engineering, technology, labour and manufacturing capacity. Considerable industrial value has already been created.
The strategic question, therefore, is not only how efficiently we can manufacture the next tyre. It is also how effectively we can preserve the value of the tyre we have already manufactured by keeping it in productive use.
If access to raw materials matters strategically, using those materials intelligently should matter as well. If manufacturing capacity is valuable, preserving the value created by that capacity should also become part of industrial strategy.
This gives retreadability a different meaning.
Retreading is usually treated as a downstream activity, beginning once the manufacturer’s role has effectively ended. Yet the ability to keep a tyre in productive use begins much earlier. It is influenced by design, engineering, material selection and, fundamentally, the quality and durability of the casing.
Retreadability, therefore, is not only an issue for the retreading industry. It is also a manufacturing consideration.
This does not mean innovation should be constrained to accommodate existing retreading processes. The challenge is whether innovation can advance while preserving the ability of a valuable industrial product to remain safely and economically in use.
As we design the tyre of the future, are we also designing it to remain in use?
THE GEOPOLITICS OF A LOCALLY GROWN TYRE
As geopolitical uncertainty encourages local-for-local manufacturing, shorter supply chains and regional production, the tyre industry is rediscovering the strategic value of proximity. But perhaps the concept of local production should not end when the original tyre leaves the factory.
A retreaded commercial tyre has an interesting characteristic: much of the additional value required to keep that tyre operating can be generated locally.
The casing is already present in the economy. Its continued use can be enabled through local inspection, technical knowledge, skilled workers, retreading plants and domestic transport networks. In that sense, retreading can create something particularly relevant in a more fragmented global economy: a locally grown tyre.
The expression should not be understood literally. The original tyre may have been manufactured thousands of kilometres away and its raw materials may have originated in several countries.
What becomes local is the additional industrial value. An economy can use its own technical and industrial capabilities to keep an existing asset productive rather than depending exclusively on another newly manufactured product entering through an international supply chain.
For many Latin American economies, which remain dependent on imported tyres and industrial inputs, this has particular significance. But the principle reaches beyond Latin America. As countries debate reshoring, nearshoring, strategic autonomy and supply-chain resilience, keeping existing industrial assets in productive use deserves a place in that discussion.
Viewed through this lens, circularity is not only an environmental strategy. It can also become a resilience strategy.
WHY INDIA, LATIN AMERICA AND CHINA?
This brings us to an opportunity that deserves greater attention: an India–Latin America–China dialogue on circular tyre manufacturing. Its value lies precisely in the differences between the three regions.
India is strengthening its position as a global manufacturing power, combining growing international ambitions with an enormous domestic mobility market and significant requirements for raw materials. Latin America operates at a different scale but sits at the intersection of important industrial relationships with North America, Europe and Asia. Commercial tyre retreading has also been part of its transport economy for decades, providing practical experience in keeping manufactured assets in productive use. China brings another dimension: extraordinary manufacturing scale, technological depth and supply-chain capabilities that have reshaped the global tyre industry.
 The purpose would not be to determine which model is superior. None of these regions has all the answers. Their experiences are valuable precisely because they are different.
What could India’s manufacturing expansion learn from markets where extending product use has long been economically necessary? What could Latin America learn from the transformation of Asian manufacturing? And what could India, Latin America and China discover together about designing tyres whose industrial value can be preserved for longer?
Those questions could form the beginning of a very different relationship.
FROM TRADE TO INDUSTRIAL DIALOGUE
India, Latin America and China already have substantial commercial relationships. Tyres, machinery, raw materials, technology and investment move between these markets. But knowledge should move as well.
Much of the relationship between tyre-producing regions is still understood through exports, imports, tariffs and market access. These issues will remain fundamental, particularly as the international trading environment becomes more complex. But the restructuring of global manufacturing creates an opportunity to move from trade relationships towards industrial relationships.
 What should durability mean for the next generation of commercial tyres? Should retreadability become a more explicit consideration in advanced tyre design? Can digital traceability allow manufacturers, fleets and retreaders to better understand the history and remaining value of a casing? And can circular economy policies distinguish more effectively between recovering materials and keeping a manufactured product in productive use?
These are not simply questions about retreading.
They are questions about how industrial value should be managed in the future. Industry associations are particularly well positioned to begin that conversation. Companies naturally approach these issues through commercial interests, while governments see them through trade, industrial or environmental policy. Associations can occupy the space between them, connecting manufacturers, retreaders, fleets, technology providers, researchers and policymakers.
An India–Latin America–China dialogue does not require another international organisation, nor should it begin by attempting to harmonise three very different markets. It could start simply as an exchange about how we manufacture, how long we use and how much industrial value we are capable of preserving.
The purpose would not be to demonstrate that one region has found the correct model. It would be to ask better questions together.
BEYOND THE FACTORY GATE
The factory of the future will undoubtedly be smarter. Artificial intelligence, automation, advanced materials and increasingly efficient production systems will transform how tyres are manufactured. But geopolitics is reminding industry that efficiency alone does not determine industrial strength. Resilience matters. Access to resources matters. Manufacturing capability matters. And the ability to make better use of what an economy already possesses may matter increasingly as well.
For the tyre industry, that means looking beyond the factory gate – not only towards what happens when a tyre eventually becomes waste but towards what happens to the industrial value created when that tyre was manufactured in the first place.
Can a tyre be considered truly sustainable if it is manufactured efficiently but cannot remain in use? Perhaps the future of manufacturing should not be measured only by how intelligently we create industrial value. It should also be measured by how intelligently we keep that value in use.
For a global industry navigating a more fragmented and uncertain world, that may prove to be much more than a circular economy argument. It may become an industrial strategy.
And that is a conversation India, Latin America and China should start together.
Study On Tyre Strength Issues And Evaluation Methods
- By Zhong Ma
- October 26, 2026
The focus of tyre regulations has shifted towards sustainability. Our research on passenger car radial tyres (PCR) strength evaluation and the strength testing requirements in the IS15633 standard aligns precisely with this trend. Before discussing why, the traditional plunger-strength test has become irrelevant for evaluating PCR tyres, let us first consider the benefits of eliminating it. Based on Continental’s engineering experience, waiving the strength test allows for an average reduction of 0.7 kg (range: 0.5–0.9 kg) in cap ply material. This translates to saving approximately USD 0.70 in material costs per tyre while simultaneously lowering rolling resistance, which yields a carbon reduction benefit of about 6 kg per tyre in-use-phase. Given that the Indian PCR market involves approximately 32 million replacement and 20 million original equipment PCR tyres, the potential annual impact includes saving roughly 40,000 tonnes of material, cutting costs by about USD 43 million and reducing carbon emissions by approximately 370,000 tonnes; over a 10- to 20-year horizon, these would yield substantial societal sustainability benefit. This paper examines the history of the strength test and addresses the issue of its unsuitability for evaluating PCR tyres and provides supporting arguments to help realise these prospective benefits.
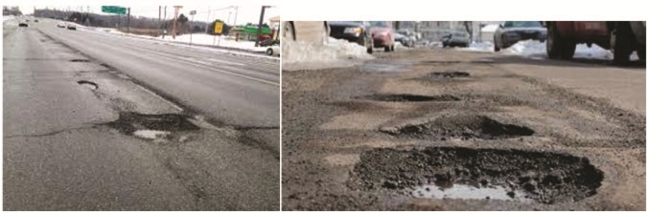
It is well‑documented that tyre‑strength testing originated to address road‑hazard impact damage. Tyre strength evaluation protocols were developed specifically to address damage caused by such impacts. Literature indicates that, starting in the 1960s, tyre‑and‑wheel damage caused by striking potholes, road shoulders or curbs became a major safety concern for automotive OEMs. The Society of Automotive Engineers (SAE) categorised this form of damaging impact as ‘road hazard impacts’. Over the following six decades, multiple test methodologies – including tyre strength tests (Plunger test), pendulum‑impact tests and full‑vehicle obstacle‑impact tests – were developed for new PCR to assess road‑hazard‑impact effects on treads, sidewalls and wheel assemblies. This work clarifies the fundamental nature of tyre‑strength‑related problems and traces the origin and evolution of these test methods. It aims to furnish a technical basis for industry and regulatory authorities to revise strength‑test standards and to support tyre manufacturers and vehicle OEMs in appropriately applying these evaluation methods when resolving consumer complaints about tyre performance.
I. WHAT IS A ROAD‑HAZARD IMPACT?
Damage to tyres and wheels resulting from driving over potholes or obstacles such as curbs and speed bumps is defined as a damaging road‑hazard impact (Figure 1). Such events remain common on real‑world roads today.
II. WHAT IS TYRE-STRENGTH EVALUATION?
Tyre‑strength evaluation assesses the external‑force thresholds at which a tyre undergoes structural failure, as well as the corresponding failure force and energy levels. Structural failure denotes rupture of reinforcing cords within the carcass, cap ply or belt layers, leading to air leakage, bulging or related defects. It is critical to distinguish air leakage caused by sharp‑object punctures – a puncture‑resistance and air‑retention concern – from true structural‑strength failure. Sharp‑object punctures can often be repaired, or leakage mitigated through sealant application. By contrast, structural damage arising from severe road‑hazard impacts is non‑repairable. Major tyre‑industry associations uniformly advise consumers against continuing service use of tyres that have sustained such structural failure.
We emphasise that air leakage from sharp‑object punctures does not constitute a tyre‑strength issue. A comparison between damage generated in a plunger‑type strength test (Figure 2(a)) and nail puncture damage (Figure 2(b)) highlights this distinction: plunger‑induced failure ruptures belt layers and creates large tears in the inner liner, whereas nail‑style sharp‑object punctures do not rupture reinforcing layers and produce only a small inner‑liner wound.
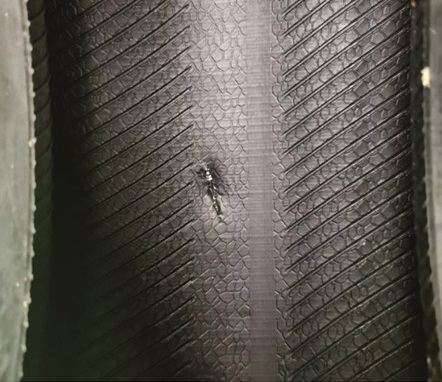
Figure 2(a) Tyre damage caused by plunger strength test
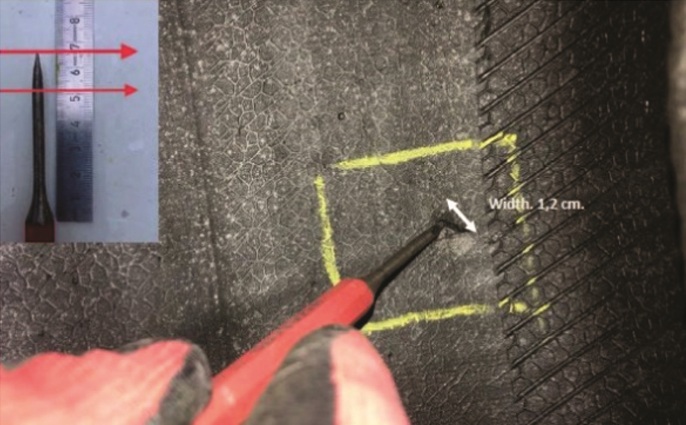
Figure 2(b) Tyre damage caused by nail puncture88
III. DISTINCT DAMAGE PATTERNS FROM ROAD‑HAZARD IMPACTS: RADIAL VERSUS BIAS‑PLY TYRES
Research demonstrates that road‑hazard‑impact damage manifests differently for bias‑ply and radial tyres. For bias‑ply tyres, impacts predominantly generate crown‑region damage; for radial tyres, impacts most commonly produce sidewall bulging and wheel‑assembly damage.
These divergent failure modes stem from fundamental structural and material differences between the two tyre architectures. As shown in Figure 3(a), bias‑ply tyres use rayon, nylon or polyester reinforcing plies arranged in criss‑cross orientations at angles below 90° relative to the tread centreline, running continuously from one bead to the opposite bead. This forms a monolithic structure with high overall integrity and stiff sidewalls. The tyre resists bending, and its constituent structural elements do not deform independently under external loading. By comparison (Figure 3(b)), radial‑tyre carcass plies run at approximately 90° relative to the tread centreline, extending bead‑to‑bead. The tread circumference is further reinforced by two steel belt layers plus a rayon, nylon or polyester cap ply. This creates a dual‑component architecture: a rigid, robust crown coupled with a flexible, air‑spring‑like tyre body. The carcass exhibits high elasticity, sidewalls deform readily under load and the tyre absorbs road impacts with unique dynamic behaviour under external forces.
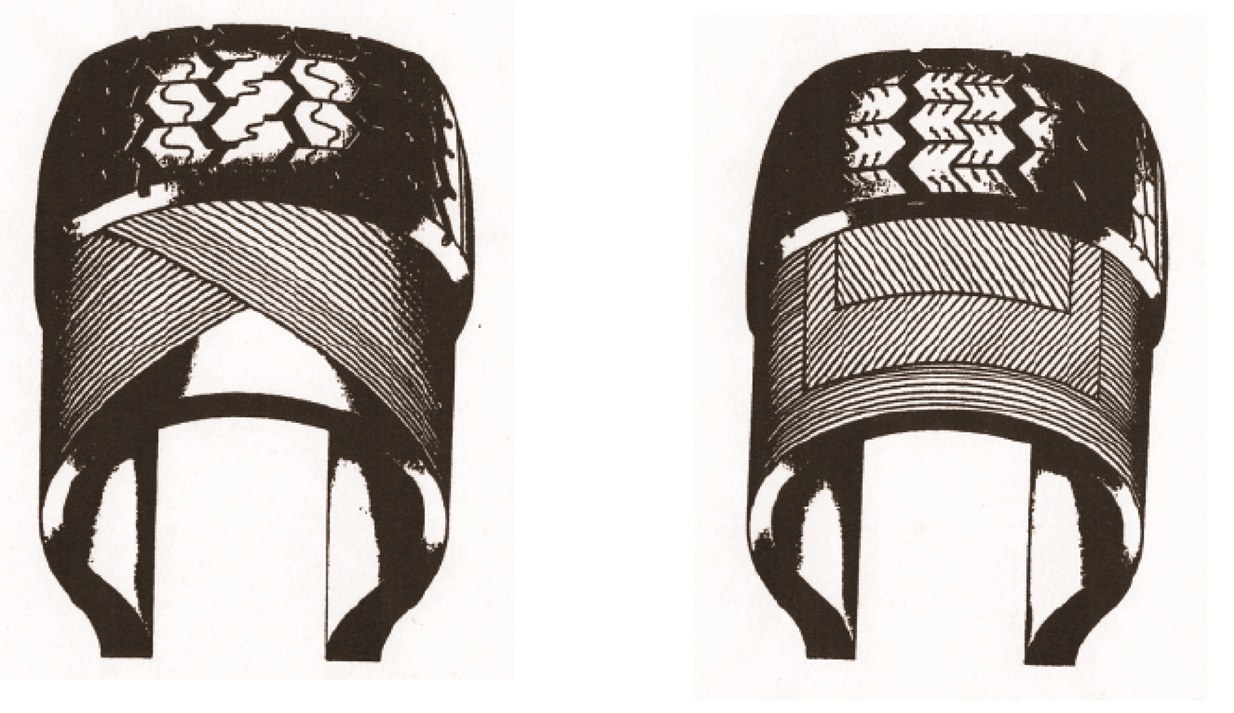
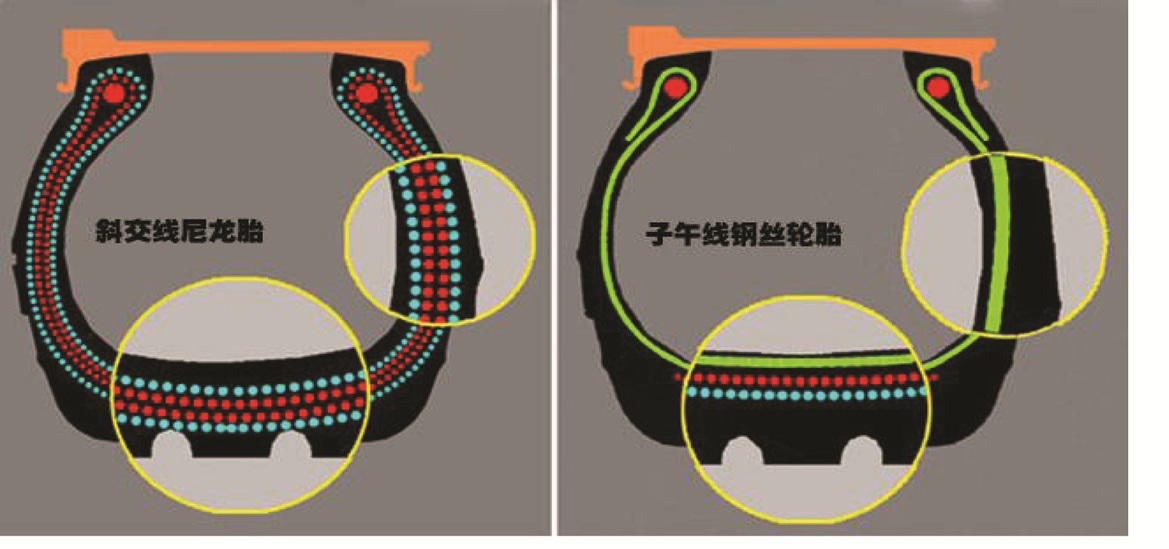 (Figure 3 (a) Schematic of bias-ply tyre design)
(Figure 3 (b) Schematic of radial tyre design)
THE STRUCTURAL CHARACTERISTICS OF BIAS-PLY AND RADIAL TYRES REVEAL THE FOLLOWING:
(1) The materials used for the circumferential cap ply and belt layers in radial tyres possess greater strength than the rayon, nylon or polyester belt materials found in bias-ply tyres;
(2) Because radial tyre sidewalls are highly flexible and prone to deformation, impact forces often cause damage to the vehicle suspension, rim or sidewall (such as bulging) before the tyre crown accumulates enough energy to suffer structural failure. Traditional strength testing involves a 19 mm plunger vertically compressing the tyre crown to simulate the forces experienced when a tyre strikes a small road obstacle (like a stone). CT images captured during a strength test of a 185/60R15 88T tyre clearly show that the plunger must descend almost to the point of touching the rim before it can puncture the crown plies and belt layers to reach the failure energy limit. This process causes incredible sidewall deformation due to the tyre’s high flexibility; however, in real-world driving conditions, the rim or suspension system would sustain damage long before the tyre could undergo such extreme deformation from a road impact.
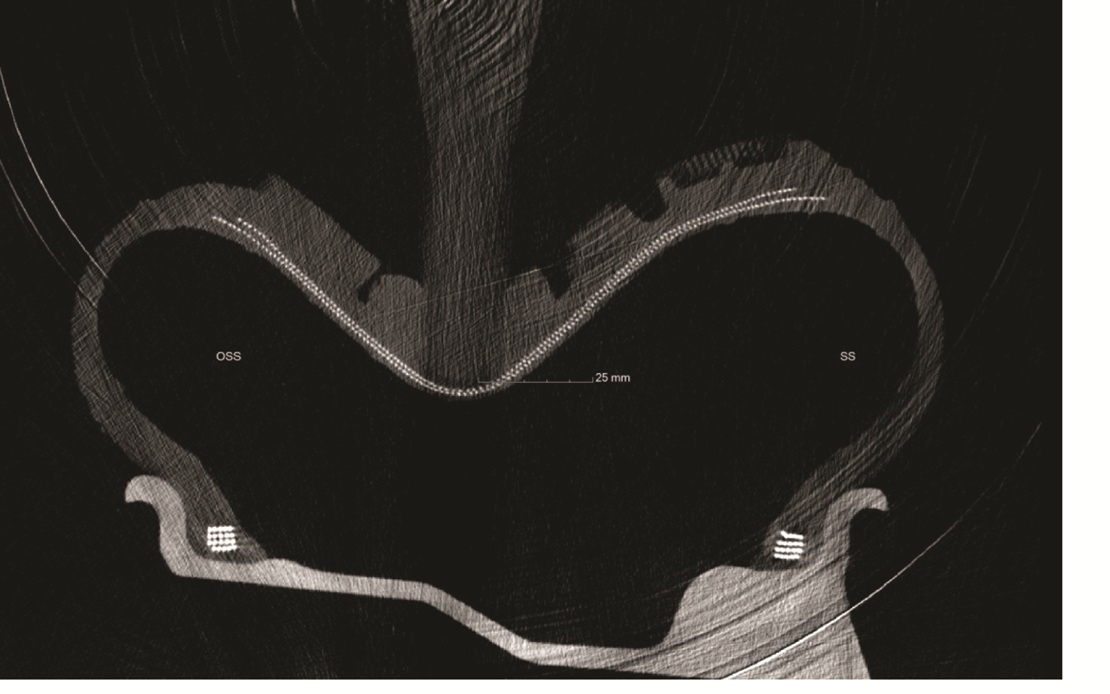 Figure 4 CT scan imagery captured during tyre‑strength testing
A detailed structural comparison between bias‑ply and radial tyres appears in the February 2020 paper Observations on Tyre Plunger Strength and Bead Unseating Performance by Professor Joseph D Walter (University of Akron). Walter notes that bias‑ply plies form a rhombic (parallelogram‑like) structural arrangement, while the combination of belt layers and carcass plies in radial tyres yields a triangulated structural configuration. Figure 5 contrasts the load‑driven deformation characteristics of these two architectures.
Within bias-ply tyres, measurable changes in cord angle occur repeatedly during the loading and unloading cycles of each tyre rotation; consequently, the rhombic structure of the bias plies is also referred to as a ‘shear’ structure. These angular changes induce significant shear strain within the rubber, leading to the accumulation of hysteretic heat – an effect that is markedly reduced in radial tyres due to their triangular structural configuration. In modern radial tyres, the carcass ply material (whether polyester or rayon) situated beneath the steel belt layers forms a stable triangular structure that reinforces the tread area. These deformation-resistant triangles provide vastly superior strength and rigidity compared to other structural designs. Without the underlying carcass plies, the belt cords – whether steel or textile – would simply form a non-rigid rhombic structure, resulting in performance characteristics identical to those of bias-ply tyres.
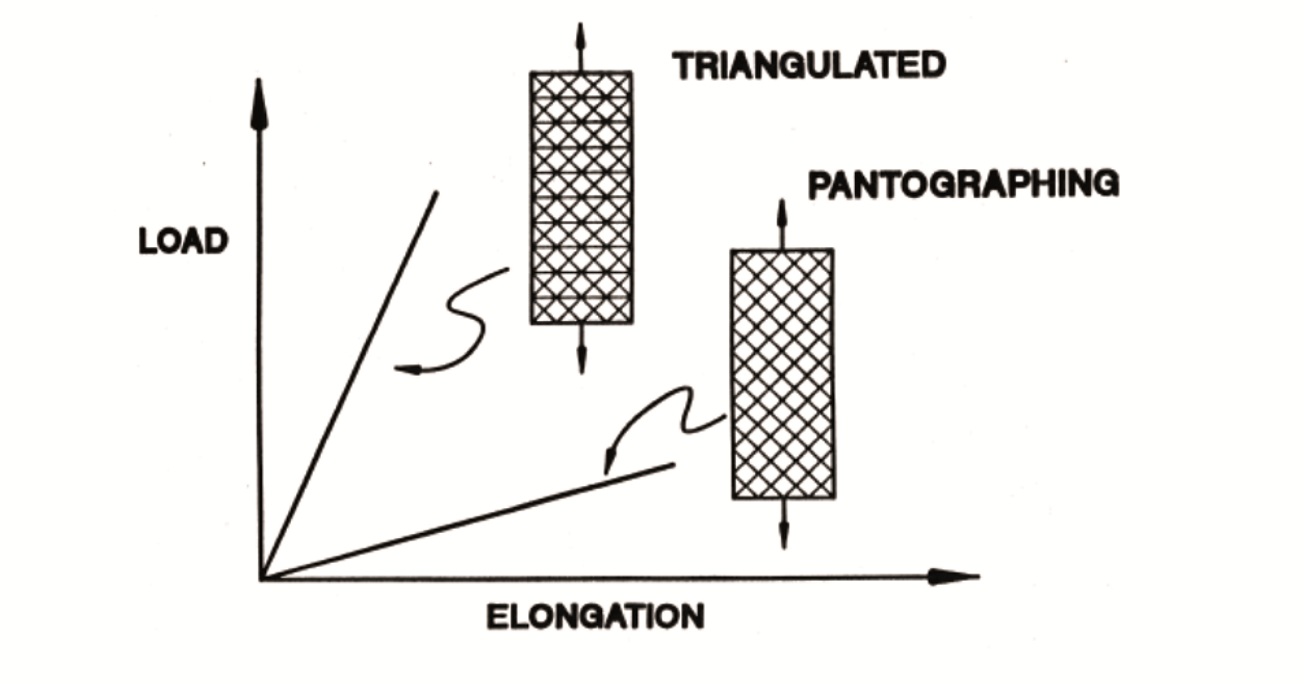
Figure 5 Deformation differences between rhombic‑shear and triangulated structures
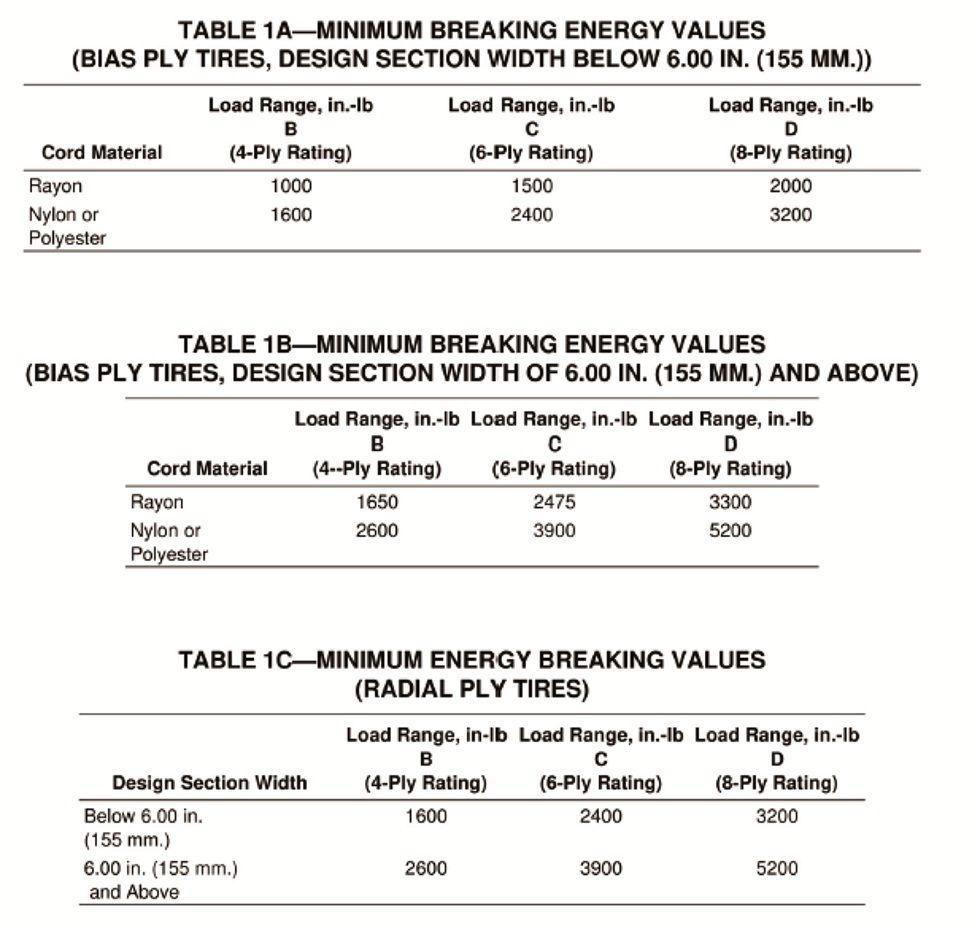 Figure 6 Strength‑evaluation criteria defined within SAE J918
In summary: the monolithic structure of bias‑ply tyres and dual‑component architecture of radial tyres produce fundamentally different failure modes under road‑hazard impact. Radial tyres deliver well‑established advantages in vehicle handling, ride comfort, service life, rolling resistance and lightweight performance. The industry’s shift from bias‑ply to radial construction necessitates updated assessment approaches for impact‑related damage, particularly for low‑aspect‑ratio radial tyres. Legacy strength‑evaluation criteria originally designed for bias‑ply tyres cannot simply be carried over unchanged.
IV. EVALUATION APPROACHES FOR ROAD‑HAZARD‑IMPACT DAMAGE
1. Road‑hazard‑impact evaluation for bias‑ply tyres:
Tyre‑strength testing and crown‑ply‑rupture assessment were pioneered in the United States. In 1965, SAE published SAE J918, Passenger Car Tyre Performance Requirements and Test Procedures, establishing tyre‑strength test procedures and defining minimum failure‑energy acceptance criteria for rayon‑, nylon‑and‑polyester‑constructed bias‑ply tyres.
Full original theoretical rationale for these early performance metrics is no longer traceable. Nevertheless, historical literature yields notable observations:
1) The standards specified higher strength limits for nylon or polyester than for rayon. In effect, strength‑performance limits were calibrated to match the tyre‑construction raw materials in use at that time.
2) The standards established minimum strength requirements not only for bias-ply tyres – which were the norm at the time – but also for radial tyres. Production radial passenger‑car tyres were not fitted as original equipment on US vehicles until 1970. Given the absence of vehicles equipped with radial tyres on the road back then, the limits clearly were not derived from real-world issues specific to radials; instead, the standards simply adopted the bias-ply strength limits – a practice that has persisted for 60 years despite the lack of an empirical basis regarding radial tyres.
2. Road‑hazard‑impact damage for radial‑ply tyres:
By the 1990s, radial‑tyre market penetration in the United States approached 90 percent. SAE practitioners then recognised that road‑hazard‑impact failure modes for radial tyres diverged sharply from those seen with legacy bias‑ply tyres. Real-world radial-tyre impact events typically produce sidewall or rim damage. The plunger‑style strength test, which was designed to assess tread‑crown robustness, provides little meaningful insight into these real‑world radial‑tyre failure modes. Accordingly, SAE released the SAE J1981 in 1994: Road Hazard Impact Test for Wheel/Tyre Assemblies, introducing pendulum-impact test to simulate damage to complete tyre‑wheel assemblies. In a February 2020 letter to the NHTSA (National Highway Traffic Safety Administration), the USTMA (U.S. Tyre Manufacturers Association) stated: “By 2000, the industry recognised that radial tyres were not susceptible to the specific damage modes targeted by [traditional] strength tests; automakers also observed that radial tyre sidewalls were relatively ‘soft’, meaning that impacts with potholes or obstacles often resulted in suspension or rim damage, or sidewall bulging, rather than tread-area failure.”
Our research highlights that both pendulum‑impact tests and plunger‑strength tests originated as successive SAE methodologies addressing road‑hazard hazards, reflecting the distinct failure physics of bias‑ply versus radial tyres. Additional supporting documentation comes from Tyre Laboratory Strength Test Validation Report (NHTSA‑2000‑8011‑0020). In March 2002, NHTSA floated a proposal to replace traditional plunger test with pendulum‑impact testing per SAE J1981, envisioning pendulum impact as a dynamic alternative for tyre‑strength assessment. Figure 7 displays representative impact strikers used within that NHTSA research programme, including wedge‑form impactors and a 50 mm cylindrical striker conceptually analogous to plunger tips used in commercial‑vehicle tyre‑strength testing.
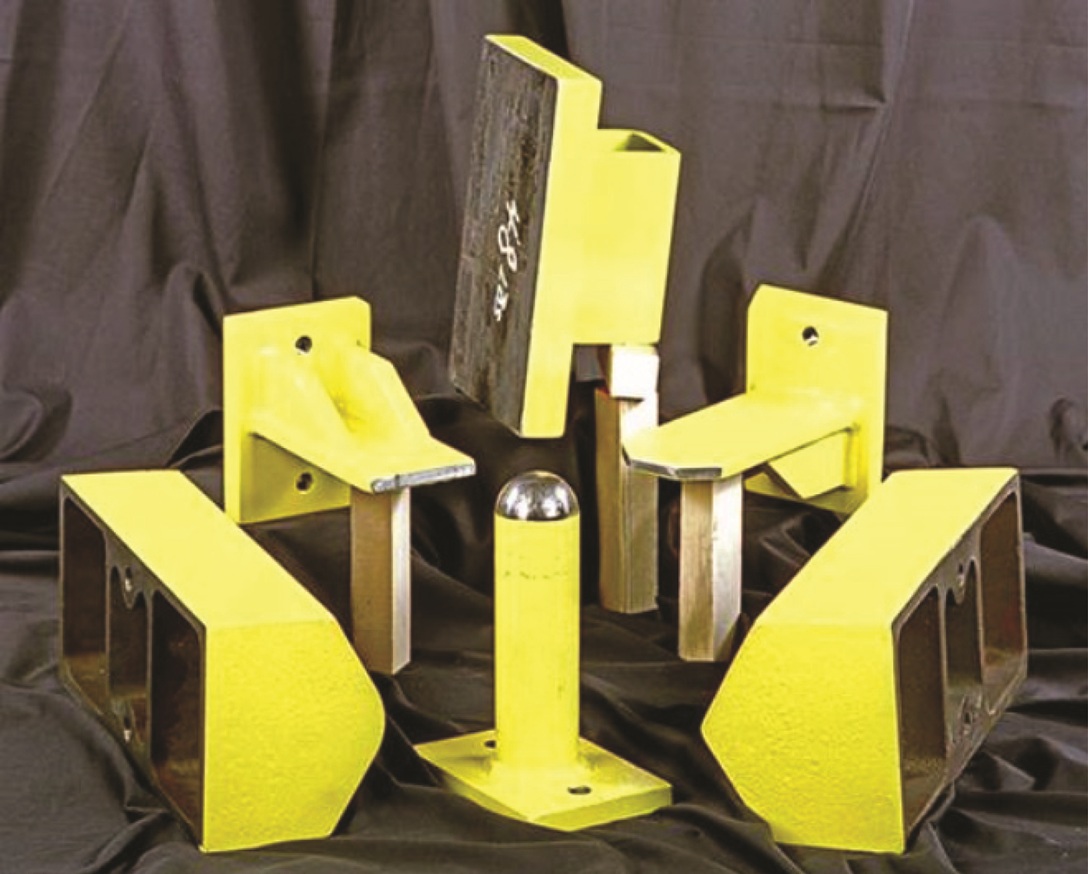 Figure 7 S Impact strikers evaluated for NHTSA pendulum‑surrogate‑strength‑test research
Test outcomes from this project disappointed NHTSA; the proposal failed to gain acceptance across tyre and automotive stakeholders. In 2002, the Rubber Manufacturers Association (RMA), Ford Motor Company and the European Tyre and Rubber Manufacturers’ Association (ETRMA) explicitly commented that pendulum‑impact testing primarily evaluates complete wheel‑assembly damage from road hazards. Its standalone suitability for assessing tyre‑intrinsic strength required further refinement and validation. As a result, NHTSA formally withdrew its proposal to substitute pendulum impact for plunger‑strength testing in June 2003, while research activities targeting radial‑tyre‑suited strength‑assessment methods continued.
During 2011‑2013, Germany’s VDA (German Association of the Automotive Industry) and WDK (German Rubber Industry Association) built upon SAE J1981 to investigate correlations between laboratory pendulum‑impact results and full‑vehicle impact behaviour. Their studies demonstrated poor correlation between pendulum‑impact measured energies and energies observed in full‑vehicle obstacle‑impact events, corroborating why NHTSA’s 2002 proposal could not succeed. WDK member companies nonetheless derived a dimensionless ‘f‑value’ via empirical formulas incorporating tyre‑geometric and load parameters; this f‑value exhibited partial correlation with full‑vehicle impact speeds. These research outputs were subsequently published within the VDA 11‑2016 technical guideline.
It should be noted that the validity of the f-factor evaluation relies on its correlation with vehicle impact speeds; if this correlation is disproven, the f-factor loses its viability. Furthermore, the f-value in the VDA-11 method is intended as a design reference for sidewall strength during the development of specific vehicle models, rather than as a general strength evaluation metric for tyres independent of specific vehicle models. We found that neither the SAE method nor the VDA f-value could serve as a general strength evaluation method for radial tyres without relying on parameters specific to a vehicle model (such as wheel assembly strength, suspension stiffness and vehicle load). To verify this finding and gather evidence, Continental Tyre conducted validation tests in China in collaboration with the National Tyre Quality Supervision and Inspection Center. By comparing vehicle-based impact tests and pendulum impact tests across two vehicle platforms and using various obstacle heights, the following observations were made:
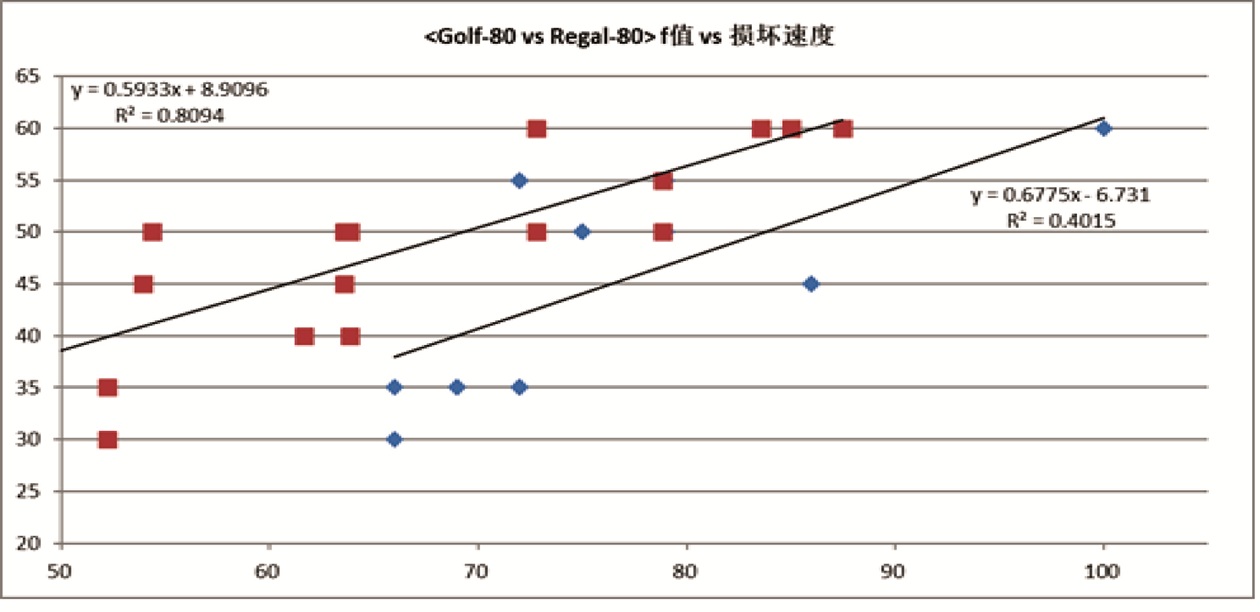
Figure 8 Comparative test results: Golf 7 versus Regal
(red data points = Golf 7; blue data points = Regal)
1. For one fixed vehicle platform, laboratory pendulum‑derived f‑values show partial correlation with real‑vehicle damage‑onset impact speeds, yet this correlation remains unstable. Substantial f‑value scatter can occur at constant impact velocity, and conversely, similar f‑values may correspond to very different impact speeds.
2. Tyres yielding identical f‑values in pendulum testing exhibit divergent damage‑threshold impact speeds when fitted on different production vehicles. In our test campaign, the ratio of damage‑threshold speeds for the Golf 7 and Regal vehicles approximated the ratio of their respective curb weights.
3. Damage‑threshold impact speeds show an approximately exponential dependence on obstacle height. Changing obstacle height therefore exerts an exponential influence on measured test outcomes. (Figure 9)
Many consumer complaints about sidewall bulging relate to damage incurred at relatively low driving speeds, for instance after striking potholes or kerbs. Defining
Figure 9 Regal impact‑test results: 80 mm vs 100 mm obstacle heights (red points = 100 mm obstacle height; blue points = 80 mm obstacle height)
tyre‑performance limits expressed via vehicle‑specific impact speeds or f‑factors – further adjusted for tyre aspect ratio – cannot adequately resolve real‑world consumer‑complaint scenarios. Such an approach also departs from the original technical intent of SAE‑and VDA‑defined pendulum‑based f‑values, which were conceived to correlate against full‑vehicle impact‑speed observations. Consequently, applying f‑factors or vehicle‑specific impact‑test outcomes as universal tyre‑strength‑evaluation criteria remains unfeasible at present.
Legacy plunger‑strength‑test procedures were conceived for bias‑ply tyres. A radial tyre’s plunger‑strength‑test performance tells us nothing about its real‑world propensity for sidewall bulging, rim damage or suspension damage following impact events. Plunger‑strength‑test results cannot characterise radial‑tyre road‑hazard‑impact robustness. Retaining the existing plunger‑strength‑test requirement for radial tyres solely for lack of a replacement methodology serves no practical purpose.
1. Provide sufficient consumer training explaining that radial tyres – particularly low‑aspect‑ratio variants – are inherently vulnerable to road‑hazard‑impact damage (e.g. pothole, curb strikes) as a direct consequence of their structural design.
2. Impact‑resistance degrades as tyre section height decreases. For vehicles intended for harsh‑road operating conditions (e.g. off‑road platforms), vehicle‑designers and end‑users should select appropriately‑specified tyres. Avoid fitting low‑aspect‑ratio wide tread tyres optimised for high‑performance road‑car track use onto off‑road‑oriented vehicles purely for aesthetic reasons.
3. Expand market‑level training and public guidance on identifying sidewall‑bulge damage and associated tyre‑replacement requirements, preventing tyres with observable bulges from remaining in‑service and creating safety hazards.
Radial‑tyre architecture delivers high‑stiffness crown regions paired with flexible, low‑stiffness sidewalls. Ongoing market trends towards lower aspect ratios exacerbate sidewall‑bulge failure risks. Industry stakeholders should communicate realistic operational limitations of radial tyres to end‑users and educate consumers on mitigating road‑hazard‑impact risks, rather than persisting with obsolete, functionally‑irrelevant legacy strength‑test requirements or adopting new, theoretically‑contested strength‑factor metrics to resolve real‑world service‑complaint tensions. In particular, hastily‑mandated sidewall‑strength minimum limits risk impeding market progress towards high‑performance, low‑aspect‑ratio radial‑tyre deployment.
We hope these preliminary research findings support industry and regulatory stakeholders addressing real‑world consumer‑and‑technical challenges. This work informs further deliberation over the continued applicability of legacy tyre‑strength testing, as well as the potential adoption constraints of pendulum‑impact‑based assessment and f‑factor methodologies, while preserving the dynamic‑performance and structural‑design advantages intrinsic to radial tyres.
VI. OUTLOOK FOR FUTURE RADIAL‑TYRE‑STRENGTH‑EVALUATION WORK
1. Owing to radial tyres’ structural‑mechanical characteristics, real‑world road‑hazard‑impact events predominantly produce sidewall damage; secondary damage may occur on wheel‑hubs or vehicle‑suspension components. Crown‑region structural failure is rarely observed. Accordingly, the existing plunger‑strength‑test methodology cannot deliver actionable insights for modern radial‑tyre assessment.
2. The shift towards radial‑tyre construction is irreversible. Removing prescriptive sidewall‑strength mandates unlocks design freedom for tyre dynamic performance, enabling improvements in vehicle handling and low‑emission capability. This represents an advanced tier of automotive safety, realising lightweighting and energy‑saving potential that would otherwise be constrained by rigid strength‑test requirements.
3. When handling consumer complaints about bulging sidewalls on low‑aspect‑ratio UHP/UUHP high‑performance radial tyres, stakeholders must recognise the trade‑offs inherent to radial‑tyre dual‑component architecture: superior dynamic performance comes alongside inherent sidewall‑impact‑vulnerability. Vehicle OEMs need to fully understand the operational characteristics of low‑aspect‑ratio high‑performance tyres, and communicate clearly to end‑users. Consumers should be made aware to avoid abusive curb‑strike events while benefitting from high‑performance‑tyre capabilities. Test data demonstrates that raising obstacle height from 80 mm to 100 mm can reduce the tyre‑damage‑onset safe‑impact speed by as much as 43 percent.
Advancing passenger car radial tyre and high-performance tyre technology to achieve lightweight and sustainable performance is the industry’s forward-looking development priority. This study clarifies the historical context of tyre strength evaluation practice; it supplies technical background to support proposal on revision of relative Indian IS standard and delivers practical guidance for consumers operating high‑performance tyres as well as for vehicle‑OEM tyre‑specification engineers.
The author is the Head Of APAC Standards And Regulations, Continental Tires.
Comments (0)
ADD COMMENT