Purify, Regenerate, Reuse: Returning Every Drop Of Waste Oil Back To Production
- By TT News
- September 07, 2026
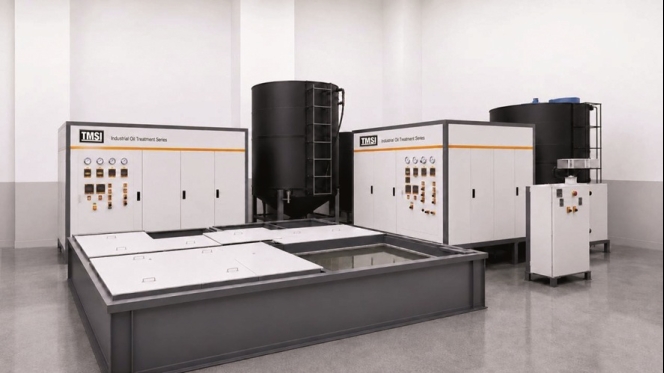
Industrial waste oil has traditionally been treated as a maintenance expense and a hazardous waste stream in tyre manufacturing. But advances in oil purification and regeneration technologies are offering manufacturers a way to recover and reuse contaminated oils instead of replacing them. By extending oil life and reducing waste, these systems can help lower operating costs, improve equipment reliability and support sustainability goals. This article examines how TMSI’s oil purification solutions are enabling tyre manufacturers to adopt a more circular approach to industrial oil management.
INDUSTRIAL WASTE OIL: STEADILY ERODING OPERATING PROFITS
In mixing room, rotor seal oil is chronically contaminated by carbon black, oxidation products, metal wear debris and mechanical impurities. During the vulcanisation process, hydraulic oil frequently suffers from contamination and system malfunctions caused by the ingress of moisture and particulates, as well as the formation of sludge and varnish. When oil shifts from a protective medium for equipment to a source of operational risk, profits are continuously – and often invisibly – drained away.
For a typical tyre factory, oil-related expenditures can reach millions of dollars annually. However, industrial waste oil should not be viewed merely as hazardous waste awaiting disposal. Through TMSI’s advanced oil purification and regeneration technologies, contaminated oil can be purified, regenerated and reintroduced into the production cycle – transforming it from a one-time consumable into a recyclable production resource that delivers quantifiable, sustainable value.
MIXER SEAL OIL REGENERATION: 90% OFF-LINE RECYCLING
Seal oil in internal mixer rotors suffers from severe contamination and rapid consumption. Traditional filtration methods struggle to simultaneously address oxides, acidic substances, mechanical impurities and micro-contaminants. Centred on patented electro-sorption and micron-level precision filtration technologies, the TMSI regeneration system selectively captures polar contaminants. It transforms waste oil into reusable, regenerated oil while maximising the retention of the base oil’s active components.
The system enables 90 percent off-line recycling of waste oil, with a processing capacity of 1.5 tonnes per 8-hour batch. Calculations for a typical project – such as a tyre manufacturer generating 240 tonnes of waste seal oil annually – show potential comprehensive annual savings of approximately USD 280,000 and a payback period of less than one year. Furthermore, the use of clean oil minimises scratching on sealing surfaces, prevents sticking caused by gum deposits and reduces wear on critical components, thereby lowering the risks of leakage, downtime and quality fluctuations.
HYDRAULIC OIL PURIFICATION: NO SHUTDOWN, NO OIL CHANGE, 100% CLOSED-LOOP ONLINE PURIFICATION
The core value of hydraulic oil purification is not only to extend the life of the oil but also to prevent maintenance from interrupting production. The TMSI hydraulic oil online circulation purification system is connected to the hydraulic station in a bypass mode and continuously removes moisture, particulate matter, sludge, paint film and oxidised pollutants during equipment operation, allowing the hydraulic oil to recover its performance in a closed-loop cycle, instead of waiting until the oil is out of control before shutting down for oil changes.
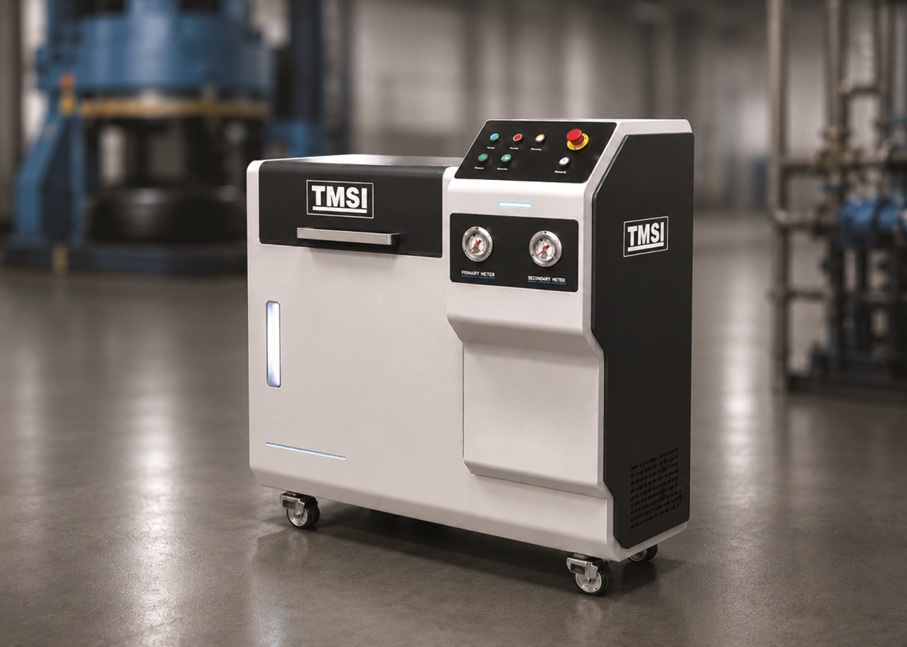
The system flow rate covers 30 L/h to 150 L/h, adapting to different tank volumes; after purification, the moisture can be reduced to less than 0.03 percent, and the cleanliness is better than NAS level 8 and can be further improved to approximately NAS level 7 in actual applications. Under normal circumstances, the hydraulic oil change interval is about 1–2 years; when contamination increases, it may be shortened to 3–6 months. Online purification not only reduces the purchase of new oil and the disposal of hazardous waste but also helps reduce the risk of valve core sticking, lagging action, hydraulic cylinder corrosion and internal leakage, ensures the stability of the mould closing force of the vulcanising machine and the consistency of the vulcanisation quality and allows equipment management to shift from post-repair to pre-protection.
PATENTED COMPOSITE FILTER ELEMENT: ENHANCING THE PURIFICATION CAPABILITIES OF EXISTING SYSTEMS
For hydraulic systems already in operation, the TMSI patented composite filter element offers a streamlined, rapid upgrade path. Designed to fit existing system interfaces, it enables an immediate boost in fluid purification performance – enhancing the equipment’s ability to remove water and impurities while improving acid values – simply through a direct replacement of the filter element.
Leveraging material modification and structural optimisation, the composite filter element achieves multi-stage purification within a single unit. It offers filtration precision ranging from 0.5 to 30 μm and consistently maintains oil moisture levels below 300 ppm through recirculating purification. Its high dirt-holding and water-absorbing structure extends service life; under standard operating conditions, the replacement interval reaches six months or longer, allowing existing equipment to achieve superior, long-lasting fluid management capabilities with minimal investment.
FROM HAZARDOUS WASTE COST TO CIRCULAR ASSET: REDEFINING THE VALUE OF INDUSTRIAL OIL
From North America to Latin America and from Asia to Europe, TMSI’s oil purification solutions are consistently proving stability, adaptability and long-term operational value for more and more manufacturers.
TMSI is transforming industrial oil consumption from the traditional ‘consume-replace-dispose’ model to a circular ‘purify-regenerate-reuse’ model, an approach successfully implemented in the tyre industry.
When waste oil ceases to be merely a cost item on a hazardous waste list and instead becomes a circular asset – capable of being purified, re-evaluated and reintroduced into the production system – fluid management shifts from a routine maintenance task to a strategic factor directly impacting consumable costs, downtime losses, investment payback periods and ESG performance. Returning waste oil to the production line represents more than just an upgrade in oil purification; it paves a new path for tyre factories towards lean, low-carbon and highly resilient operations.
Kumho Petrochemical Group Shifts Focus To R&D and Speciality Materials
- By TT News
- September 25, 2026
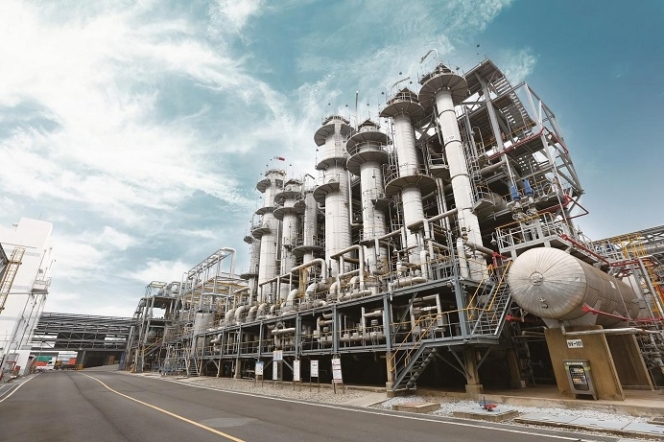
Kumho Petrochemical Group is steering its business towards research-driven, higher-value outputs as oversupply and soft demand continue to weigh on the worldwide petrochemical sector. The Seoul-based group outlined plans to boost spending on speciality chemicals, sustainable materials and novel production methods, a push intended to lift profits while building a foundation for future expansion.
Underlying the move is a deliberate evolution in the group's identity, from a bulk materials vendor to a provider of technology-backed solutions that address shifting customer requirements and stricter environmental rules. A central element of that effort involves widening the speciality lineup, exemplified by added capacity for solution styrene butadiene rubber, a synthetic rubber that enhances durability, rolling resistance and tread wear in high-performance electric vehicle tyres.
Environmental initiatives form another pillar. Facilities built by the company can trap approximately 76,000 metric tonnes of carbon dioxide each year, while separately developed technology turns recycled acrylonitrile butadiene styrene sourced from scrapped household appliances into automotive-grade interior components that satisfy performance standards and generate fewer emissions than conventional methods. The group has also joined forces with POSCO Future M and BEI on anode-free lithium-metal battery development.
Parallel technology-focused programmes are underway at affiliated units. Kumho P&B Chemicals is formulating water-based epoxy resins that curb volatile organic compound releases while incorporating more bio-based inputs to reduce carbon intensity. Kumho Mitsui Chemicals is advancing bio-based polyurethane systems and electric vehicle materials, alongside debottlenecking work to add 100,000 tonnes of annual methylene diphenyl diisocyanate capacity. Kumho Polychem, meanwhile, is targeting ethylene propylene diene monomer through low-temperature polymerisation paired with energy-efficiency improvements.
Birla Carbon Announces Asia-Wide Speciality Materials Price Hike Of Up To 15%
- By TT News
- September 22, 2026
Birla Carbon has confirmed a price increase of up to 15 percent for its Speciality Materials products across Asia, scheduled to take effect on 1 October 2026. The company pointed to significant and sustained rises in feedstock costs, driven partly by ongoing geopolitical instability and disruptions in global feedstock markets, as the reason behind the adjustment.
Although Birla Carbon pursued operational efficiencies, supply chain optimisation and disciplined cost management to soften the impact, the scale and persistence of the cost escalation left a price adjustment unavoidable. The company's sales teams will engage customers directly to explain the details and help them navigate the transition.
ACE Laboratories, Abdallah Consulting Launch VericarbSM To Standardise Recovered Carbon Black
- By TT News
- September 20, 2026
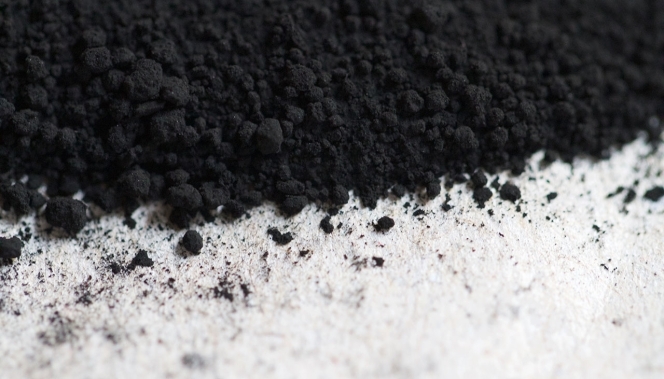
ACE Laboratories, an independent ISO/IEC 17025-accredited polymer testing laboratory, has partnered with Abdallah Consulting, LLC, a prominent tyre pyrolysis advisory firm, to introduce VericarbSM. This independent certification programme verifies that materials marketed as recovered carbon black (rCB) meet established criteria for rCB.
Recovered carbon black, derived from end-of-life tyres via pyrolysis, serves as a sustainable substitute for virgin carbon black in rubber and polymer applications. However, the emerging market has lacked the standardisation and independent verification that established supply chains provide. VericarbSM addresses this gap through independent material characterisation and rubber performance data, offering stakeholders a consistent basis for evaluating rCB products.
For producers, certification accelerates market entry and improves buyer approval rates. Consumers gain more capable suppliers and reduced evaluation time, while investors benefit from clearer volume sizing and fewer costly test failures. The programme is jointly administered by both organisations.
Erick Sharp, CEO, ACE Laboratories, said, “The rCB market has enormous potential, but growth has been held back by uncertainty about material quality and consistency. VericarbSM gives producers a way to prove their product and gives buyers the independent data they need to say yes.”
Dave Abdallah, Founder, Abdallah Consulting, said, “One key reason for the delayed growth of recovered carbon black is lack of product performance information in the customer’s language. ASTM standards are critical; in fact, most testing done in the process follows ASTM methods. But customers relate to a product better when its performance is shown in applications relevant to them. VericarbSM solves the language issue by showing verified rCB in terms of rubber performance while simultaneously adding credibility via third-party analysis and reporting.”
Zeon Establishes Kurashiki Subsidiary To Absorb Tohpe's Acrylic Rubber Business
- By TT News
- September 18, 2026
Zeon Corporation established Zeon Chemicals Kurashiki Co., Ltd. on 23 July 2026 to take over the acrylic rubber operations of fellow group firm Tohpe Corporation. The new entity, headquartered in Kurashiki City, Okayama Prefecture, is wholly owned by Zeon with paid-in capital of JPY 10 million and is led by representative Koji Minami.
On 21 August, Tohpe and the new subsidiary signed an absorption-type company split agreement, prompting Zeon to begin the procedures required under the Companies Act. Operations at the new company, focused on manufacturing and selling acrylic rubber and related activities, are scheduled to commence on 30 October 2026.
Acrylic rubber, known for its heat resistance, is used in automotive components including oil seals and hoses. The Zeon Group already maintains four production sites across Japan, United States and Thailand, forming a global supply network for the material.
The restructuring follows Zeon’s 11 May 2026 announcement that it would transfer Tohpe shares to NATOCO Co., Ltd. of Miyoshi City, Aichi Prefecture, as part of Tohpe’s paints business divestiture. Tohpe’s acrylic rubber operations, which complement Zeon’s Elastomers Business, will now be positioned as a key specialty rubber manufacturing site, with closer operational coordination intended to strengthen Group competitiveness and corporate value.
Comments (0)
ADD COMMENT