What kind of products does Uzer Makina offer to global tyre industry?
Uzer Makina has been serving top tyre makers all around the world with its tyre curing presses and molds since 1978. Our press product category consists of mechanical and hydraulic presses for all kinds of tyres; while mold category includes tread segments, sidewall plates, container mechanisms, AG molds and bladder molds.
 Tell us about the evolution of the company as a global leader
The company was founded by Selahattin Uzuner and his nephew Bahattin Ertuğ. At first, the company was working for petrochemical industry in Turkey and later on started to make mold maintenance activities for various tyre companies in Kocaeli. First mold was manufactured 1984. Nearly 10 years later, Uzer Makina started to manufacture tyre curing presses again for plants in İzmit. In 2000, the plant was moved to Kartepe, Kocaeli, where it is currently located. In 2004, first hydraulic tyre curing press is manufactured and in 2007 Uzer Makina designed, manufactured and internationally patented its popular product Floating Column Hydraulic Press. Until late 2000s, the company mostly served domestic market. After 2010, we started to supply a good amount of its products abroad as well. With an aggressive growth strategy, Uzer Makina invested in buildings, brand-new equipment, human resources and expanded production in last five years to become a global player in tyre curing equipment market. We now serve top tyre makers and their plants in more than 40 countries.
What is the latest step in your expansion process?
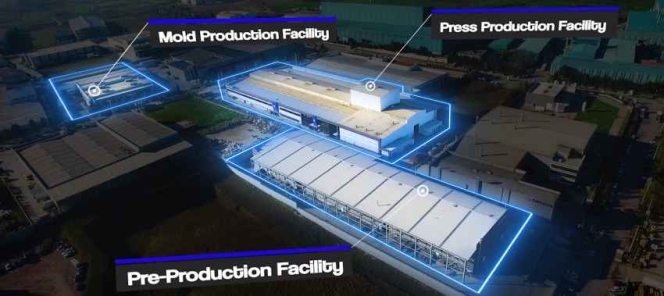
After doubling capacity in 2018 by separating press and mold factory, Uzer Makina has completed another expansion by June 2020. This new facility is entirely dedicated for pre-production activities, including storing steel raw materials, cutting, bending, construction, welding, sandblasting and heat treatment serving both for tyre curing press and mold categories which used to be a part of press manufacturing facility before. Uzer Makina also moved its HQ office from mold factory to press factory.
Investment decision was made at the end of 2019 by the top management before Covid-19 pandemic with the goal of decreasing the costs by decreasing the amount of manufacturing activities which are outsourced. Following this decision, Uzer Makina has acquired 9500 m² land just next to existing press manufacturing facility and finished 6500 m² building in less than 7 months.
Uzer Makina also has added brand-new pre-production equipment like heat treatment furnace, sandblasting machine and bending machine. With these new machinery investment, Uzer Makina is planning to decrease the cost per product and production time while increasing the total quality of the processes by taking these operations in house rather than outsourcing them.
This expansion enables Uzer Makina to better use the existing press manufacturing facility. Since pre-production occupied a good amount of space before leaving the building, remaining place is now used for press manufacturing and assembly. Therefore, Uzer Makina is able to manufacture more presses at the same time compared to previous set-up. Uzer Makina has also made machinery investments for existing press area as well including automated spray-painting booth for painting press bodies/parts and vertical turning machine with 3 meters turning diameter which would mainly be used for parts of bigger (over 85”) mechanical presses.

What are the features of the new SUV & TBR Floating Column Hydraulic Press?
A new era for SUV & TBR tyre curing has begun as Uzer Makina announced the development of SUV & TBR version of its most popular and internationally patented Floating Column Type Hydraulic Press in the last Tyre Technology Expo. Uzer Makina dispatched the first 65” Floating Column Hydraulic Type Curing Press at the end of 2020. This new version outweighs the existing solution Frame Type which used to be the industry standard almost in every aspect. It offers a simpler design, the construction weights much less, has fewer components, maintenance requirements are lower and finally the energy requirement is lesser compared to Frame Type. Besides, most importantly, pricewise there is no significant difference between these two types.
 On the other hand, tyre manufacturers will be able to benefit all the advantages of the internationally patented Floating Column Technology for curing of larger tyres. Floating Column Technology provides fully automatic mold height adjustment and therefore eliminates the need for conventional mold height adjustment systems. The technology features two squeezing cylinders under the columns on both sides of each cavity. The piston rods of these cylinders are directly connected to the columns. Besides applying squeezing force, these cylinders also change the position of the locking point, which is located on the columns for adjustment of mold height. Therefore, the press does not need multiple locking points and can work perfectly well with just one. Columns rise at the end of each cycle and release the locking plates from grooves, meaning the locking mechanism can work without jamming.
In addition to these, Uzer Makina is able to construct this new size Floating Column Type Hydraulic Press as V-Shape as well in order to save space. The V-Shape design enables tyre manufacturers to use the curing press area at least 12% more efficiently, in other words, tyre producers would be able to place 112 curing presses in an area that was previously large enough for 100 machines. This concept was developed by Uzer Makina engineers in response to the recent market demand for upgrading existing machines in tyre production plants.
On the other hand, Uzer Makina have been recently putting so much effort to increase energy efficiency on the presses and therefore help tyre manufacturers to comply with the latest European regulations. With this object in mind, Uzer Makina has developed “Energy Saver Steam Hoses” as a subsidiary product that would work both with Uzer Makina presses and others. With these hoses, one can save up to 5% energy per press which is equal huge amount of energy considering the fact that tyre curing is the most energy consumer process of tyre production. These hoses also prevent curing area from overheating. In case there is an effort to cool down the area, there is no need for it or at least it requires much less effort to keep the curing area at normal temperature.
 Uzer Makina is not solely a tyre curing press and mold producer – the company also strives to improve the efficiency of the entire curing process. Uzer Makina places great emphasis on digitization and designs its presses to be fully compatible with Industry 4.0 requirements such as EMS, AGV, SCADA, MES and ERP systems. In addition, the company conducts its own research and also works with leading industry companies to offer solutions such as mold pre-heating presses, mold changing pickup cranes and RFID mold management systems – to help tyre manufacturers achieve the most efficient curing processes.
How did the company take on the pandemic?
Even though pandemic conditions were very challenging for tyre industry especially in terms of demand last year, 2021 is very promising also for Uzer Makina. There are many reasons for this: firstly, because of US tariffs against Asian tyre makers, Turkey & Eastern Europe has become a very attractive country for capacity increase for tyre production. Almost all tyre makers in Turkey runs at full capacity and some of them already is expanding. Secondly, there has been a global change in transportation as many people now prefers to move more individually than ever, this probably will eventually affect the number of tyres produced globally. Uzer Makina started to feel this rebound in the demand as many existing customers has decided to restart their previously on hold orders and requesting inquiries for new equipment, and it is also a known fact that quite a few tyre makers are making new greenfield & expansion projects. As Uzer Makina continues to improve its reputation in the market year by year, this rebound will have much more positive effect on the company.
In the pandemic period, like all other companies, Uzer Makina also had to transform the way to operate business into more digital. Now in Uzer Makina, all internal meetings are video meetings. Since travelling abroad is still an issue, nearly all the meetings with customers and suppliers are done via video calls too. Uzer Makina enriched the content of the installation and commissioning materials and provided remote support in order to help the customers which cannot accept people to their plants because of travelling bans. (TT)

- AZuR Chemical Recycling Project Group
- AZuR Network
- End-Of-Life Tyres
- Tyre Pyrolysis
- Recovered Carbon Black
- Tyre Pyrolysis Oil
- Pyrolysis Gas
New Research Quantifies Environmental Benefits Of End-Of-Life Tyre Pyrolysis
- By TT News
- October 15, 2026
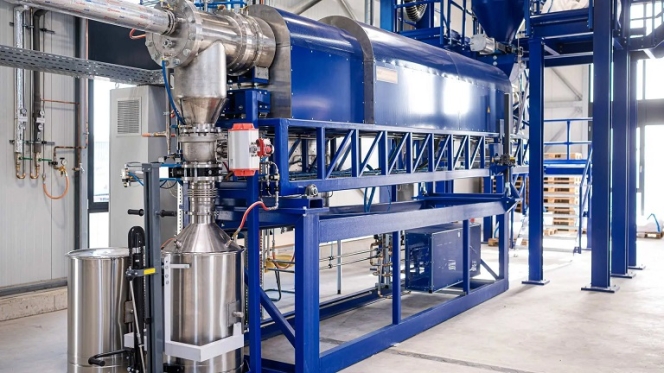
New research findings from a doctoral dissertation by Dr.-Ing. Sebastian Bogdahn examine how end-of-life tyres can yield high-quality recovered carbon black (rCB) through pyrolysis while delivering substantial environmental benefits. The work, titled ‘Production and Environmental Assessment of High-Quality Carbonaceous Materials from End-of-Life Tyre Pyrolysis’, was presented in condensed form at an AZuR Chemical Recycling Project Group meeting in Dillingen/Saar on 1 October 2026.
The dissertation tackles how end-of-life tyres can be recovered and recycled to maximise their value. Pyrolysis is identified as a complementary technology that helps close recycling gaps in the circular economy and offers an alternative to fossil-based carbon black, a material that plays a crucial role in determining tyre properties.
In the pyrolysis process, rubber granules from processed tyres undergo thermal decomposition without oxygen, producing three main streams: solid rCB, tyre pyrolysis oil and pyrolysis gas. Previous evaluations of such technologies often separated technical and environmental perspectives, relied on secondary data and lacked standardised methodologies, making findings difficult to compare.
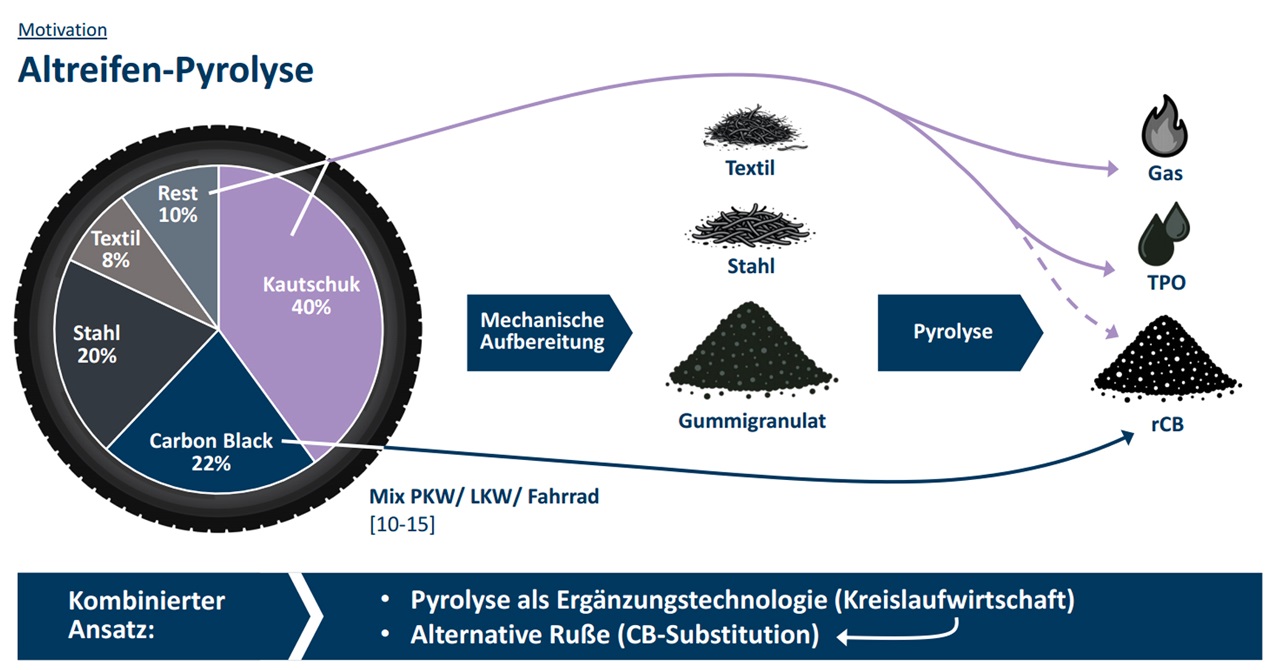
Image credit: Dr.-Ing. Sebastian Bogdahn
Bogdahn overcomes these limitations by integrating a technology-specific process model with a detailed life cycle assessment model. This combination enables a scientifically robust environmental evaluation of pyrolysis and its secondary raw materials using reliable primary data. A central component is a process model that mathematically describes material conversion by combining reaction kinetics, reactor behaviour and mass and energy balances.
Starting with laboratory-scale experiments, the model was scaled up and validated using a pilot-scale rotary kiln at the Institute of TH Köln. Comprehensive laboratory analyses of feedstocks and products supported development and validation. Optimal conditions for the investigated system were found at 650 degrees Celsius with a residence time of about one hour, achieving complete material conversion and high-quality recovered carbon black. Product distribution was roughly 40 percent rCB, 37 percent TPO and 23 percent pyrolysis gas by weight.
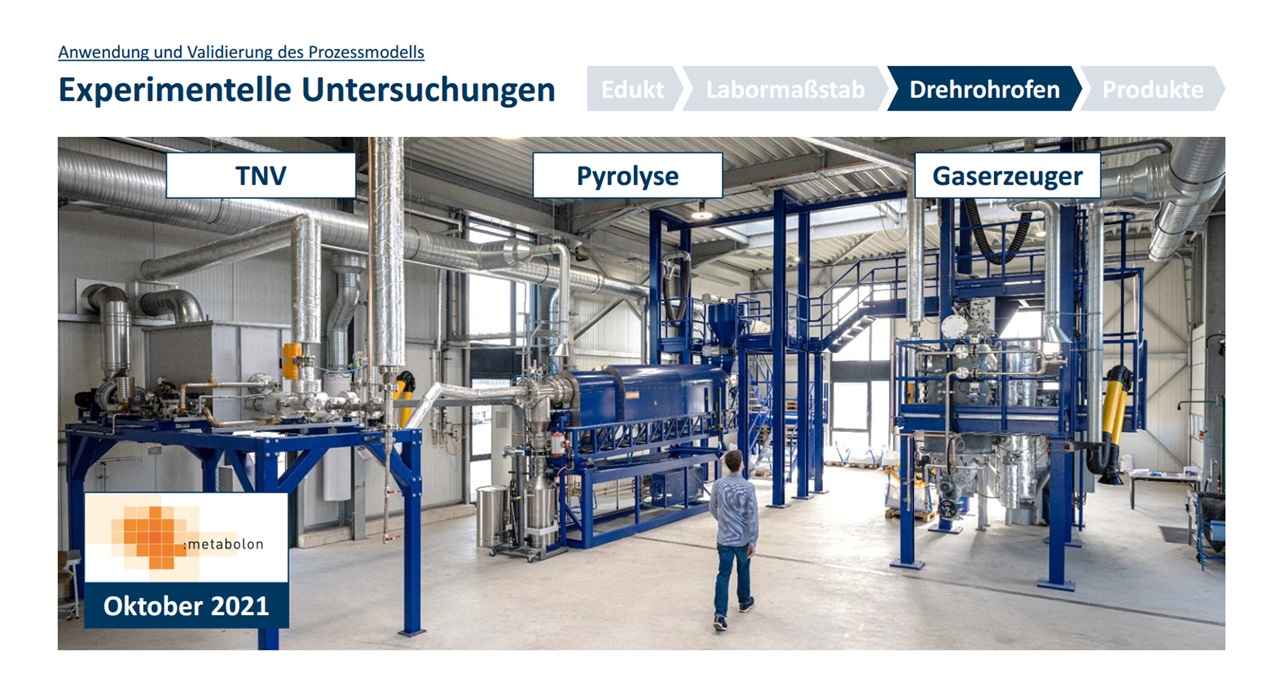
Image credit: Dr.-Ing. Sebastian Bogdahn
Using validated primary data, Bogdahn conducted a comprehensive environmental assessment and developed a methodological matrix covering relevant standards and guidelines to address inconsistent approaches. In the rotary kiln baseline scenario, one metric tonne of recovered carbon black results in a global warming potential over 100 years of about 918 kilogrammes of carbon dioxide equivalents, compared with the International Carbon Black Association’s global industry average of 3,910 kilogrammes for conventional fossil-based carbon black, a reduction of approximately 77 percent. Even after a quality adjustment for lower carbon content, the reduction remains about 70 percent. The study followed ISO 14067 and underwent independent external critical review under ISO 14071, also covering TPO and sustainable carbon black.
Further improvements remain possible. Emissions mainly stem from electricity consumption and gas combustion, with rCB processing accounting for about 44 percent, pyrolysis gas cleaning and combustion about 36 percent and tyre shredding about 19 percent. Sensitivity analysis confirms that renewable electricity offers substantial additional greenhouse gas reductions, reinforcing that a circular economy achieves genuine sustainability only when powered by renewable energy. Enhancing material quality through demineralisation and activation could enable higher substitution rates for fossil-based carbon black.
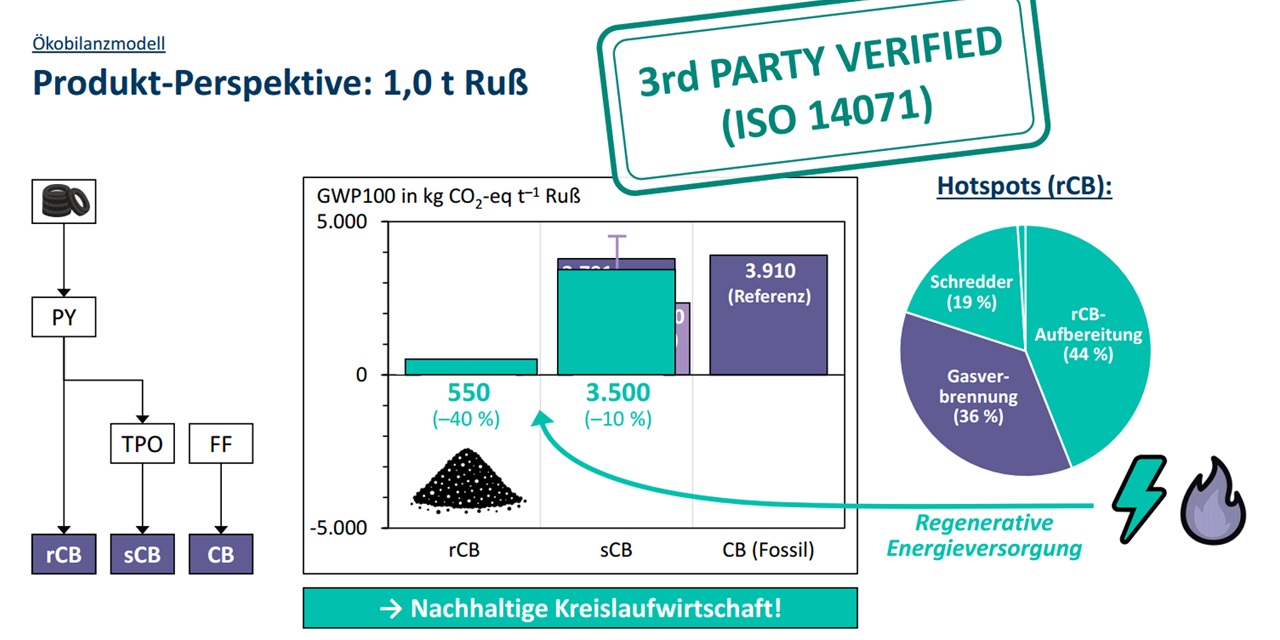
Image credit: Dr.-Ing. Sebastian Bogdahn
A central conclusion extends beyond pyrolysis itself. Raw materials, tyre manufacturing, the use phase and recovery pathways form an interconnected system spanning the entire tyre life cycle, closely linked to the carbon black, chemical, steel and energy sectors. Achieving circularity requires collaboration across systems and industries, along with greater methodological harmonisation and stronger integration of industrial value chains. The AZuR network’s work reflects this need, recognising that extended tyre use, repair, regrooving, retreading, mechanical recycling and appropriate chemical recycling must all function as interconnected elements of the value chain.
Tyres Europe Backs CARUSO Findings As EU Data Act Marks One Year
- By TT News
- October 15, 2026
Tyres Europe, as part of a coalition of 10 European associations representing consumers and automotive and mobility service providers, has issued a joint press release welcoming the latest CARUSO Connected Vehicle Field Test assessing the EU Data Act’s implementation across 29 major vehicle manufacturer groups. The findings confirm the legislation established important principles for accessing vehicle-generated data and encouraged some manufacturers to engage for the first time. One year on, however, the framework remains insufficient alone to enable a competitive, innovative connected mobility market.
Covering 15 automotive use cases across 28 vehicle manufacturer groups, the study concludes that while data access has improved, conditions for competitive, scalable, multi-brand services are still lacking. Access remains fragmented, inconsistent and often commercially or technically impractical across the car parc. Limited third-party access, differences in data scope, quality and coverage, and restrictive commercial terms continue to undermine the business case for innovative services. Genuine multi-brand development remains unattainable, preventing consumers and businesses from fully benefiting from connected mobility.
For many manufacturers, implementation has become a compliance exercise rather than a genuine effort to enable market access. Independent providers face limited datasets, restrictive terms, manual approvals, manufacturer-specific consent mechanisms and inconsistent technical solutions. Such approaches may satisfy the Data Act’s broadly defined obligations but are incompatible with the real-time, automated access modern digital services require.
Strong enforcement matters. Manufacturers respond faster where national authorities investigate complaints and apply enforcement mechanisms. Without consistent, harmonised, proactive enforcement across the European Union, Data Act rights risk remaining largely theoretical for a significant share of Europe’s vehicle fleet.
The coalition urges European Union institutions and Member States to enforce the Data Act consistently, issue clear guidance on fair, reasonable and cost-based compensation and use forthcoming reviews to reinforce rather than weaken it. Dedicated automotive legislation should establish common access conditions, interoperability requirements, initial technical and data delivery standards and safeguards against discrimination. Effective access must cover vehicle-generated data and the in-vehicle functions and resources needed to develop, scale and deliver digital mobility services, enabling fair competition, growth and investment.
According to the coalition, the Data Act was an important first step, but horizontal legislation alone cannot create a workable multi-brand market. Implementation varies widely: of 28 manufacturers, nine (32 percent) have barely implemented the Act; 18 (64 percent) lack adequate third-party pricing; 18 (64 percent) lack adequate data provision; and 19 (68 percent) lack an adequate API solution. Sixteen manufacturers (57 percent) enable none of the use cases, while only nine support the most feasible ones. Without stronger enforcement and dedicated automotive legislation, Europe will fall short of its innovation, consumer choice and fair competition ambitions.
CEAT Q2 FY27 Revenue Rises 26% to INR 47.62 Bln
- By TT News
- October 14, 2026
CEAT reported a 26 percent year-on-year increase in consolidated revenue to INR 47.62 billion in the second quarter of the 2026-27 financial year, while net profit stood at INR 1.12 billion as higher raw material costs continued to weigh on the tyre maker.
The company’s consolidated earnings before interest, tax, depreciation and amortisation (EBITDA) margin was 9.5 percent, according to its unaudited results for the quarter ended 30 September.
Arnab Banerjee, Managing Director and Chief Executive, said revenue growth was supported by premium segments across business units. He added that the conflict in West Asia had kept raw material costs high, prompting the company to tighten cost controls.
CEAT expects to deliver double-digit revenue growth in the second half of the financial year, alongside further price increases, Banerjee said.
On a standalone basis, revenue rose 23 percent year on year to INR 45.48 billion. EBITDA margin was 10.14 percent, while net profit reached INR 1.64 billion.
Kumar Subbiah, Chief Financial Officer, said commodity costs were expected to remain elevated in the third quarter. The company would continue to pursue measured price increases and improve its product mix to manage cost pressures.
Subbiah said debt increased during the quarter, largely because of capital expenditure of close to INR 4.9 billion to expand capacity in areas with high utilisation, as well as dividend payments.
He added that CEAT would maintain financial discipline while investing to meet demand and support profitable growth.
Michelin Expands Delhi Presence With Dwarka And Karol Bagh Outlets
- By TT News
- October 14, 2026
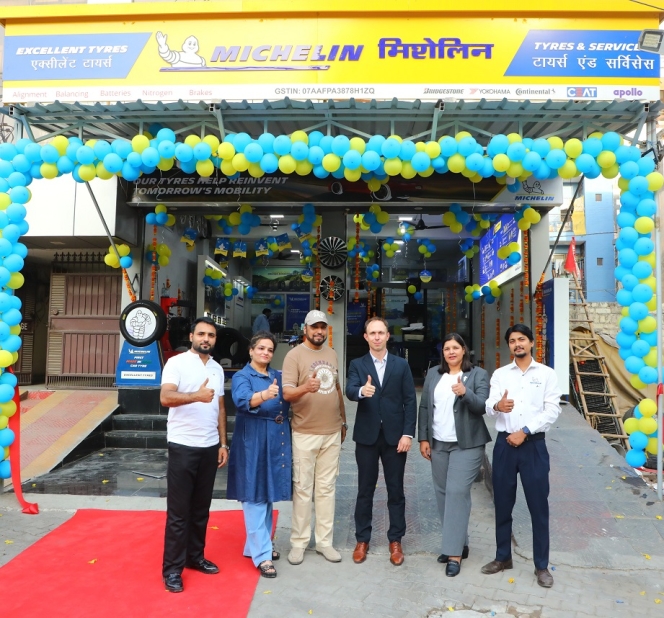
Michelin has strengthened its retail presence in India by launching two Michelin Tyres & Services outlets in Delhi, located in Dwarka and Karol Bagh. The openings make Michelin's premium tyre range, including the Made-in-India Primacy 5, accessible to customers in west and central Delhi, alongside professional fitment and tyre care. The Dwarka facility was inaugurated by Benjamin Coesnon, Marketing Director India.
The Dwarka outlet, operated with Excellent Tyres, covers 1,500 sft and caters to one of Delhi's largest planned residential sub-cities and its expanding south-west corridor. Excellent Tyres, established in 1994, brings over 30 years of experience in the capital's tyre trade. Meanwhile, the Karol Bagh store, run with Rana Tyres, spans 1,000 sft in a prominent automotive trade hub. Founded in 1977 and now led by its third generation, Rana Tyres contributes nearly five decades of technical knowledge and a loyal clientele.
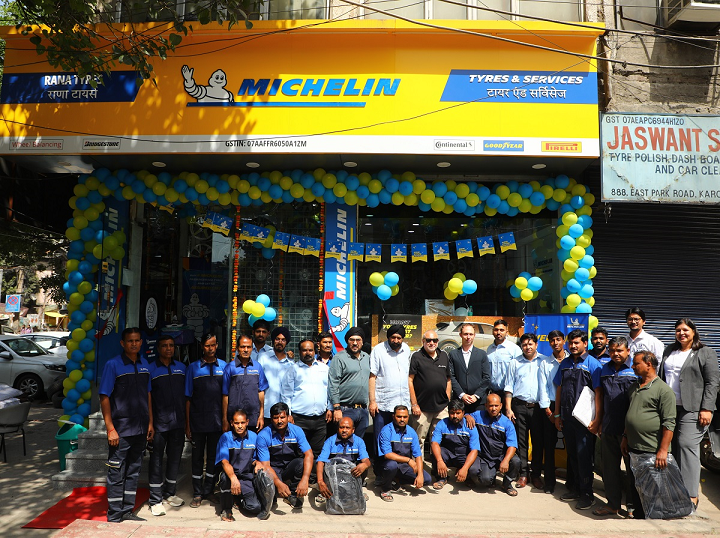
The expansion reflects Michelin's sustained commitment to India. Its distribution network now exceeds 800 points of sale, while over INR 28 billion has been invested in the Chennai manufacturing plant. A further INR 6.86 billion went into a passenger car tyre line that now produces the Primacy 5 for Indian buyers. The new stores aim to deliver safer, more durable and higher-performing mobility.
Shantanu Deshpande, Managing Director, Michelin India, said, " Delhi is one of the largest premium car markets in the country. Expanding our presence in Delhi will provide accessibility to today's customers and serve the next wave of premium car owners. With the Made-in-India Primacy 5 now available at these stores, customers in the capital can get Michelin's globally benchmarked safety and longevity, backed by expert service from trusted partners. India remains a key growth market for Michelin, and Delhi is central to how we continue to build our presence."
Comments (0)
ADD COMMENT