The Last Man Standing: How A Perth Startup Became The Mining Industry’s Tyre Whisperer
- By Sharad Matade
- August 13, 2025

Vehicle Management Corporation survived industry consolidation to dominate a USD 1.5 billion niche managing mining’s most expensive consumables.
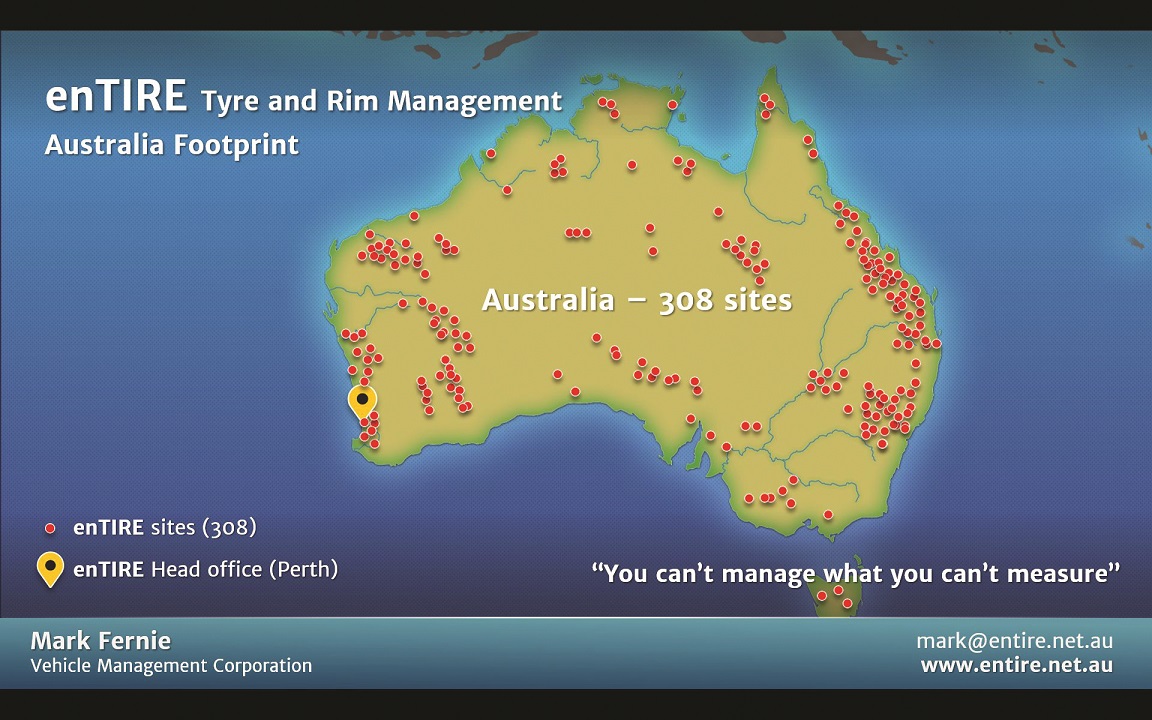
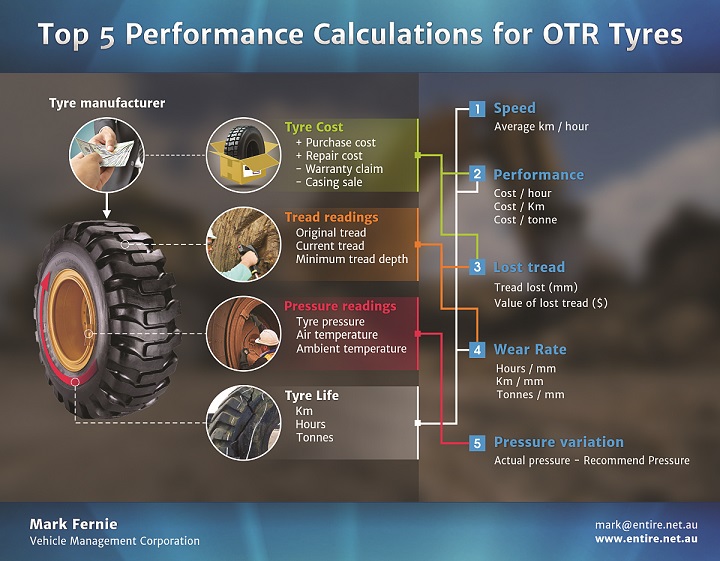
More than 30 years after its modest beginnings, Fernie’s Vehicle Management Corporation (VMC) now leads the global independent tyre management software sector. The company oversees USD 1.5 billion in tyre and rim assets across 480 mining sites on multiple continents. With individual mining tyres costing upward of USD 50,000, VMC’s enTIRE software has become critical for operators aiming to maximise the value of their most expensive consumables.
“We don’t sell tyres or offer tyre services – software is our sole focus,” Fernie said. This specialisation has been VMC’s core competitive strength and a key reason it outlasted larger, better-funded competitors during two decades of industry consolidation.
VMC’s journey from a single-client DOS application to managing billions of dollars in assets demonstrates how even small software firms can thrive by addressing highly specialised industry needs that larger solutions often overlook.
THE CONSOLIDATION SURVIVOR
VMC’s fierce independence stands out in a tyre industry where consolidation is accelerating. While giants like Bridgestone and Michelin snapped up rivals – Otraco and Klinge, respectively – VMC has held the line, rebuffing takeover interest and prioritising customer relationships over shareholder pressure or supplier alliances.
“With Bridgestone acquiring Otraco and Michelin purchasing Klinge, VMC became the only independent, commercially viable tyre management software provider remaining,” Fernie explained. “Developing a competitive independent system today would require USD 5+ million in funding and years of field testing, making our market position difficult to replicate and any alternatives difficult to justify.”
This independence is now central to VMC’s appeal for multinational miners working with multiple suppliers. Unlike manufacturer-backed software, VMC’s enTIRE system is completely agnostic, allowing clients to base their purchasing decisions solely on performance data and cost-effectiveness.
That strategy has earned VMC unusually durable client ties. Its three-decade partnership with Freeport Indonesia – one of the world’s largest mining operations –underscores the appeal of a model that favours operational flexibility over vendor lock-in, a growing concern among customers wary of manufacturer-driven ecosystems.
“Most of our clients are long-term,” Fernie noted, emphasising how this stability has become increasingly valuable as mining companies seek to avoid the disruption and data loss that often accompanies vendor changes in manufacturer-controlled systems.
BEYOND COST CUTTING: SAFETY AND ENVIRONMENTAL IMPACT
While cost reductions – often 10 percent to 30 percent within three years – drive initial adoption, VMC’s impact extends far beyond savings. In nonstop mining environments, where tyre failures can lead to life-threatening accidents, safety and uptime are equally vital.
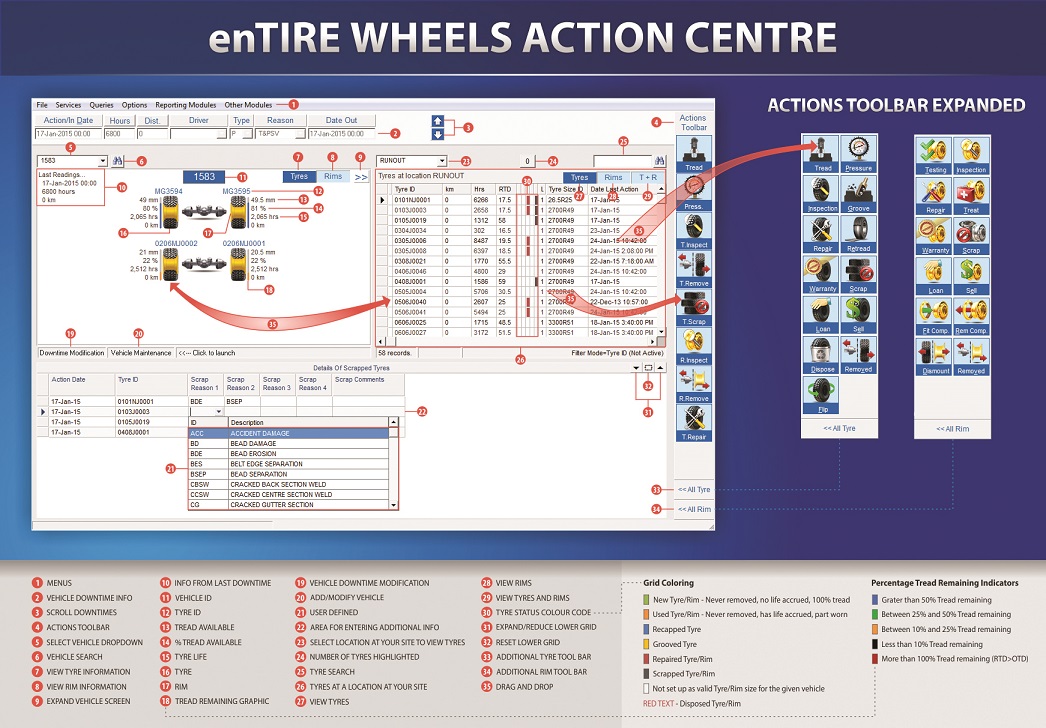
“Operating tyres outside pressure or load specs increases blowout risks,” Fernie said, emphasising safety. enTIRE tracks rim certifications and keeps failure histories, supporting safety protocols. “Rim accidents are very dangerous, potentially fatal.”
Environmental benefits have also emerged as an increasingly important value proposition for mining companies under growing pressure to reduce their carbon footprints and waste generation. By extending tyre life and dramatically reducing premature failures, mining operations generate substantially less waste while simultaneously improving fuel efficiency through optimised tyre pressure monitoring systems.
“Optimising pressure with TPMS can extend tyre life by 20–30 percent, reduce rolling resistance and lower fuel consumption by up to three percent – a substantial saving in mining operations,” Fernie explained. In an industry where fuel costs represent significant operational expenses and environmental regulations continue to tighten, these seemingly modest percentage improvements compound into substantial savings and meaningful reductions in environmental impact.
The environmental mathematics are compelling: operators can achieve approximately 30 percent increases in tyre life through proper lifecycle management, directly reducing landfill waste, shipping requirements and manufacturing demands – collectively helping reduce the carbon footprint of tyre procurement and disposal across the mining sector.
THE TECHNOLOGY EVOLUTION
VMC’s technological evolution, from humble beginnings as a basic DOS program to advanced, cloud-based solutions, reflects the broader digitisation revolution in factory operations that began in the early 1990s. The firm’s flagship enTIRE software began as a Windows product with what Fernie recounts with clear pride as a ‘pioneering drag-and-drop interface’ in the early 1990s – a cutting-edge user experience design that was decades ahead of its time.
The platform has progressed steadily through several generations of technology, transitioning from Microsoft Access databases to high-performance SQL Server implementations, which have significantly improved performance and scalability. It introduced full multi-site support features in 2001 and incrementally incorporated tyre pressure monitoring systems (TPMS) from seven sensor vendors starting in 2007. The software industry award was presented in 2005, when the system was named the Financial Review Australian Information Industry Association’s ‘Best Industrial Software Application’.
Recent development efforts focus heavily on artificial intelligence integration for enhanced analytics capabilities and predictive maintenance functionalities. “We’re actively using AI to streamline development and support,” Fernie said, outlining the company’s forward-looking technology strategy. “We expect AI will significantly enhance predictive analytics, client dashboards and user interfaces, improving how data is interpreted and acted upon.”
The integration of multiple TPMS systems represents a particular competitive advantage. “enTIRE PressureNet is sensor brand-agnostic and integrates with multiple sensor types, unlike many manufacturer-locked systems,” Fernie explained. “Our independence allows clients to choose or switch sensor brands without losing backend compatibility.”
FIGHTING FRAUD IN HIGH-STAKES OPERATIONS
In addition to optimising operations and pre-emptive maintenance, enTIRE is an advanced fraud detection and prevention solution in settings where a single tyre costs more than high-end cars. The software’s detailed tracking identifies many forms of theft, tampering and misbehaviour that afflict the high-end tyre market throughout global mining operations.
“Tyre fitters may scrap a near-new tyre (if not tracked) and then this tyre would be picked up from the scrap location and resold,” Fernie explained, detailing one common fraud scheme. “In mining, each tyre can be worth up to USD 50,000. This potential additional income is very significant in developing countries.” The financial incentives for such fraud are substantial, making comprehensive tracking systems essential for asset protection.
Beyond simple theft, the system prevents more sophisticated data manipulation during high-stakes contract negotiations. “If a tyre supply contract is worth USD 100 million, there can be significant pressure placed on operators of any tyre management system to ‘modify’ tyre performance in a supplier’s favour,” Fernie said, highlighting the system’s role in maintaining data integrity. “enTIRE has very strong internal systems to prevent internal tampering.”
Other fraud prevention features involve detecting unauthorised tyre replacement in off-site fleet operations, where drivers may sell new tyres and substitute them with less expensive ones, and preventing early scrapping of tyres that can otherwise be retreaded or reallocated for a longer service life.
ORGANIC GROWTH STRATEGY AND MARKET POSITION
VMC has achieved its market-leading position without relying on venture capital investment or large corporate sponsorship; instead, it has relied on diligent organic growth fuelled by strong customer relationships, word-of-mouth referrals and relentless reinvestment in product development. The firm purposefully reinvested earnings in automation technologies and enhanced software capabilities, rather than engaging in fervent hiring or costly promotional campaigns, while maintaining lean operations and establishing increasingly refined development capabilities.
“When large manufacturers’ systems failed with over-engineered projects, clients often came to us for reliable replacements,” Fernie said, describing a pattern that has accelerated during recent supply chain disruptions when tyre shortages made lifecycle extension critical for maintaining operational continuity.
The company’s fundamental growth strategy centres on systematic data accumulation and market share expansion. “Our strategy, early on, has always been to increase market share as we realised that the more tyre performance data our systems controlled, the more valuable we would become,” Fernie explained, articulating a network effect strategy that becomes more powerful with scale.
This field-tested software, combined with deep industry connections and vast databases, now creates major entry barriers that would require competitors years and millions to overcome.
DIVERSE APPLICATIONS AND INDUSTRY DIFFERENCES
VMC software supports significantly disparate operating models in mining and transport industries, each with dissimilar tracking demands and cost-justification criteria. Mining applications typically involve high-cost, low-volume tyres that are closely monitored by operating hours. In contrast, transport fleets manage high-volume, lower-cost tyres, which are tracked by kilometres and frequently shared across interchanging trailers pulled by various prime movers.
“Mining justifies the cost of extensive data entry based on the large cost savings, while the transport industry is more careful regarding tracking cost,” Fernie explained, highlighting how economic incentives drive different implementation approaches across industries.
Its flexibility in covering these differing operational needs while ensuring consistent data quality and analytical functionality across both industries is possible with the software.
GLOBAL EXPANSION AND CULTURAL ADAPTATION
VMC continues to expand its global presence, with a specific emphasis on high-growth regions such as Africa, Indonesia, India, Eastern Europe and Latin America, where a large demand for advanced asset management solutions arises from growing mining activities and infrastructure projects.
The firm has local teams offering multilingual support capabilities. However, cultural adjustment remains a continuing challenge in emerging markets as they transition from legacy manual systems to online platforms.
“We adapt training and user interfaces to local literacy and workflow styles,” Fernie said. “Regional teams help bridge gaps in communication, training and change management, ensuring smoother adoption.”
Main entry barriers in emerging markets include the absence of sound local technical support, the scarcity of internet infrastructure in geographically remote mining sites, the reluctance to change due to entrenched manual systems and administrative hurdles involving payment reliability and bureaucratic delays.
FUTURE TECHNOLOGY AND INDUSTRY TRENDS
Future software updates mirror industry-wide trends towards greater automation and the integration of artificial intelligence. On the horizon are planned improvements, including richer analytical dashboards, enhanced cloud analytics capabilities, mobile inspection tools with integrated image capture capabilities and AI-driven notification systems for predictive maintenance notifications.
As autonomous and electric cars increasingly penetrate mining fleets, VMC’s strategic emphasis on tyre and rim information, rather than vehicle powertrains, places the company well-positioned to meet emerging transportation technologies without necessitating drastic system architecture adjustments.
“enTIRE tracks data independently of vehicle type, so electric vehicles are managed the same as diesel fleets,” Fernie explained. “Our focus is on tyre and rim data accuracy – not the powertrain.”
INDUSTRY CHALLENGES AND MARKET OUTLOOK
The tyre management industry faces ongoing challenges related to data accuracy and actionable insights. “The industry’s main challenge is accurate and actionable data,” Fernie observed. “Successful tyre management operations start with accurate data collection, management and transparent reporting.”
Supply chain disruptions have strengthened demand for VMC’s services as tyre shortages heighten the importance of lifecycle extension and predictive maintenance. “Our strongest growth has been when there have been tyre shortages and clients want to extend their current tyre life as much as possible,” Fernie noted.
For Fernie, who brings over 30 years of experience in tyre management software development to the industry, VMC’s continued success validates the strategic decision to remain independent in an increasingly consolidated market. “Just ‘being there’ and remaining independent will always attract customers from non-independent tyre management systems over time,” he said, expressing confidence in the company’s long-term competitive position.
In an industry where margins of operation are crucial and safety must not be compromised, VMC has established a highly profitable niche by addressing complex problems that most individuals never even consider – until a USD 50,000 tyre blows on a distant mining operation thousands of miles from the nearest replacement. For mining operators globally with billions of dollars in mobile equipment, that specialised expertise and uncompromising independence have been worth their weight in gold.
VMI Launches Modular COMBEXX RF System For Low-Shear, High-Quality Compound Straining
- By TT News
- November 18, 2026
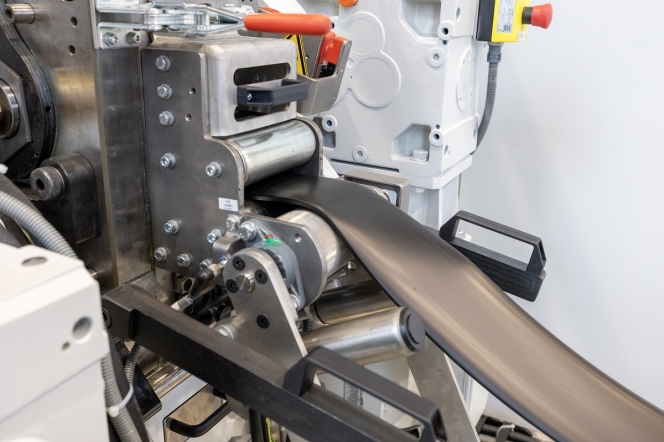
VMI has launched the COMBEXX RF (Roller Feeder) machine, a modular system that redefines integrated straining by replacing traditional extruder screws with a precision roller unit. The new system offers manufacturers a compact, energy-efficient and high-quality alternative to conventional plasticising screw mechanisms, drawing on VMI’s decades of expertise in extruder gear pump systems.
The COMBEXX RF is designed to address key challenges in modern mixing lines, namely incorporating a compound straining process within limited floor space while minimising thermal exposure. By delivering direct, low-shear feeding, the roller feed system preserves material integrity throughout the process.
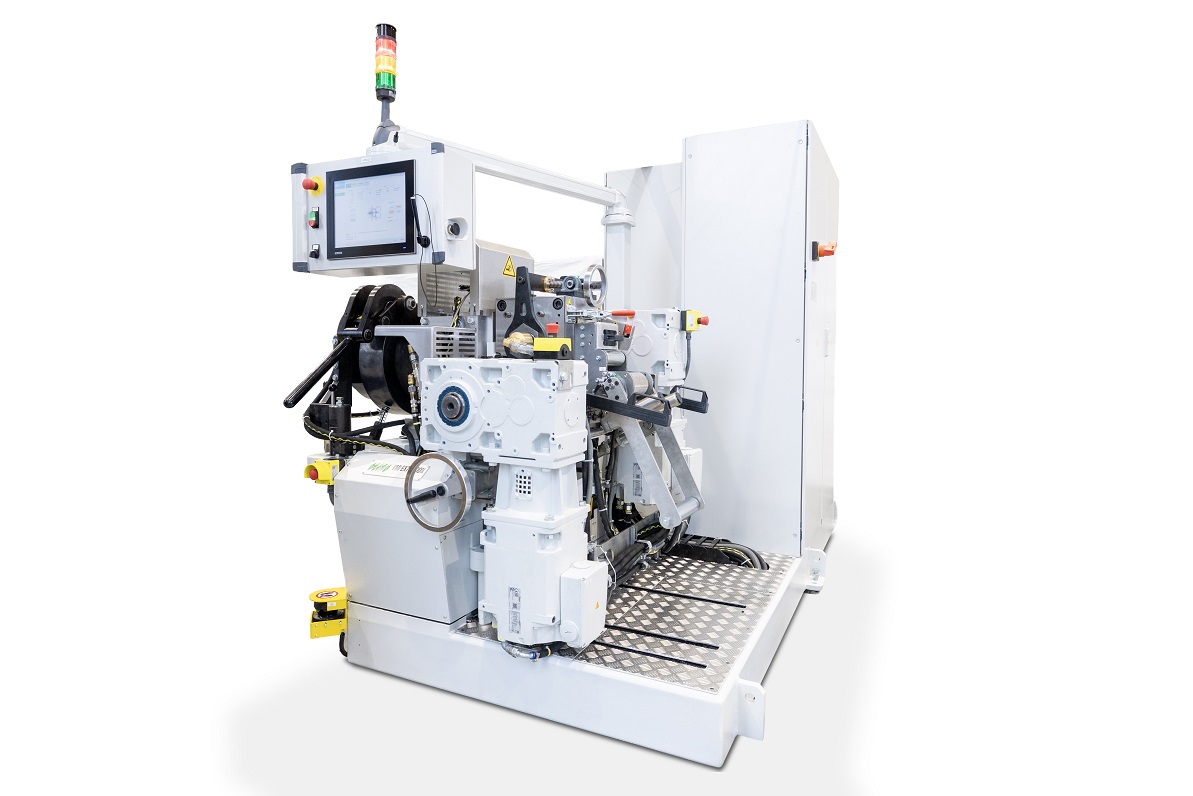
The system provides several advantages for manufacturers. Its compact design and smaller footprint improve space optimisation compared with screw-driven extruder gear pumps. Cost efficiency and quality preservation are achieved because the system eliminates the need for secondary heating, cutting energy consumption and preventing alteration of compound characteristics. The COMBEXX RF is also engineered for seamless integration into existing mixing lines and can be rapidly moved into place when continuous straining is required, with availability in different sizes and capacities.
Coen Heukshorst, Sales Manager, VMI, said, “The COMBEXX RF represents a significant step forward in how we approach integrated straining. By removing the extruder screw and relying on our proven roller technology, we are answering to current market demands. It’s a solution that fits the modern plant’s need for flexibility and efficiency.”
Michelin And Academic Partners Launch I-TireLab Joint Laboratory
- By TT News
- November 05, 2026
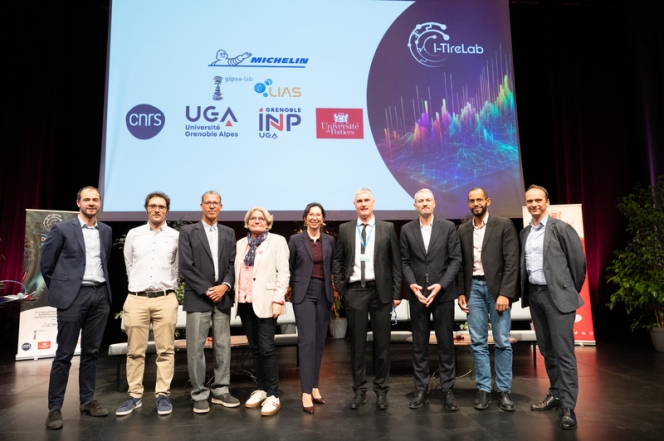
Michelin has partnered with the University of Poitiers, Grenoble Alpes University, Grenoble INP – UGA and the CNRS to launch I-TireLab, a joint laboratory combining data and modelling to pursue advances in tyres, tyre manufacturing and flexible composites. The project carries a total investment of roughly EUR 4.5 million over four years and is intended to close the gap between academic research and industrial challenges.
The laboratory pairs Michelin's expertise in tyre simulation and modelling, materials and industrial processes with the modelling, system state estimation and control methodology strengths of the Laboratory of Computer Science and Automatic Control for Systems at Poitiers and the GIPSA-lab, which unites UGA, CNRS and Grenoble INP – UGA. Though the partnership has operated for several years, I-TireLab gives it a long-term framework aimed at turning data into knowledge, decisions and actions.
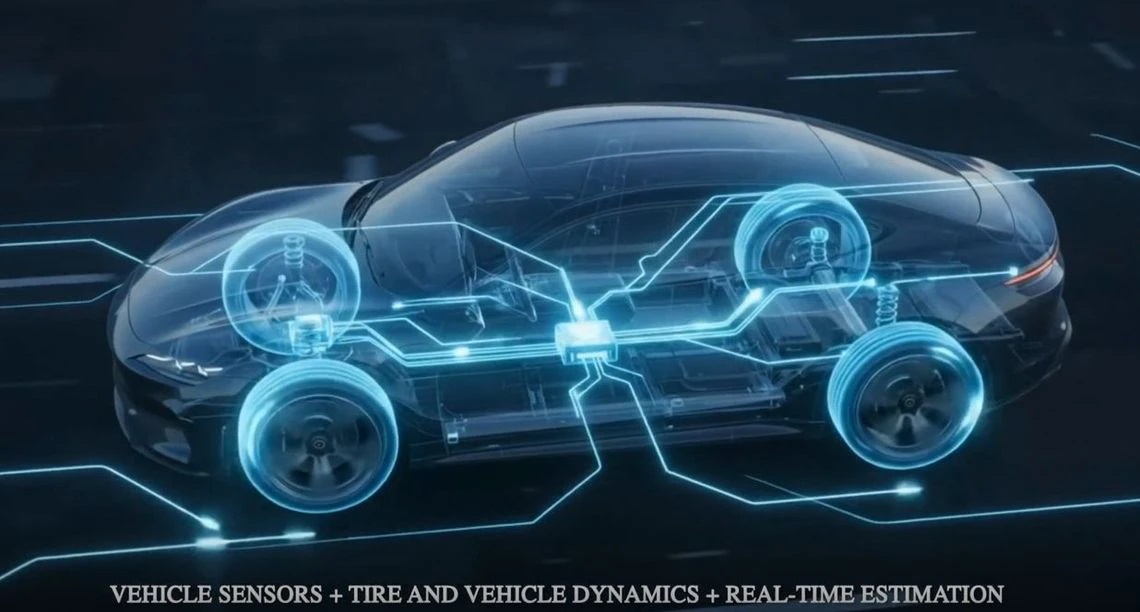
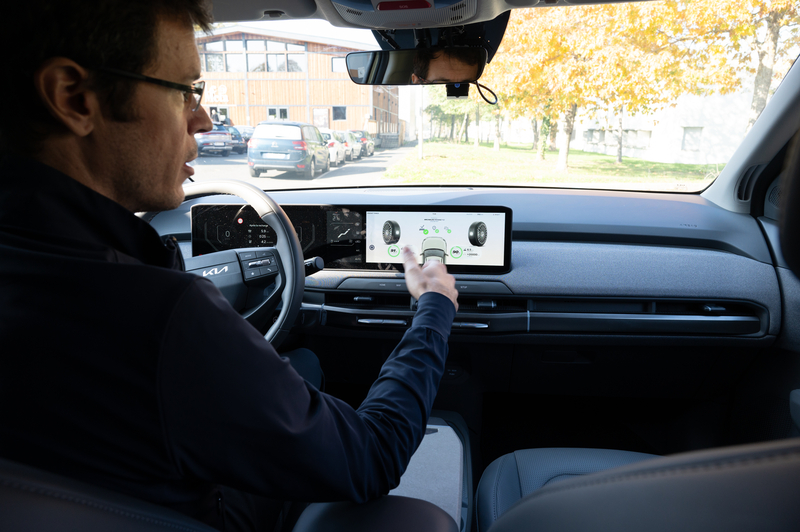
The teams combine data analysis and modelling to represent and predict the behaviour of tyres, processes and materials, then test the relevance and limits of those models through data and experimentation. Four research themes support safer, higher-performing mobility, less resource-intensive manufacturing and new applications for flexible composites.
The first theme targets a clearer view of tyre condition on the road, including real-time estimates of wear and grip using existing on-board sensors without specialised equipment. The second feeds that information into vehicle control systems, optimising braking based on tyre status and grip potential to enhance stability and efficiency. The third addresses rubber manufacturing, developing simulation and control tools to anticipate equipment operation and fine-tune settings while maintaining consistent quality and limiting waste and energy use. The fourth explores how flexible products can influence air and water flows around objects through control laws that alter component shapes.
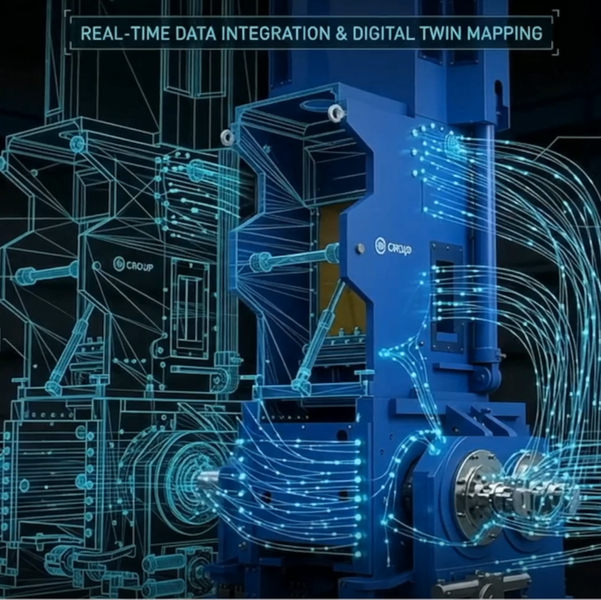
Michelin contributes product-usage understanding, data and experimental and industrial resources, while the academic laboratories supply theoretical and methodological expertise for designing and validating new approaches. The collaboration also helps train young researchers at the interface of fundamental research, experimentation and industrial needs, with access to demonstrators and partner-site tests for near-real-world assessment.
Planned applications include supporting Michelin Touch Intelligence, the tyre digital twin unveiled in May 2026 that estimates pressure, wear, load and grip in real time without extra sensors across all brands and models. Research on certain flexible composites could also inform Wisamo, Michelin's inflatable, retractable automated wingsail, whose first unit is in delivery and which uses wind to boost ship propulsion and cut fuel consumption.
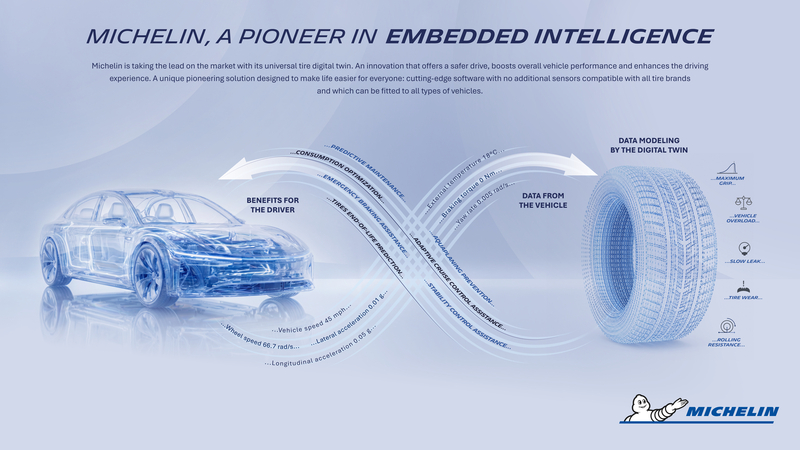
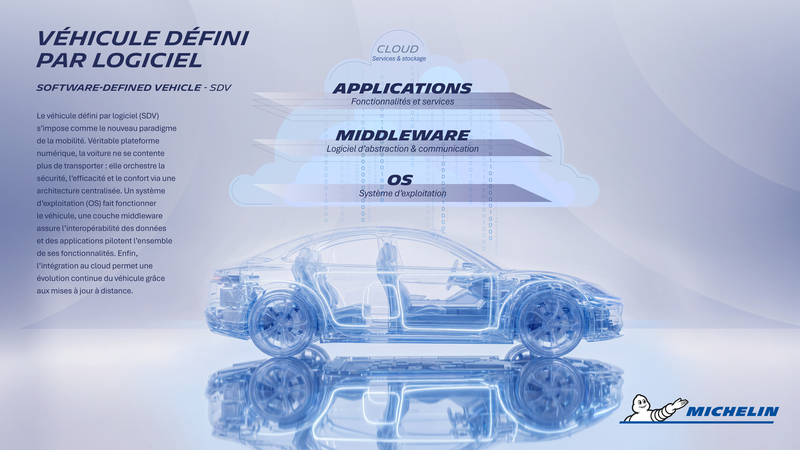
Philippe Jacquin, Michelin General Manager & Director of Research and Development, said, “I-TireLab will make it possible to turn science into real-world innovations, from tyres and tyre manufacturing to tyre-vehicle interactions. Michelin Touch Intelligence, the tyre digital twin is one recent illustration of what that means in practice: when we know more about the tyre’s status and grip potential, we can enable vehicle adjustments and optimisation.”
Guillaume Mercère, I-TireLab Director; John Martinez-Molina, I-TireLab Co-Director and Thibault Dairay, I-TireLab Co-Director, said in a joint statement: "I-TireLab brings together researchers, engineers and young scientists to make mobility safer, improve our control of tyre manufacturing, and explore new possibilities for flexible materials. By drawing on fundamental research, experimentation and industrial needs, we are developing new methods, training talents and preparing the innovations of the future, together.”
Mehdi Gmar, CNRS Deputy CEO for Innovation, said, “I-TireLab once again demonstrates that the expertise and knowledge developed in academic research laboratories – in this case, at GIPSA-lab in modelling and control of complex systems – have industrial applications. This is now the case with Michelin across very different areas: tyres on the road, rubber manufacturing and flexible materials supporting safer, more resource-efficient mobility.”
- Swarnakaruna Princeton Rubber Industries
- N Swarnalatha
- Princenton Rubber Industries
- retreading
- tyre
- Ashish Kumar Isukapati
- IFCI Venture Capital
State-Backed Capital Powers Swarnakaruna Princeton’s Expansion Push
- By Gaurav Nandi
- November 02, 2026
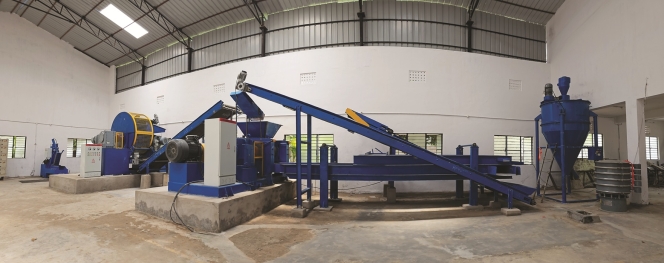
Swarnakaruna Princeton Rubber Industries has built capacity to recycle about 96,000 end-of-life tyres annually after government-backed financing helped the Visakhapatnam company transition from processing buffing waste to recycling whole tyres. The recycler is now targeting larger industrial buyers while exploring tyre imports to lower raw-material costs.
India’s push to formalise its end-of-life tyre recycling ecosystem is creating room for smaller recyclers to scale, but access to capital, machinery reliability, raw-material costs and the economics of producing higher-grade crumb rubber remain significant constraints.
Visakhapatnam-based Swarnakaruna Princeton Rubber Industries Private Limited offers a case in point. The company has expanded from a small operation processing buffing powder to a whole-tyre recycling business capable of producing around 300–400 tonnes of crumb rubber a month following financial support channelled through IFCI Venture Capital under a government-backed programme for Scheduled Caste entrepreneurs.
The business traces its roots to 2014, when Managing Director N Swarnalatha established K.S. Princeton Rubber Industries after approaching the District Industries Centre in Visakhapatnam with plans to become an entrepreneur.
The original operation had a single grinder and relied on buffing powder as its principal feedstock because it lacked the equipment required to process complete end-of-life tyres.
“The company started in 2014, but the setup was very minimal. We had just one grinder and were not capable of recycling a whole tyre, so buffing powder was our raw material,” said Swarnakaruna Princeton Rubber Industries Chief Executive Officer Ashish Kumar Isukapati.
That model began changing in 2018 when the company sought funding from IFCI Venture Capital Limited. The proprietorship was subsequently converted into a private limited company as part of the process of securing the investment. Funding was eventually released in stages, with commercial production from the expanded facility beginning in August 2024.
According to Isukapati, the project received about INR 50 million from IFCI Venture Capital, alongside a promoter contribution of INR 17.1 million. The overall project cost was approximately INR 67.21 million.
The money was deployed largely towards machinery and rebuilding and expanding the existing manufacturing premises.
Isukapati said the financing was particularly significant because conventional access to growth capital can prove difficult for first-generation entrepreneurs.
TYRES TO CRUMB
The expanded operation can process roughly 8,000 end-of-life tyres each month, equivalent to around 96,000 tyres annually, according to Isukapati. At the upper end of production, the facility can manufacture around 400 tonnes of crumb rubber a month, while recovered steel accounts for roughly 25 percent of output by weight or around 100 tonnes at that production level.
The company currently sells entirely into the domestic market, with Kerala representing its largest destination. It also supplies TVS Sundaram Industries in Chennai.
However, the economics vary considerably according to crumb size and end application.
More than 70 percent of the company’s current crumb-rubber production goes to non-tyre applications, particularly rubber-mat manufacturers in Kerala. These customers typically consume 20 and 24 mesh material. TVS Sundaram Industries takes roughly 60–80 tonnes a month, with the company supplying 30-mesh crumb rubber.
Tyre-related customers typically require finer grades such as 40, 60 and 80 mesh crumb rubber. The company has pulverising equipment capable of producing material in those ranges, but finer grinding lowers throughput and changes the economics of the operation.
“We are capable of manufacturing the higher meshes, but the overall output comes down. We have to balance which mesh we manufacture against the quantity we can produce because crumb rubber itself is a relatively low-priced product. The way to generate sustainable revenue is through volume,” Isukapati said.
That volume-quality equation has become particularly important as the recycler seeks to tap larger customers closer to its Visakhapatnam plant.
One of its main targets is HINCOL, which Isukapati said operates a facility locally and requires around 500 tonnes of crumb rubber a month. The company has so far been unable to fully address that opportunity because of the combination of volume, quality specifications and tender pricing.
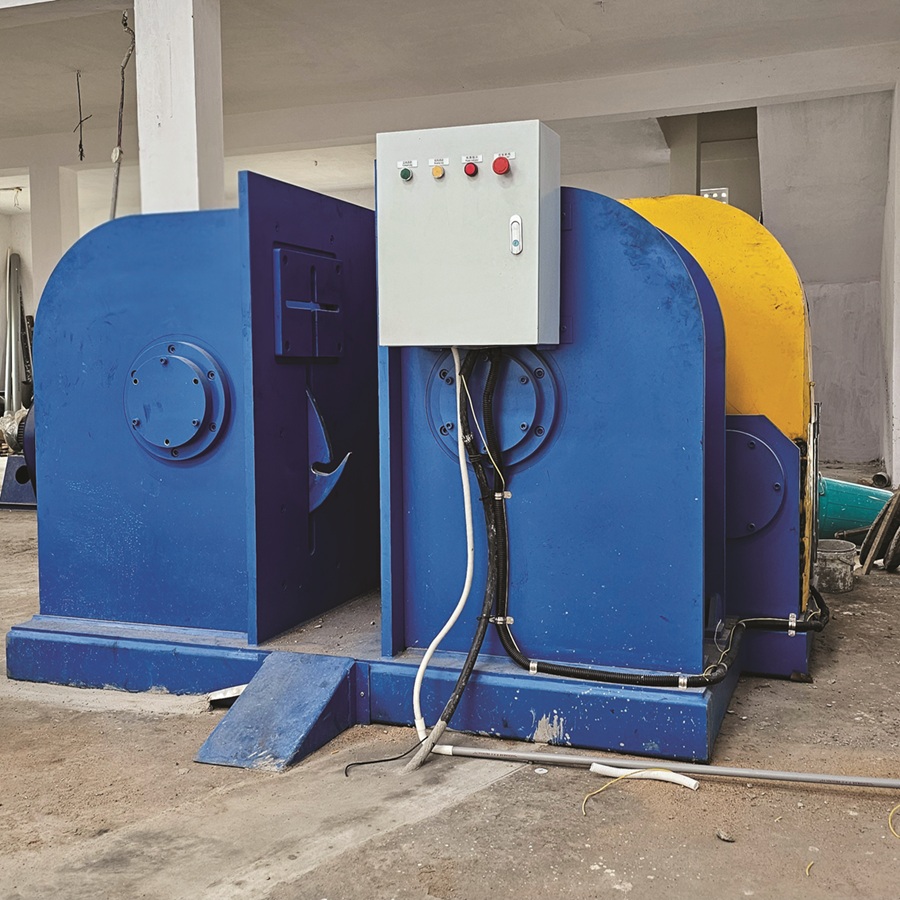
Isukapati sees similar opportunities with buyers across the eastern and southern tyre and rubber manufacturing belt. He estimates that potential demand within roughly 300 kilometres of its operation could exceed 1,000 tonnes a month.
The challenge is converting that proximity into profitable sales.
PORT OPPORTUNITY
The company currently sources a significant portion of its tyres through Andhra Pradesh State Road Transport Corporation auctions. And the company is also seeking a licence to import end-of-life tyres, a move it believes could allow it to leverage its proximity to Visakhapatnam port and reduce feedstock costs.
“We are trying to capitalise on Visakhapatnam port and have applied for an import licence. If that works out, we could spend less on raw material, which would give us an advantage in offering a more competitive price,” Isukapati said.
The company’s expansion has not been without setbacks. Location presents a significant constraint. The facility operates on a plot of about 980 square yards, where incoming tyres, finished crumb rubber and recovered steel all have to be stored and managed. Expanding towards the 500-tonne monthly volumes sought by larger customers could therefore require the company to address its space limitations.
Technical support and spare-part availability are also more difficult in Visakhapatnam than in established manufacturing clusters, Isukapati said.
BIGGER CHALLENGE
Swarnakaruna does not currently operate a dedicated research and development department. Product development and process adjustments are handled by its production manager and technical staff, while third-party laboratories are occasionally used when customers require test reports.
Beyond the company’s own expansion, Isukapati sees feedstock pricing as one of the biggest problems confronting India’s mechanical tyre recyclers.
Waste-tyre prices can rise when pyrolysis operators increase production, but crumb-rubber producers cannot necessarily pass those higher costs to customers because buyers have multiple competing suppliers.
He also called for greater policy attention to the procurement and channelisation of waste tyres, arguing that mechanical recyclers do not necessarily receive a commercial advantage for converting end-of-life tyres into reusable rubber products.
His comments come as India’s tyre-recycling ecosystem adjusts to extended producer responsibility requirements and increasing competition for waste-tyre feedstock.
For the tyre recycler, the next phase will therefore be less about simply adding equipment and more about achieving scale economically. The company is seeking cheaper feedstock, higher production, access to larger nearby customers and potentially a more formal research and development structure.
Recovered steel also remains important to the economics of the operation. Despite the constraints, he sees a sizeable addressable market around the company’s Visakhapatnam base.
“The opportunity is absolutely there. If we can get the right balance between the mesh we manufacture, the quantity we produce and the price, there is a huge opportunity out there,” Isukapati said.
- DUNLOP
- Sumitomo Rubber Industries
- SENSING CORE Technology
- Wheel Detachment Prediction Detection System
- Isuzu Motors
- Medium-Duty Trucks
Dunlop's SENSING CORE Adopted For Isuzu FORWARD Trucks
- By TT News
- October 30, 2026
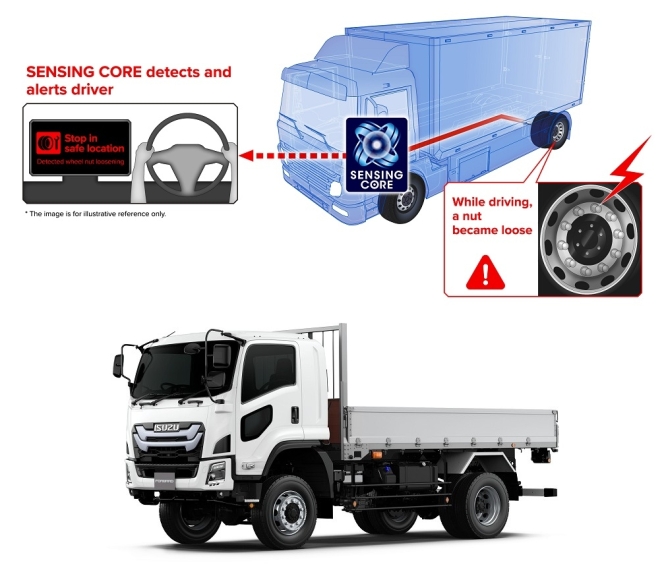
DUNLOP (company name: Sumitomo Rubber Industries) has confirmed that its proprietary SENSING CORE technology has been adopted for medium-duty truck models. The system, designed to detect the conditions of tyres, vehicles and road surfaces, is fitted to Isuzu Motors' FORWARD medium-duty trucks with a gross vehicle weight exceeding 14.5 metric tonnes, which come standard with the Wheel Detachment Prediction Detection System, one of the functions offered by SENSING CORE.
SENSING CORE is a software technology built on expertise gained from the Deflation Warning System, a tyre pressure warning system. It analyses wheel speed data generated by tyre rotation together with controller area network data transmitted through the vehicle's control system, allowing it to detect various tyre and road conditions, including tyre pressure, wear, load and signs of potential wheel detachment. The Wheel Detachment Prediction Detection System in Isuzu's FORWARD models detects loosening of wheel nuts while the vehicle is in motion, alerting the driver through a warning message and buzzer if an abnormality is found.
This capability complements conventional inspections and driver experience and is expected to play a significant role in preventing wheel separation accidents. Isuzu's FORWARD is a medium-duty truck with a broad lineup designed to meet diverse logistics industry needs, and such trucks are widely used in local delivery, long-haul transport and building and construction operations, serving as a vital means of transportation.
Operated across urban areas and major highways, wheel detachment accidents involving these trucks could cause serious harm to third parties such as pedestrians and cyclists, driving growing societal demand for improved safety. Preventing such accidents requires fundamental inspection and maintenance measures, yet drivers find it difficult to detect loosening wheel nuts while driving, making early-detection technologies essential. The provision of the Wheel Detachment Prediction Detection System to medium-duty trucks enables early detection of signs of vehicle malfunctions and contributes to further improving safety and preventing wheel detachment accidents.
Comments (0)
ADD COMMENT