GUIDE TO RUBBER SELECTION
- By Dr. Samir Majumdar
- December 29, 2020
In the 1930s, when rubber became one of the essential commodities, selection was never a problem because we had only Natural Rubber (NR) that time. Today, beyond 2010, there are number of elastomers are being used in the industry and the choice is typically important with respect to the competitive advantage of both, durability in the service and cost.
NR was called rubber because it could have rubbed out pencil mark. When other synthetic rubbers were produced, they had also similar property of rubbing out pencil mark, but were called elastomers because NR was then typically identified as Rubber. However, both NR and other synthetic rubber (SR) together are called elastomers, because they had typical elastic properties and interestingly, all rubber and elastomers are high polymers. From the time 1930 , industries have increased many folds of time. Engineering requirement in the manufacturing industries, with respect to temperature, pressure and durability have also simultaneously increased and our demand on the applications have also been increased.
CAPTION Fig.1: Asia Pacific Total Elastomers (54%), NR+SR
With very competitive demand in the market, all rubber properties cannot be achieved only by NR. Balancing critical demand for rubber applications, that we require in our day to day life, use of SR or blending with SR has become very common practice in the industry today.
For example, other than pneumatic tyre, there is hardly any uses of NR these days in automotive industries. Uses of various grades of EPDM, Silicone rubber (Q), Nitrile rubber(NBR), Fluoro Elastomers (FKM) , Perfluoro Elastomers (FFKM) , Hydrogeneted Nitrile rubber (HNBR), Chlorosulphonated Polyethylen (CSM), Polychloroprene(CR) , Polyurethane Rubber (AU/EU), Fluorosilicone Silicone Rubber (FQ) etc. have been increased due to typical automotive parts requirement. Since automobile spares are now mostly manufactured in Asia Pacific countries, they are the largest consumer of total elastomers (Fig.1).
CAPTION Fig.2: Only SBR is the highest (47%) synthetic rubber
After NR, the next high consuming elastomer is SBR (Fig.2) because of its higher filler and oil loading capability and higher abrasion resistant quality. After SBR, the next high quantity rubber used is BR, followed by IIR (BIIR,CIIR) and EPDM. Recently silicone rubber uses have increased many fold times in Western countries, China, Japan, Korea and in India. However, the total SR uses remains highest in Asia Pacific(Fig.3).
CAPTION Fig.3: Asia Pacific Highest Consumer of SR (48%)
In critical applications, it is therefore, advisable to give considerable thought, or take advice, on the formulation of the compound. As the potential for 'tailoring' compound to specific applications is essentially limitless, it is often advisable to carry out preliminary qualification tests to ensure that the compound chosen will perform as intended by customer need.
A considerable thought in critical applications, for the formulation of the specific compound need considerable experience with selecting raw materials and art of processing. Very common mistakes by rubber compounder is mostly related to incorrect selection of (1) ingredients, (2) their doses, (3) rubber blends and (4) correct machines. Rubber compounding is an art of developing rubber mixtures with suitable raw material and their doses, that will perform in desired services but with minimum cost possible such that product can be competitive in the market and can be processed well in machines without any difficulties faced by man and machines.
There are broadly two classes of Rubbers or elastomers, they are Natural Rubber (NR) and Synthetic Rubber (SR). NR occurs naturally in the plant and hence the name but all synthetic rubbers are man made rubbers and are produced by chemical synthesis. Among the Synthetic elastomers, there is again two category; one is general purpose rubbers (GPR),which can be used as equivalent to NR, e.g., Butadiene Rubber (PBR) and Styrene Butadiene Rubber (SBR) and the other category is specialty elastomers. Specialty elastomers are generally costlier than GPR and are only used in special purpose. Following are the list of specialty elastomers ,which are widely being used in rubber industry beyond 2000:
Butyl Rubber (IIR), Chlorobutyl Rubber (CIIR), Bromobutyl Rubber (BIIR), Chlorinated Polyethylene(CM), Chlorosulphonated Polyethylen (CSM), Ethylene Acrylic(EEA) , Ethylene Propylene Rubber(EPM) , Ethylene Propylene Diene Rubber(EPDM), Fluoro elastomers (FKM), Hydrogenated Nitrile Rubber (HNBR), Isoprene Rubber (IR), Nitrile Rubber(NBR) , Polyacrylic Rubber (ACM), Perfluoro Elastomers (FFKM), Polychloroprene (CR) , Polysulphide Rubber (TR) , Polyolefin Elastomer (POE), Polyurethane Rubber (AU/EU) , Silicone Rubber(Q), Fluorosilicone Silicone Rubber (FQ) etc.
Elastomers having carbon-carbon double bond on the elastomeric backbone could be cross-linked with sulphur and accelerators. Many of these elastomers are also could be cured with organic peroxides, examples are NR,SBR,BR, AU/EU, CM, CR,CSM,EPM,EPDM,FPM,NBR,HNBR,IR,POE,Q,FQ. Elastomers that cannot be cured with organic peroxides are; ACM,IIR,CIIR,BIIR,ECO.
Rubber compounding
Rubber compounding is an art of developing rubber mixtures with suitable raw material and their doses, that will perform in desired services but with minimum cost possible such that product can be competitive in the market and can be processed well in machines without any difficulties faced by man and machines. In all rubber industry today, the biggest challenge is cost reduction of a good quality product. During selecting raw materials, therefore, the cost of these will also play a vital role in compound designing.
A rubber product might require desired physical properties and ageing properties. For this one need to add particular reinforcing filler or a suitable combination of reinforcing fillers to have desired physical properties. The typical ageing resistant property may be achieved with only NR by adding suitable anti-degradants or, NR could also be blended with synthetic elastomers with better ageing resistant property. NR being cheaper and easily available it is the first choice having good strength, abrasion , tear strength and low heat development in dynamic condition. A synthetic rubber product might require good green strength , in that case either NR or blend of rubber is the choice. For example, for better green strength of CIIR, it is often blended with NR.
CAPTION Fig.4: Turn-up Bladders
A rubber product may require a specific need , say air retention property or oil resistance property. For the former case the choice is essentially butyl rubber (or, halobutyl rubber , CIIR,BIIR) and for the later it is usually, NBR/HNBR and for both oil resistance and air impermeability, the usual choice is NBR / HNBR rubber (Turn-up bladder for tyre building operation, Fig.4). For a typical product, if the property demands oil resistance at 200 0C, then the choice is FKM (Fluoroelastomers) or Q. For resistance upto 328 0C , it is FFKM.
CAPTION Fig.5: Typical Industrial Gaskets
Heat resistance property is typically related to product durability and sustainability at desired temperature and is very important for various industrial gaskets (Fig.5). For temperature resistant rubber compounding and following temperature resistance of the polymer is important, NR ~ 65 °C, SBR ~ 75 °C, NBR ~ 110 °C, HNBR ~ 180 °C, Q ~ 200 °C+, FKM ~ 240 °C, FFKM ~ 328 °C. The temperature ranges quoted are only a rough guide, because the temperature resistant property also depend on the typical compound design as well, depends upon the particular application, and may depend on detailed differences between alternative versions of the same rubber.
Rubber compound is always developed as per customer need. For any rubber article, the first choice is the selection of right rubber. Rubber is selected mostly on the basis of :
- Cost
- Heat and/or Oil Resistance
- Temperature Requirements
- Energy Absorption
- Seal Ability
- Flex Resistance
- Water Resistance
- Gas Impermeability
- Electrical Properties
- Abrasion Resistances
- Dynamic Properties
- Flame Resistance
Rubber compound related definitions
- Elastomer, a polymeric material that recovers substantially to its original shape after significant deformation at room temperature.
- Compound, a mixture of elastomer and other materials that is intended to process (mold) satisfactorily and meet end-use specifications.
- Filler, a particulate material added to an elastomer that modifies both the workability and the end-use behavior of the resulting composition.
- Plasticizer, a material added to an elastomer to improve its workability.
- Resins are added to improve rubber tack.
- Waxes also used as plasticizer , are also added for smooth finish of rubber articles.
- Antioxidant, a chemical added to a compound to slow or prevent oxygen attack on the compound.
- Antiozonant, a chemical added to a compound to prevent ozone attack.
- Cross linking agent, a chemical added to a compound to link the long molecules in a polymer together, or to assist in the cross-linking process.
- Accelerator, a chemical added to a compound to increase the rate of cross-linking in the compound.
- For example, sulfur links the long molecules, while an accelerator increases the cross-linking rate.
- Retarder, a material added to an elastomer compound to delay the onset of cross linking (scorch).
- Vulcanization is same as cross-linking but with sulphur.
- Peroxide also helps in cross-linking process.
Elastomer blends
Elastomer blends often creates problem when two different types of unsaturated rubbers are mixed and vulcanized together. For example, NR and IIR have two different unsaturation level and hence both sulphur , ZnO and black flows more towards polar rubber, on NR phase, and results undercure in IIR phase and the resultant blend vulcanizate becomes spongy and cannot be used.
GPR (NR,SBR,BR) rubber could be blended to any proportion. For higher synthetic rubber level (BR,SBR) , accelerators dose is often adjusted to higher side and sulpur level is adjusted to lower side, because for equivalent curing, BR, SBR requires more accelerators as compared to NR. Stearic acid is added 2-3 phr with only synthetic elastomer and for NR, stearic acid dose of 0.5 phr is enough.
CAPTION Fig.6 : Micro Dispersion of Rubber Blends
Practically most of the polymers are not miscible to 100%, polymer blends usually consist of micro-dispersion of one rubber into the other rubber and this results after intensive mixing of these two different polymers. These micro dispersed rubber often has dimensions around 0.1-1.5 nm(Fig.6). When fillers are also mixed into such blends, a situation may develop in which the filler unevenly distributed between two phases. Such uneven distribution of fillers, naturally effects the uniformity of compound physical properties. In most blends the effect on the properties of blended elastomers depend on:
- The polymer compatibility
- Distribution of fillers in different phases and
- The degree of cross-links between rubber phases
Though NR,SBR,BR could be blended to any proportion , yet the blended phases are not compatible to hundred percent and there is also phase separation, where, on proper identification one can witness that there is phase separation with NR & SBR, NR & BR, BR & SBR. However, upon proper mixing these phase differences could be minimized (Fig.7) such that the resultant blend gets cured almost homogeneously . That is why very highly dispersed NR (5 to 10 parts) could also be co-cured with IIR.
CAPTION Fig.7 : Well Dispersed Rubber Blends
IIR cannot be blended with GPR but can be blended with EPDM (having ENB diene content between 2-3 mole%) to any proportion. Higher diene content EPDM rubber (ENB, >9.0% mole) could be well blended with GPR. If high diene content EPDM is blended with IIR, filler, sulphur, accelerator and zinc oxide flows more towards EPDM than IIR. IIR could be blended with CIIR and BIIR to any proportion. Such blend is often used in making tyre inner-tubes and hose jacket compounds. When CIIR and BIIR doses are on the higher side with IIR (>60phr) it is worthwhile that zinc oxide is added in the final batch since zinc oxide is curative for CIIR & BIIR.
Besides zinc oxides, CIIR and BIIR can also be cured with sulphur/accelerator system as well. However, for very good heat resistant property, they are often cured with ZnO. Highly dispersed plastic (LDPE) could also be blended with CIIR/BIIR with no detrimental effect but with improvement on air permeability.
CIIR and BIIR could be blended to any proportion with GPR. Such blend is often used in tyre inner liner. When CIIR and BIIR doses are on the higher side (>60phr) both zinc oxide and amine type anioxidant/antioxonates are added in final batches as these are curatives in CIIR and BIIR.CIIR blend with GPR and EPDM is used in PC sidewall for glossy finish sidewall and addition of CIIR also help to reduce the curing time of PC tyre. Blend of EPDM/NR/SBR and EPDM/NR/SBR/CIIR are often used in tyre side wall compound for better look.
CR rubber is not normally blended in the industry as it is mostly used in adhesive industry. However, they can be blended to any proportion with GPR. In adhesive industry crystallinity is important and CR gives the highest degree of crystallinity among all general-purpose rubber. CR could be blended with IIR , close to 5-15 phr, for bladder making and in general, only 5.0 phr is added in the beginning of the mixing cycle.
In bladder mixing, Zinc oxide could be mixed with CR in master batch. CR is premasticated in mixing mill for making bladder compound, before adding in Banbury.CR/BR blend is used in hose covers.CR could also be blended with GPR at any proportion like CIIR. Both zinc oxide and amine type antioxidant / antioxonates are added in final batches as these are curatives in CR and CIIR.
In general Silicone rubber (MQ,PMQ,VMQ) cannot be blended with any other rubber because of phase difference problem but highly dispersed EPDM could be blended with it upto 10 -15 phr. EPDM/Q blend is used in heat resistant cover roll compound.
EPDM, being a good elastomer as weather resistant and heat resistant is often blended with number of other elastomers to get the benefit of the vulcanisates.
EPDM/CR blend are very popular in making gaskets. EPDM/IR blend is widely used in car wiper rubber blades. EPDM/SBR blends are used in gaskets, sponges and hose stocks. EPDM/CSM blend is used in transmission belt, conveyor belt and in hose covers. EPDM/LDPE blend is very popular in making cable insulation compound.
NBR in general, is not blended with other elastomers as this rubber having higher degree of polarity , is exclusively used for oil resistance property. It may have acrylonitrile content ( ACN) ranging from 18-50%. Incase of higher oil resistance, the elastomeric grade is selected with higher ACN. For better abrasion however, 10-20 phr of BR could be added to NBR with the aid of good dispersing agents , used in shoe sole, high abrasion resistance rolls and in conveyer belts. Higher ACN content will have better abrasion property. NBR could be cured both by sulphur/accelerators or by peroxides. Hydrgenated NBR (HNBR) has emerged into market with better heat resistant property as compared to NBR. For intermediate heat resistant property NBR and HNBR could be blended.
NBR/SBR blends used in hydraulic hose tubes, high pressure hose, belt cover, idler roll compounds and in gasket compounds. NBR/PVC blend and NBR/PVC/BR blend are used for roll cover compound, very popular in electric cable insulation and in closed cell sponge applications in shoe industry. XNBR/PVC blend is used for heavy duty cable jackets, roller cover, belt cover, hose cover stocks etc. NBR/IR blend and NBR/TR blend is popular in colored or non-black roll covers. The later is mostly used in printing roll cover compound.
Zeon Breaks Ground On Kawasaki Facility To Speed Lab-To-Mass-Production Scale-Up
- By TT News
- October 19, 2026
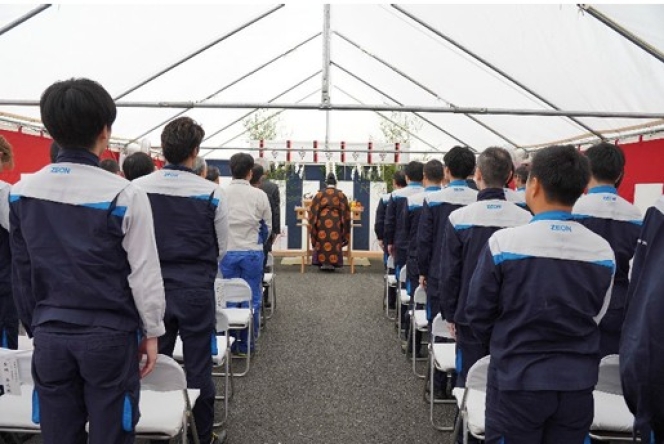
Zeon Corporation broke ground on a multi-product research and prototyping complex at the Kawasaki Innovation Frontier Port in Kawasaki City, Kanagawa Prefecture, on 16 October with a ceremony held beforehand to seek safety during construction. The company expects the complex to shorten the path from laboratory work to mass production for established and emerging businesses alike, making it central to its long-term growth strategy.
Set inside an existing building within the port's Research & Development Center area, the complex is slated to begin operating in January 2028. Its design aims to move products past the laboratory stage and into medium-scale sample output more quickly, clearing a bottleneck on the route to full-scale manufacturing.
Zeon's core production methods – polymerisation, hydrogenation, coagulation and drying – will be built into the complex, which is engineered to handle diverse manufacturing conditions and operating approaches. Beyond serving established and new businesses, the polymer design company envisions the site as a centre for technology development and a platform for rolling out new processes and operational, analytical, and measurement technologies within and beyond the company. It will eventually host development and prototyping work across a wide range of technologies, including contract prototypes commissioned by outside parties.
The Kawasaki Innovation Frontier Port is the umbrella name for the site combining the neighbouring Kawasaki Plant and Research & Development Center. The label underscores the location's role in breaking new ground by merging innovation, research and development and production and casts the Kawasaki waterfront as a port that propels innovation. Once a co-creative innovation facility begins operating in December 2026, the two sites will function as one continuous operation, turning out ever more sophisticated products and production methods and reinforcing their standing as a launchpad for technology.
Vipal Rubber Launches VT290 Tread For European Truck Market
- By TT Bureau
- October 13, 2026
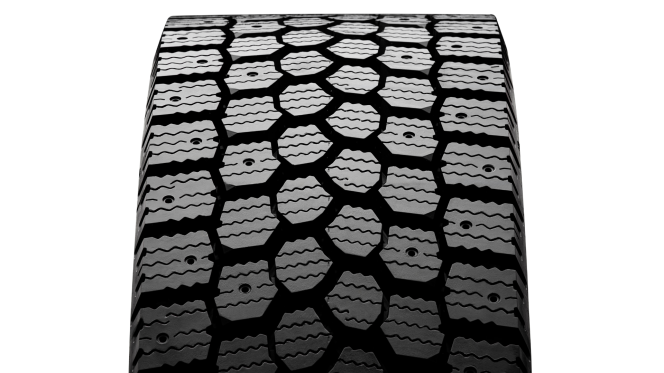
Vipal Rubber has launched the VT290, a tread designed for truck drive axles used on motorways and paved roads, targeting regional and long-distance transport operations in Europe.
The product is available in widths of 240mm, 250mm, 260mm, 270mm and 280mm. It is designed to provide traction and stability on dry and wet roads, as well as in demanding conditions involving snow.
Frederico Schmidt, General Manager of Vipal EMEA, said, “The launch of the VT290 reinforces Vipal’s ongoing commitment to offering technologically advanced solutions suited to the specific characteristics of European roads and climate.” “We want to further consolidate our presence in the region, delivering a high value-added product that combines innovation, operational efficiency and safety,” he added.
The VT290 carries the M+S marking and 3PMSF certification. Its design includes side sipes and grooves intended to help remove snow and mud from the tread, improving grip on slippery surfaces.
The tread pattern is also designed to distribute engine torque more evenly, helping to reduce uneven wear. Tie bars between the tread blocks add structural stability, supporting vehicle control during driving.
Fabrício Nedeff, Commercial Manager of Vipal EMEA, said, “With the VT290, weare responding directly to the real needs of fleet operators and truck drivers, combining performance, adherence and efficiency in different driving conditions. [RS2.1]In addition to expanding options for our customers, the product strengthens business opportunities for our partners in the region,”
Vipal said the launch would expand its offering for retreaders, distributors and fleet operators in the European market.
- Association of Natural Rubber Producing Countries
- ANRPC
- Monthly NR Statistical Report
- Natural Rubber
ANRPC Publishes Monthly NR Statistical Report For August 2026
- By TT News
- October 02, 2026
The Association of Natural Rubber Producing Countries (ANRPC) published its Monthly Natural Rubber Statistical Report for August 2026, noting firmer prices in several markets. Supply constraints, stable downstream demand and persistent geopolitical and macroeconomic uncertainty shaped the month. Renewed conflict and disruptions to major shipping routes added further pressure.
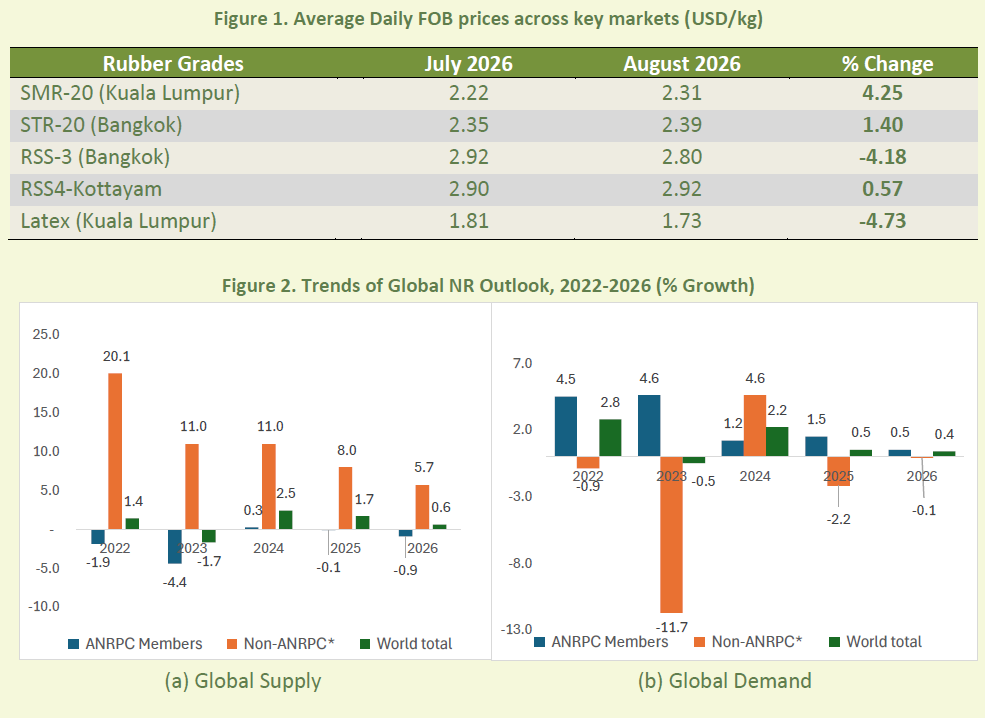
Physical prices for major grades moved in different directions. SMR-20 in Kuala Lumpur averaged USD 2.31 per kg, up 4.25 percent from July, while STR-20 in Bangkok rose 1.40 percent to USD 2.39 per kg. RSS-3 dropped 4.18 percent to USD 2.80 per kg, but RSS-4 in Kottayam gained 0.57 percent to USD 2.92 per kg. Latex-in-bulk fell 4.73 percent to USD 1.73 per kg. Brent crude averaged USD 91.08 per barrel, driven by concerns over possible restrictions on oil shipments through the Strait of Hormuz and wider Middle East instability, which raised energy supply risks and strengthened the oil market risk premium.
On trade, China's imports climbed 3.39 percent month-on-month, while India fell 10.18 percent and Malaysia dropped 8.24 percent; Viet Nam rose 5.08 percent. Exports advanced 5.63 percent in Viet Nam but declined in Thailand (-5.24 percent), Indonesia (-5.36 percent), Malaysia (-1.48 percent) and Cambodia (-1.88 percent).
Global production is projected to rise 0.6 percent to 15.039 million tons in 2026 from 14.952 million tonnes in 2025, after revisions to Thailand's 2025 output and updated 2026 estimates for Thailand, Malaysia and Indonesia. Weather, including erratic rainfall and drier Southeast Asian conditions, affected output. August 2026 production was estimated at 1.396 million tonnes, down 4.51 percent from 1.462 million tonnes a year earlier. Demand is forecast to grow 0.4 percent to 15.356 million tonnes in 2026 from 15.301 million tonnes, with the largest consumption gains expected in China, Malaysia and Cambodia. Prospects depend on vehicle sales, tyre production, shipping conditions and weather-related supply disruptions, while steady EV-linked demand supported modest growth led by China and India. The ringgit traded between RM4.02 per USD and RM4.09 per USD, and the baht between 32.68 and 33.34. The SHFE January 2027 contract averaged 18,109 CNY per tonne, up 7.78 percent month-on-month, while the SGX November 2026 contract averaged USD 2.24 per kg, up 4.32 percent.
Epsilon Carbon Advances Scope 3 Emissions Measurement Across Value Chain
- By TT News
- October 01, 2026
Epsilon Carbon Pvt. Ltd., a global speciality carbon and carbon black manufacturer, has broadened its emissions accounting to include value chain impacts beyond its direct operations. The move advances measurement and management of Scope 3 emissions across its supply and distribution network, according to the company.
The initiative spans Epsilon Carbon’s integrated carbon complex in Vijayanagar, Karnataka. That site has a production capacity of 500,000 tonnes per annum of speciality carbon and 215,000 TPA of carbon black. It combines carbon manufacturing with energy circularity efforts in one integrated ecosystem. The company assessed material Scope 3 categories under GHG Protocol guidelines.
Scope 3 emissions are indirect and arise from purchased goods and services, transportation, business activities and downstream product use where relevant. The assessment gives Epsilon Carbon clearer visibility into emissions outside its direct control and a foundation for spotting reduction opportunities. It builds on existing operational emissions and energy efficiency work.
The company previously reported a 98 percent Scope 2 reduction against its baseline year. A 17 MW captive power plant uses waste heat from carbon black operations, energy consumption intensity fell 6 percent from baseline, and 77 percent of energy needs came from waste heat recovery, avoiding over 89,000 tonnes of CO₂. Epsilon Carbon now emphasises supplier engagement, data transparency and circularity, aligning disclosures with global sustainability frameworks to track value chain emissions consistently and develop measurable reduction initiatives.
Vikram Handa, Managing Director, Epsilon Carbon, said, “Meaningful climate action requires us to look beyond the boundaries of our operations and understand the impact of the entire value chain. Scope 3 measurement gives us greater visibility into the emissions and enables deeper engagement with our partners and suppliers. Building this visibility will help us make more informed decisions as we scale our operations and advance our decarbonization plans.”
Comments (0)
ADD COMMENT